Understanding the principles and application scenarios of limestone material handling is crucial for optimizing industrial processes in various sectors. This article delves into the fundamental mechanisms behind limestone handling systems and explores the specific characteristics of different operational environments where these systems are employed.
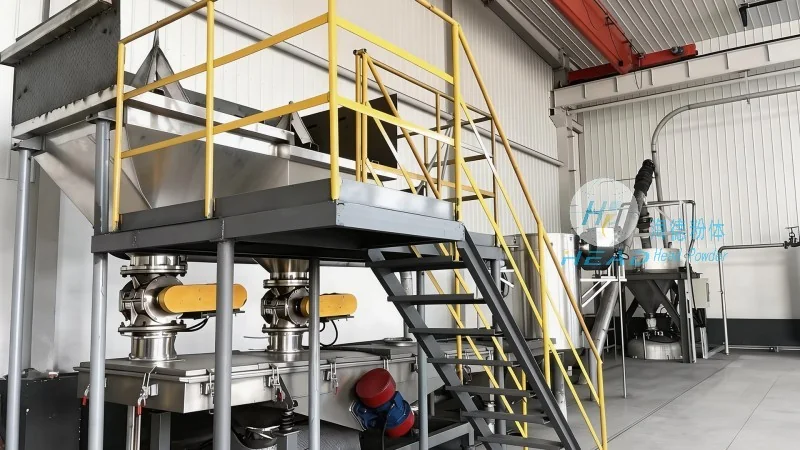
Limestone material handling systems are designed to efficiently transport limestone, a widely used raw material in industries such as cement production, construction, and chemical manufacturing. The core principles revolve around the use of specialized equipment and processes to ensure safe, reliable, and cost-effective movement of the material from its source to the point of use. Key factors influencing the design and operation of these systems include material properties, such as limestone's density, particle size distribution, and moisture content, as well as the required throughput and distance of transport. Advanced engineering solutions, including conveyor belts, bucket elevators, and pneumatic conveying systems, are employed to address these variables and meet the specific needs of each application.
The effectiveness of limestone material handling systems depends on the integration of several critical components. Conveyor belts, for instance, are commonly used for horizontal and inclined transport due to their high capacity and low maintenance requirements. Bucket elevators are ideal for vertical lifting, especially in applications where space is limited or where the material needs to be elevated to a significant height. Pneumatic conveying systems, on the other hand, utilize air pressure to transport limestone particles through pipelines, offering flexibility in layout and the ability to handle fine powders or dust. Each component is carefully selected and configured to ensure seamless operation and minimal downtime, contributing to overall system efficiency.
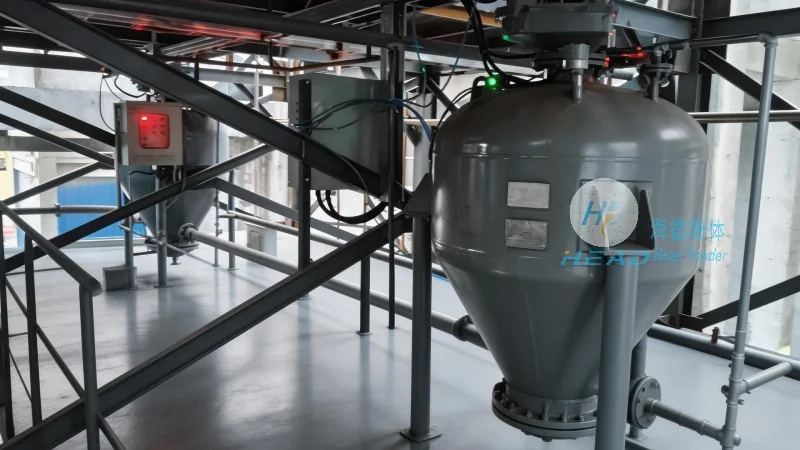
The application scenarios of limestone material handling systems vary significantly based on the industry and the specific requirements of the process. In cement plants, for example, limestone is typically transported from quarries to grinding mills or storage silos, where it is then processed into clinker. The systems used in such environments must handle large volumes of material and operate continuously to support high production rates. In construction projects, limestone may be used as a raw material for concrete production or as a decorative stone, requiring different handling methods such as bulk loading onto trucks or processing into smaller pieces for on-site use. The operational characteristics of these systems, including speed, capacity, and durability, are tailored to the demands of each scenario to ensure optimal performance.
Despite the advancements in material handling technology, several challenges remain in the efficient transport of limestone. One of the primary challenges is the prevention of material degradation, such as breakage or dust generation, which can affect the quality of the final product and increase operational costs. Advanced equipment, such as impact-resistant belts and enclosed conveying systems, is used to mitigate these issues. Another challenge is the need for maintenance and upkeep of the handling systems, which can be time-consuming and costly. Regular inspections, lubrication, and component replacement are essential to ensure the longevity and reliability of the equipment. Additionally, environmental considerations, such as dust control and noise reduction, are increasingly important in modern material handling operations, requiring the implementation of dust suppression systems and noise-canceling technologies.
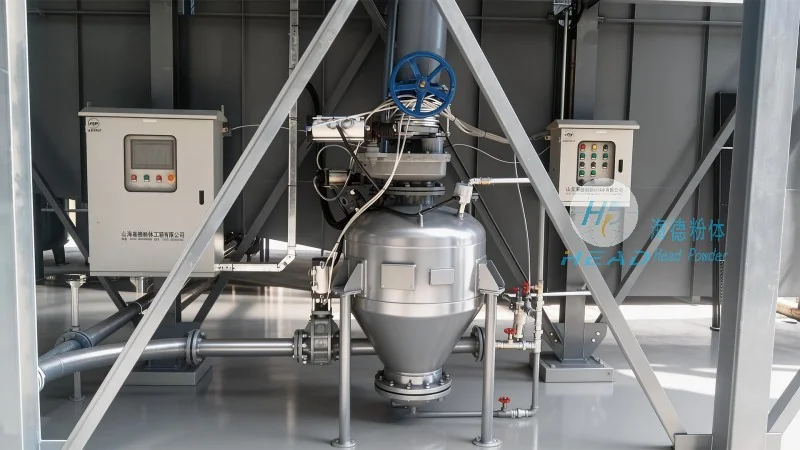
Advanced engineering solutions play a vital role in optimizing limestone material handling systems. For instance, the use of automated control systems allows for real-time monitoring and adjustment of the conveyor speed, ensuring that the system operates at peak efficiency. Sensor technology, such as load cells and level detectors, provides valuable data on material flow and system performance, enabling proactive maintenance and troubleshooting. Additionally, the integration of energy-efficient components, such as variable frequency drives (VFDs), reduces energy consumption and operating costs while maintaining the required performance levels. These technological advancements not only enhance the operational efficiency of limestone handling systems but also contribute to their sustainability and environmental compliance.
In conclusion, the principles and application scenarios of limestone material handling are complex and require careful consideration of various factors, including material properties, operational requirements, and environmental considerations. By employing advanced engineering solutions and integrating specialized equipment, industries can achieve efficient and reliable transport of limestone, supporting their production processes and meeting the demands of their customers. The continuous development of material handling technology ensures that these systems will remain essential in the industrial landscape, providing the foundation for sustainable and productive operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top