Wheat bran, a byproduct of the milling process, is essential in industries like food processing, animal feed production, and biofuel manufacturing. Efficient handling of this bulk material is critical, and the wheat bran powder conveying system from Shandong HeadPowder Engineering Co., Ltd. addresses key challenges such as dust control and energy efficiency. This article examines the fundamental principles behind these conveyors and highlights their application characteristics in various industrial settings.
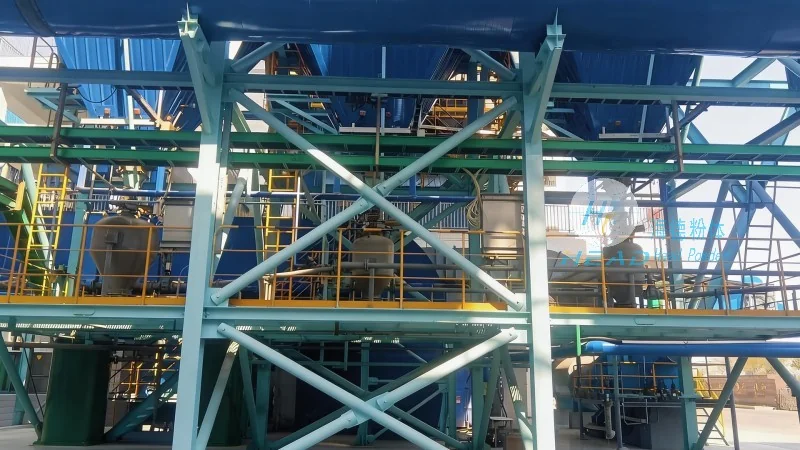
HeadPowder, a leading manufacturer in bulk material handling solutions, specializes in designing and manufacturing advanced powder conveying equipment. With a focus on innovation and customer-centric solutions, the company has established itself as a trusted partner for industries requiring reliable and efficient material transport systems. HeadPowder's headquarters is located in Shandong, China, where the company leverages local manufacturing capabilities and technical expertise to deliver high-quality products tailored to diverse industrial needs.
Wheat bran powder conveyors operate on the principle of pneumatic or mechanical transport, depending on specific design and application requirements. The primary mechanism involves using air or mechanical components to move bulk wheat bran from the source to the destination. In pneumatic systems, compressed air creates a flow that carries the powder through a pipeline, while mechanical systems may employ screw conveyors, belt conveyors, or bucket elevators. The choice of system depends on factors like wheat bran's bulk density, transport distance, and dust control needs. For fine, dust-prone wheat bran, pneumatic conveying is often preferred as it minimizes particle separation and maintains consistent flow rates.
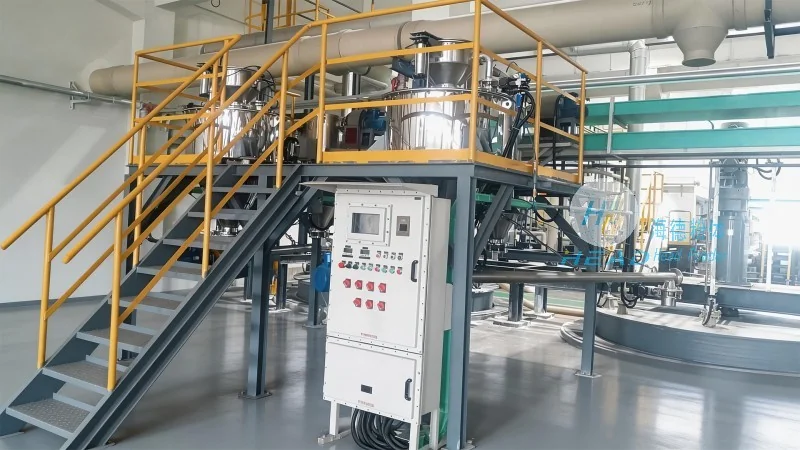
The working scene characteristics of wheat bran powder conveyors are tailored to industrial demands, including high efficiency, low maintenance, and robust construction to handle abrasive wheat bran. These systems are designed to manage varying particle sizes and moisture content, ensuring consistent performance under fluctuating conditions. Another critical characteristic is seamless integration with existing production lines, enabling uninterrupted material transfer in large-scale facilities. This integration capability is vital in food processing plants where continuous operation is essential.
Wheat bran powder conveyors are widely used across industries, each with unique operational needs. In food processing, they transport wheat bran from storage silos to processing lines, ensuring steady raw material supply for products like bread and cereals. Low dust levels are crucial here to meet hygiene standards and prevent contamination. In animal feed production, the conveyors move wheat bran to mixing and packaging units, supporting efficient feed production. Their mechanical strength and durability also make them suitable for biofuel plants, where wheat bran is processed into bioethanol. In these applications, the conveyors handle large volumes while maintaining energy efficiency to reduce operational costs.
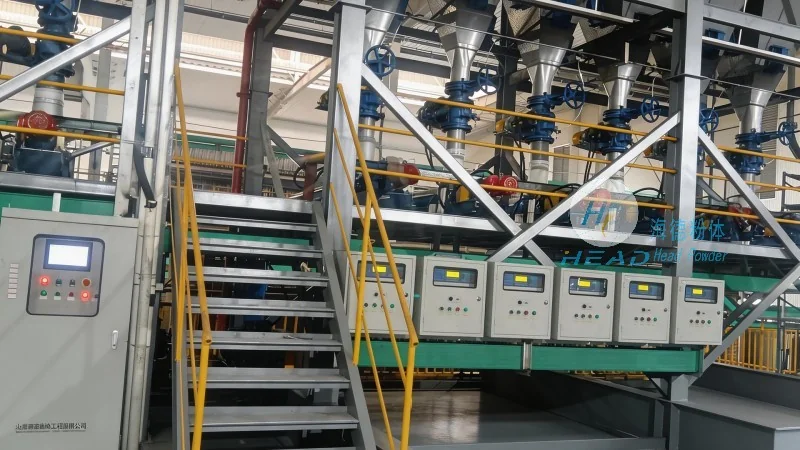
Compared to traditional methods like manual handling or bucket elevators, wheat bran powder conveyors offer significant advantages. They enhance safety by reducing manual labor in dusty environments, minimizing respiratory risks and workplace accidents. Automated operation boosts efficiency, allowing continuous production without interruptions. Performance metrics such as conveying capacity, pressure drop, and energy consumption are optimized for peak efficiency. For example, pneumatic systems achieve high rates with low pressure drops, reducing energy use. Robust construction with corrosion-resistant and wear-resistant components ensures long-term reliability and minimal downtime.
Wheat bran powder conveyors from Shandong HeadPowder Engineering Co., Ltd. represent a sophisticated solution for efficient and safe bulk wheat bran transport. By understanding the core principles and application characteristics, industries can make informed decisions about implementing the right conveying technology. The combination of advanced engineering, robust construction, and integration capabilities makes these conveyors an essential component in modern industrial processes, contributing to increased productivity and reduced operational costs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top