For coffee processing facilities, efficient material handling is crucial to maintain product quality and operational efficiency. Dry coffee pneumatic conveying lines offer a solution that minimizes product contamination and damage while ensuring smooth material transport. This article explores the fundamental principles behind these systems and highlights key working scenarios where they are commonly applied.
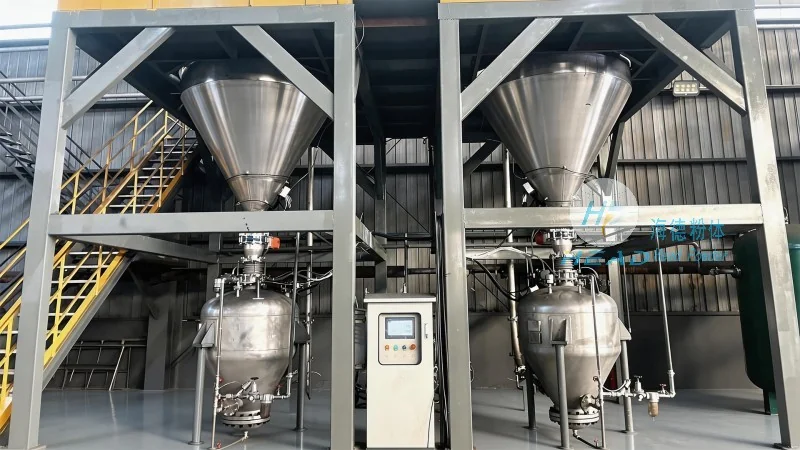
The core mechanism of dry coffee pneumatic conveying involves using air pressure to transport bulk materials like coffee beans or ground coffee. The system typically consists of a hopper, a conveyor line, and a receiver. As air is introduced into the system, it creates a flow that pulls or pushes the coffee particles through the pipeline. This method eliminates the need for mechanical components that might come into direct contact with the product, reducing the risk of contamination and preserving the coffee's aroma and quality. The air pressure can be generated through positive pressure systems, where air is forced into the line, or negative pressure systems, where air is drawn out, creating a vacuum that pulls the material. Both approaches are effective, with positive pressure often preferred for longer distances or when handling fine powders, as it provides more control over the material flow.
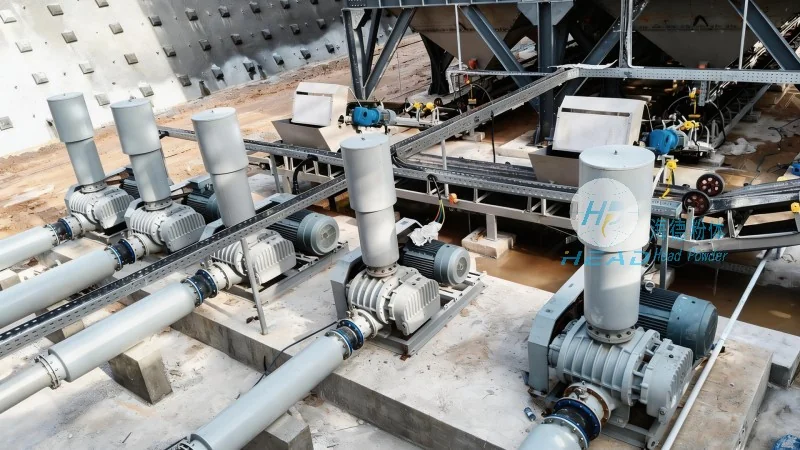
Dry coffee pneumatic conveying systems are particularly suited for applications where hygiene and product integrity are paramount. In coffee roasting plants, these lines are used to transfer freshly roasted beans from the roaster to storage silos or packaging areas. The enclosed system prevents exposure to dust, moisture, and external contaminants, which is essential for maintaining the coffee's flavor profile. Additionally, in coffee grinding operations, pneumatic conveyors efficiently move ground coffee from the grinder to blending or packaging stations, ensuring consistent product flow and reducing labor costs associated with manual handling. Another common scenario is in coffee blending facilities, where different types of coffee beans are mixed using pneumatic conveying to achieve uniform blends. The system's ability to handle various particle sizes and densities makes it versatile for different stages of coffee processing.
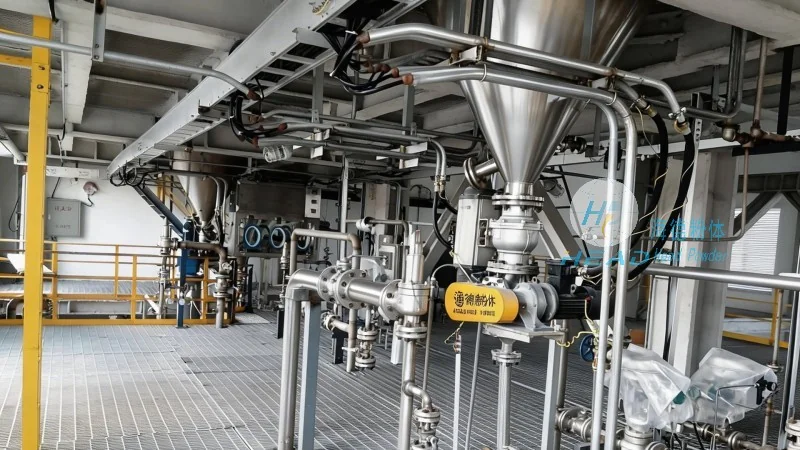
Compared to traditional mechanical conveying methods, dry coffee pneumatic conveying offers several advantages. First, it provides a completely enclosed environment, which is critical for maintaining the quality of sensitive products like coffee. The lack of direct contact between the product and machinery reduces the risk of cross-contamination and preserves the coffee's natural characteristics. Second, the system is highly flexible and can be easily reconfigured to accommodate changes in production volume or product types. This adaptability is valuable for coffee manufacturers who may need to adjust their processing lines based on market demands. Third, pneumatic conveying systems are energy-efficient, especially when using low-pressure air, and can reduce operational costs over time. The absence of moving parts that require regular maintenance also contributes to lower long-term maintenance expenses.
As a leading provider of engineering solutions for the food processing industry, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems. With a focus on quality and innovation, HeadPowder has established itself as a trusted partner for coffee manufacturers seeking reliable and efficient material handling solutions. The company's expertise in pneumatic technology ensures that each system is tailored to meet the specific needs of its clients, whether it's for small-scale roasting operations or large industrial coffee processing plants. HeadPowder's commitment to using high-quality materials and advanced engineering principles ensures that their systems not only meet but exceed industry standards for performance and durability.
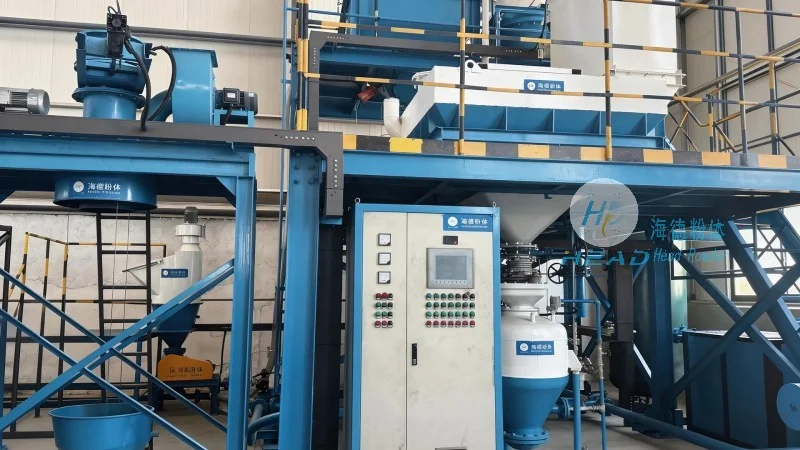
Dry coffee pneumatic conveying systems represent a sophisticated and effective solution for modern coffee processing. By leveraging the principles of air pressure to transport materials, these systems offer superior hygiene, product protection, and operational flexibility. For coffee manufacturers looking to enhance their processing capabilities and maintain the highest standards of quality, investing in a well-designed pneumatic conveying system is a strategic decision. With the support of companies like Shandong HeadPowder Engineering Co., Ltd., coffee producers can achieve efficient, reliable, and cost-effective material handling that supports their business growth and product excellence.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top