High-pressure dilute-phase pneumatic conveying systems represent a sophisticated technology in material handling, offering efficient and reliable solutions for transporting bulk materials over varying distances. This article delves into the fundamental principles behind these systems and explores the key characteristics of their operational environments, providing a comprehensive overview for professionals in the field.
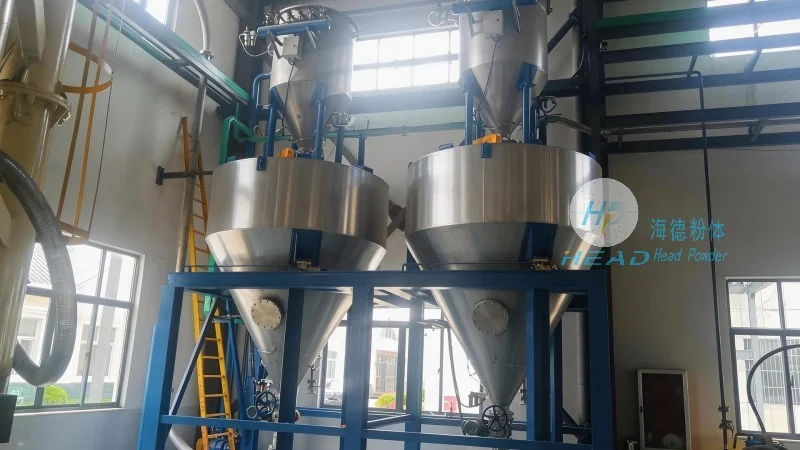
At the heart of high-pressure dilute-phase pneumatic conveying lies the principle of transporting particles in a low concentration within a gas stream. Unlike dense-phase systems, where particles are more concentrated and move in a plug flow, dilute-phase systems rely on a higher velocity of the conveying medium (typically air or other gases) to suspend and move the material. The system operates under elevated pressure, often ranging from 5 to 15 bar, which enables the gas to maintain a sufficient velocity to keep particles suspended and prevent settling. This method is particularly effective for fine to medium-sized particles, as the high velocity ensures that the particles remain in a suspended state throughout the conveying process.
A critical component in the system is the air compressor, which generates the necessary pressure and flow rate. The compressor supplies compressed air to the conveying line, where it mixes with the material to be transported. The line itself is typically made of robust materials such as stainless steel or high-grade plastic, designed to withstand the high-pressure conditions and prevent leakage. The system also includes various accessories like valves, filters, and cyclones, which are essential for controlling the flow, separating the material from the air, and ensuring the system operates efficiently.
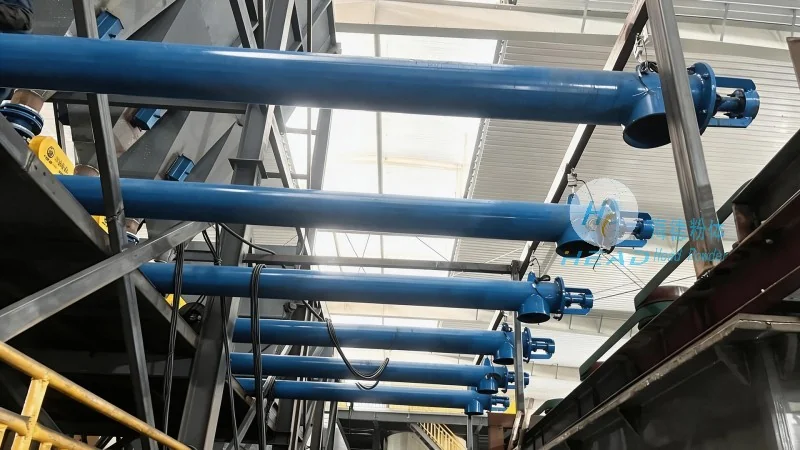
The operational characteristics of high-pressure dilute-phase systems are tailored to specific industrial applications, making them suitable for a wide range of scenarios. One of the primary advantages is their ability to handle materials with varying particle sizes and densities, from fine powders to small granules. This versatility makes them ideal for industries such as pharmaceuticals, food processing, and chemical manufacturing, where the purity and integrity of the material must be maintained.
Another significant characteristic is the system's capability to transport materials over long distances, often up to several hundred meters, without the need for intermediate storage or transfer points. This continuous operation reduces downtime and improves overall productivity. The high-pressure design also minimizes the risk of material degradation, as the particles are kept in motion and do not experience prolonged exposure to static conditions, which can lead to agglomeration or quality issues.
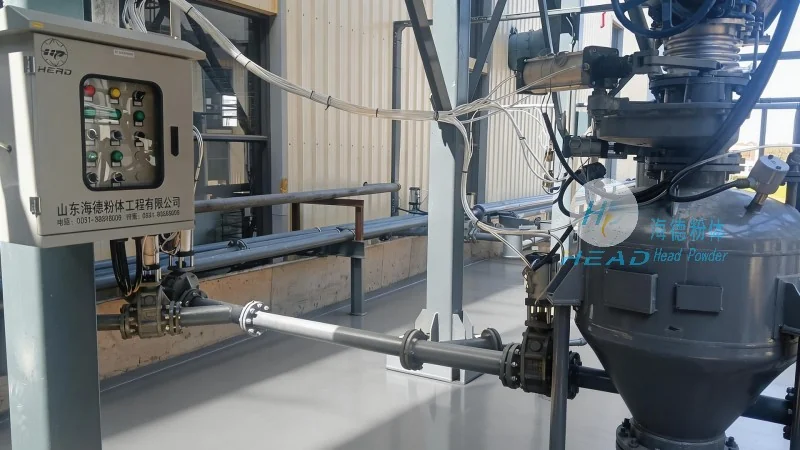
Furthermore, the dilute-phase approach offers advantages in terms of energy efficiency and maintenance. By maintaining a higher gas velocity, the system can achieve a more uniform flow, reducing the likelihood of blockages or clogs. This reduces the need for frequent maintenance and cleaning, contributing to lower operational costs over time. The system's design also allows for easy integration with existing production lines, as it can be customized to fit specific space constraints and operational requirements.
High-pressure dilute-phase pneumatic conveying systems are widely used across various industries due to their adaptability and efficiency. In the pharmaceutical industry, for example, these systems are crucial for transporting active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring that they remain free from contamination and maintain their quality. The system's ability to handle fine powders without causing particle degradation makes it an ideal choice for this sector.
In the food processing industry, the technology is used to transport ingredients like flour, sugar, and spices, where hygiene and product purity are paramount. The stainless steel construction of the conveying lines and components ensures that the system meets stringent food safety standards, while the low concentration of particles prevents cross-contamination between different products.
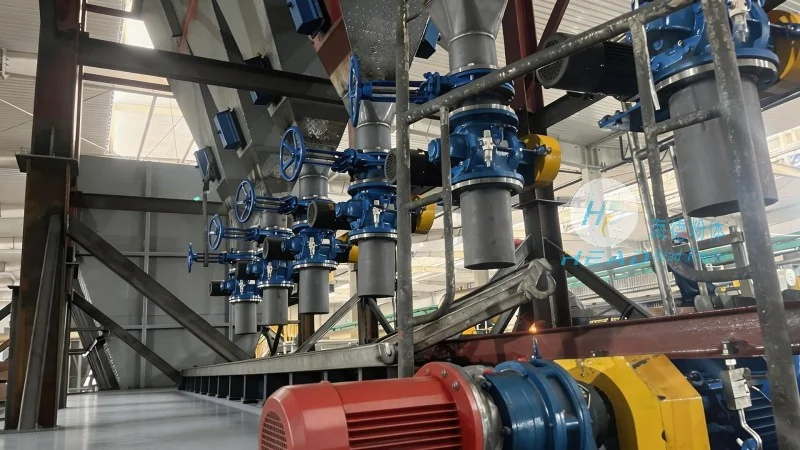
The chemical industry also benefits significantly from high-pressure dilute-phase systems, particularly when handling powders that are reactive or require precise control over temperature and pressure. The system's ability to maintain a consistent flow and pressure helps in controlling the reaction conditions, ensuring safe and efficient processing. Additionally, the system's design allows for easy cleaning and maintenance, which is essential for handling chemicals that may be corrosive or hazardous.
High-pressure dilute-phase pneumatic conveying systems offer a robust and efficient solution for material handling in various industrial applications. Their ability to transport materials over long distances, maintain product quality, and operate with minimal maintenance makes them a preferred choice for many industries. As technology continues to advance, these systems are likely to become even more sophisticated, with improved energy efficiency and better integration with automation technologies. The continued development and application of high-pressure dilute-phase systems will undoubtedly play a vital role in enhancing productivity and sustainability in material handling operations worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top