Electrode carbon purification residue, also known as calcium carbide ash, is a byproduct generated during the production process of calcium carbide. This residue contains a significant amount of calcium oxide and other impurities, which can cause environmental pollution if not handled properly. Air-driven conveying technology has emerged as an efficient method for the transport of this residue, offering advantages such as low energy consumption, minimal equipment wear, and the ability to handle fine powders. This article will explore the principle of air-driven conveying for electrode carbon purification residue and analyze its working scene characteristics.
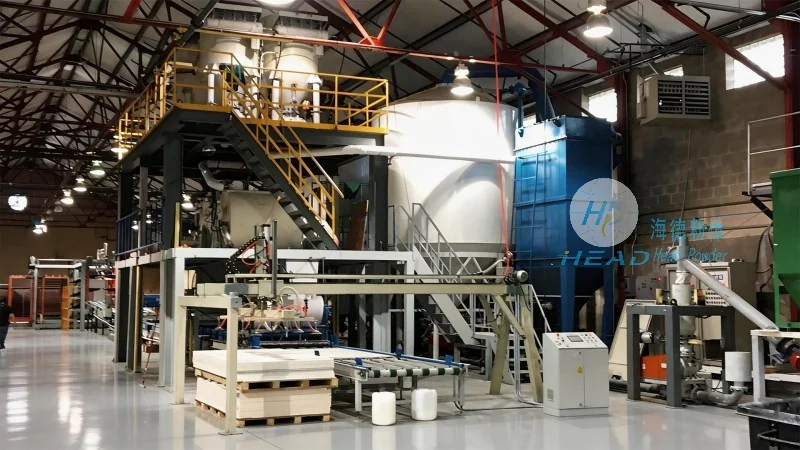
Air-driven conveying, also referred to as pneumatic conveying, utilizes compressed air to transport bulk materials through a pipeline system. In the context of electrode carbon purification residue, the process typically involves a series of components, including a hopper, a feeder, a conveying line, and a receiver. The residue is first stored in a hopper, then fed into the conveying line via a feeder. Compressed air is introduced into the conveying line, creating a flow that carries the residue particles forward. The air velocity is carefully controlled to ensure that the particles are suspended and transported without clogging the pipeline. The key principle is the balance between the air velocity and the particle size and density, which determines the conveying capacity and efficiency. The system can be either positive pressure (where air is blown into the line) or negative pressure (where air is sucked out), with positive pressure being more common for transporting electrode carbon purification residue due to its dusty nature and the need to prevent dust leakage.
Several critical components are integral to the air-driven conveying system for electrode carbon purification residue. The hopper serves as the storage unit, holding the residue until it is needed for transport. The feeder, often a rotary valve or a screw feeder, controls the flow rate of the residue into the conveying line, ensuring a consistent and controlled feed. The conveying line is typically made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of the residue. The air compressor provides the necessary compressed air, which is regulated by a pressure control system to maintain optimal operating conditions. The receiver is the final destination where the residue is deposited, and it may include a dust collection system to capture any fine particles that escape during the conveying process. Each component plays a vital role in ensuring the smooth and efficient operation of the entire system.
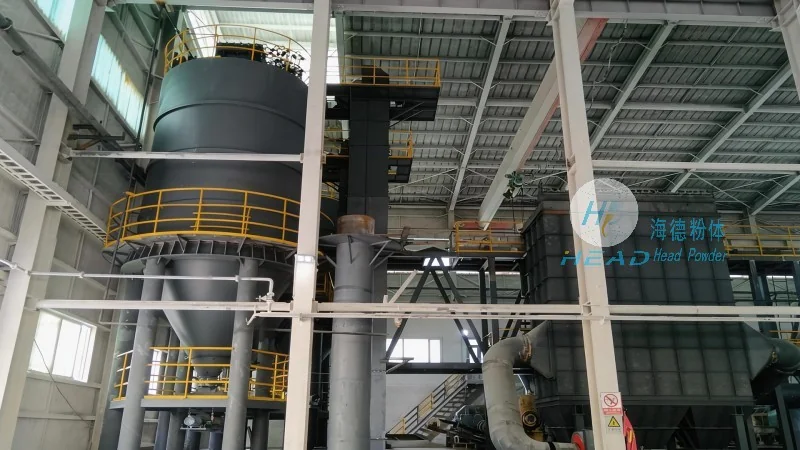
The application of air-driven conveying for electrode carbon purification residue is prevalent in industrial settings, particularly in the calcium carbide and electrode manufacturing industries. The working scene characteristics are influenced by several factors, including the scale of production, the distance of transport, and the environmental regulations. For small-scale operations, a simple positive pressure system with a short conveying line may be sufficient. However, for large-scale plants, a more complex system with multiple conveying lines and a central control system is often required to handle high volumes of residue. The system is also suitable for long-distance transport, as the air velocity can be adjusted to maintain the particle suspension over extended distances. Additionally, the technology is adaptable to different environments, including indoor and outdoor settings, as long as proper ventilation and dust control measures are in place. The working scene often involves integration with other processes, such as the residue's subsequent treatment or disposal, making the air-driven conveying system a critical link in the overall production workflow.
Implementing air-driven conveying for electrode carbon purification residue offers several advantages that make it a preferred choice over traditional methods like belt conveyors or bucket elevators. One of the primary benefits is energy efficiency, as the system requires less power to transport the residue compared to mechanical systems. The low equipment wear is another significant advantage, as the absence of moving parts in contact with the material reduces maintenance costs and extends the lifespan of the equipment. Additionally, the system can handle fine and dusty materials without causing clogging or blockages, which is essential for electrode carbon purification residue due to its particle size. However, there are also considerations to keep in mind. The system's performance is highly dependent on the air pressure and flow rate, which must be precisely controlled to avoid system failures or material loss. Dust control is also a critical aspect, as the fine particles can be hazardous to workers and the environment. Proper filtration and ventilation systems are necessary to mitigate these risks. Furthermore, the initial investment cost for the air-driven conveying system can be higher than traditional methods, although the long-term savings in energy and maintenance offset this cost over time.
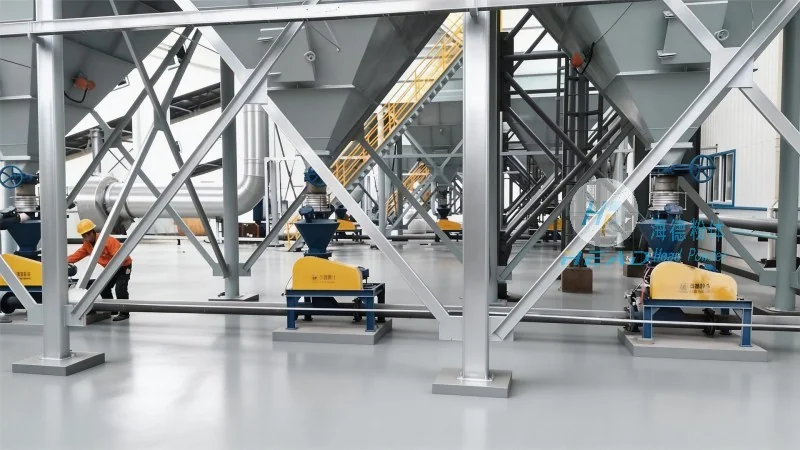
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions in the powder handling industry, has successfully implemented air-driven conveying systems for electrode carbon purification residue in several industrial plants. The company's expertise lies in designing customized systems that meet the specific requirements of each client, ensuring optimal performance and efficiency. For instance, in a large-scale calcium carbide production facility, HeadPowder designed a positive pressure air-driven conveying system that transported the residue from the reaction chamber to the storage silo over a distance of 200 meters. The system was equipped with a high-efficiency air compressor and a dust collection system, which effectively controlled the dust emissions and ensured compliance with environmental regulations. The client reported a significant reduction in energy consumption and maintenance costs compared to their previous belt conveyor system. This case study highlights the effectiveness of air-driven conveying technology in handling electrode carbon purification residue and the role of specialized engineering companies like HeadPowder in optimizing these systems for industrial applications.
Air-driven conveying technology has proven to be an effective and efficient method for the transport of electrode carbon purification residue, offering numerous advantages over traditional mechanical systems. The principle of using compressed air to suspend and transport particles is well-established, and the working scene characteristics of this technology make it suitable for various industrial applications. As environmental regulations become more stringent and the demand for efficient waste management increases, the adoption of air-driven conveying systems is likely to grow. Companies like Shandong HeadPowder Engineering Co., Ltd. are at the forefront of developing and implementing these systems, providing customized solutions that address the specific needs of their clients. The future of electrode carbon purification residue handling will likely involve further advancements in air-driven conveying technology, such as the integration of automation and real-time monitoring systems, to enhance performance and reduce operational costs. By leveraging the principles and characteristics of air-driven conveying, industries can effectively manage their residue while minimizing environmental impact and maximizing operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top