HeadPowder, a leading provider in the field of material handling solutions, specializes in the application of pneumatic conveying systems for desulfurization sodium bicarbonate material. This article explores the working principle and key characteristics of such systems, offering insights into their efficiency and operational advantages.
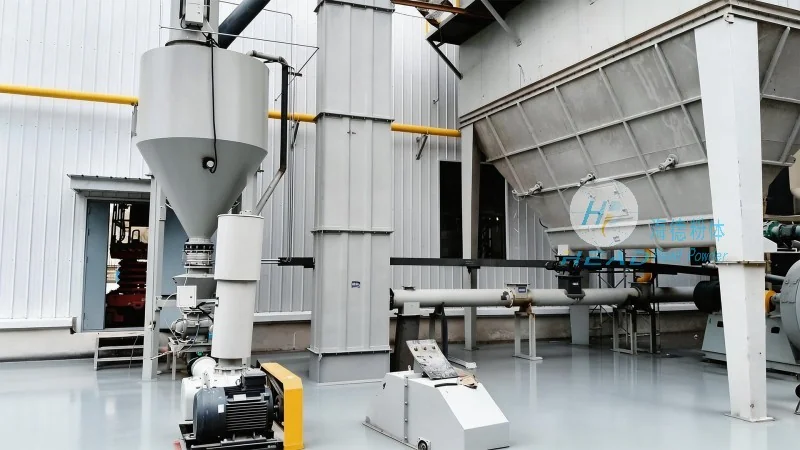
Pneumatic conveying is a method of transporting bulk materials through a pipeline using a gas stream, typically air. In the context of desulfurization sodium bicarbonate, this technology is crucial for handling the material from storage to processing units without the need for mechanical equipment like conveyors or elevators. The process involves several key components and steps that ensure efficient material transport.
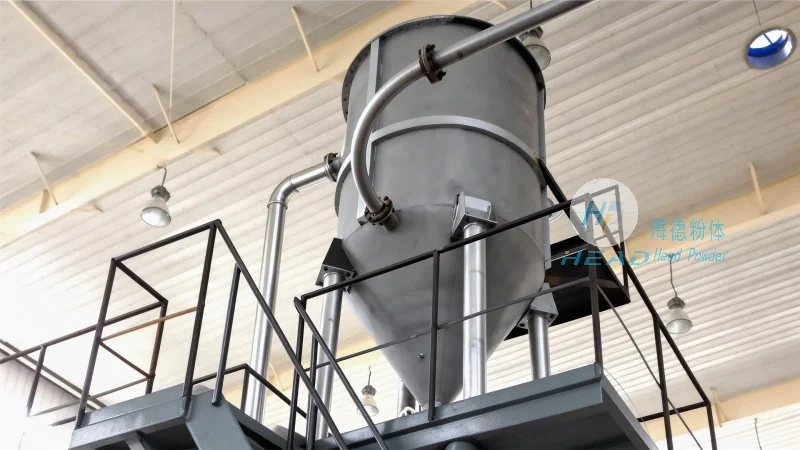
The core of the pneumatic conveying system for desulfurization sodium bicarbonate material lies in the creation of a high-velocity air stream within a sealed pipeline. The material, in the form of dry powder or granules, is introduced into the pipeline at a specific point, often through a hopper or feeder. As the air flows at a velocity exceeding the material's terminal velocity, it entrains the particles, carrying them along the pipeline to the destination point. The system typically includes a blower or compressor to generate the necessary air pressure and flow rate, ensuring consistent material transport. The process can be either positive pressure (where air is pushed through the system) or negative pressure (where air is drawn out), depending on the application requirements and the distance of material transport.
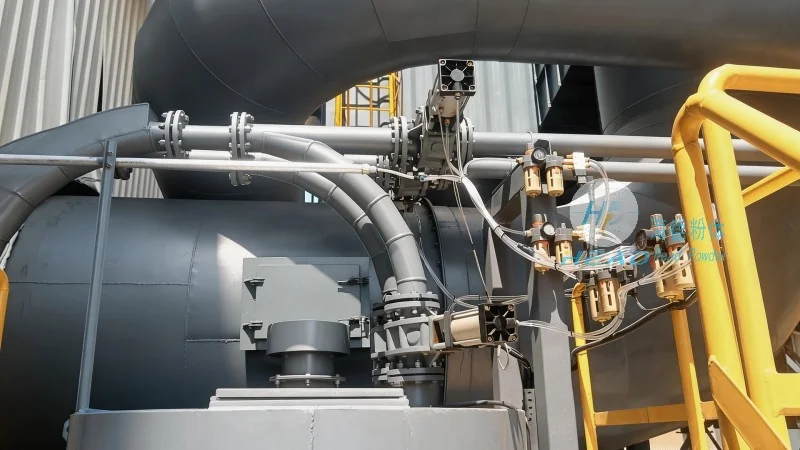
Several distinct characteristics define the effectiveness of pneumatic conveying systems for desulfurization sodium bicarbonate material. First, the system offers a completely enclosed transport path, which minimizes dust emissions and contamination, a critical factor in industrial environments where air quality and material purity are paramount. Second, it provides a flexible and scalable solution, allowing for changes in material flow rates and pipeline configurations without significant modifications to the system. Third, the technology is highly efficient in terms of energy consumption compared to traditional mechanical conveying methods, reducing operational costs over time. Additionally, the system can handle a wide range of material properties, including varying particle sizes and moisture content, making it versatile for different stages of the desulfurization process. The ability to transport material vertically and horizontally with minimal loss or degradation is another notable advantage, ensuring that the quality of desulfurization sodium bicarbonate is maintained throughout the conveying process.
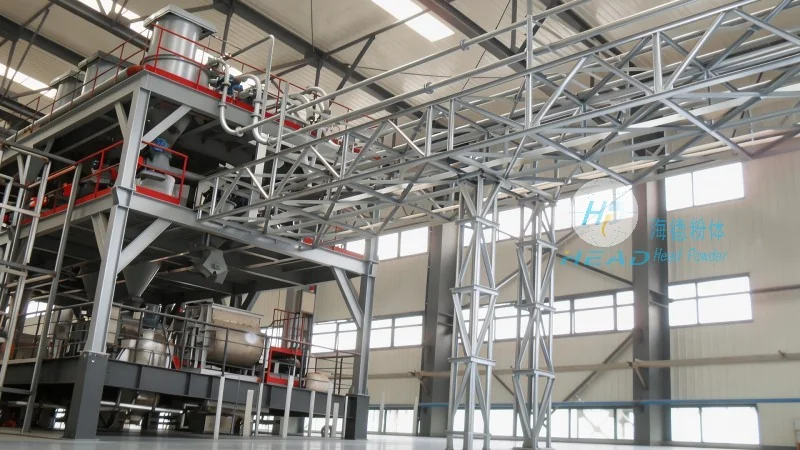
While pneumatic conveying systems offer numerous benefits, proper operation and maintenance are essential to ensure optimal performance and longevity. Regular inspection of the blower or compressor, pipeline integrity, and material feed mechanisms is crucial to prevent blockages or system failures. The use of appropriate filters and cleaning systems is also vital to maintain air quality and prevent dust accumulation within the pipeline. HeadPowder, with its headquarters in Shandong, China, provides comprehensive support for the installation, operation, and maintenance of pneumatic conveying systems, ensuring that clients achieve the best possible results in their desulfurization processes. By adhering to best practices and leveraging the expertise of HeadPowder, industrial facilities can maximize the efficiency and reliability of their material handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top