When it comes to the efficient handling and transportation of rice husk ash materials, pneumatic conveying systems offer a reliable and effective solution. These systems are designed to move bulk materials like rice husk ash through a pipeline using air pressure, providing a clean and efficient method for material transport in industrial applications.
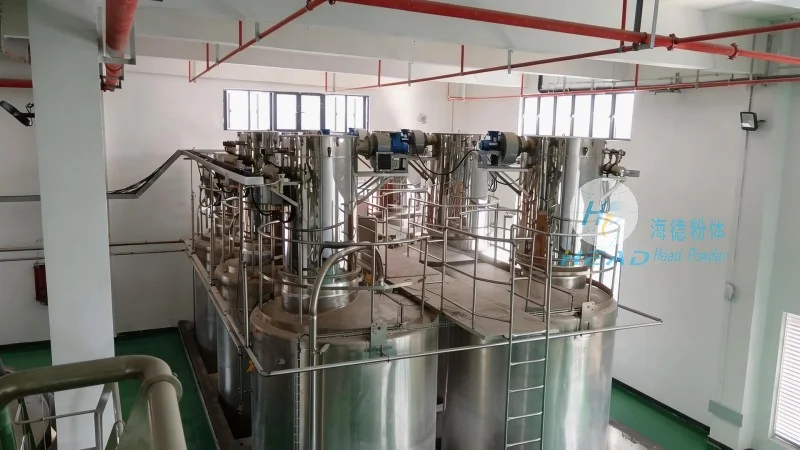
The core mechanism of pneumatic conveying for rice husk ash involves the use of a conveying pipeline where air is introduced to create a flow that transports the material. There are primarily two types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems use higher air velocities to move materials in a suspended state, while dense-phase systems operate at lower velocities, allowing for a more controlled and gentle transport of the material. For rice husk ash, the choice of system depends on factors such as the material's properties, the required conveying distance, and the desired flow rate. The system typically includes components like a feeder, a blower or compressor, a pipeline, and a receiver. The feeder ensures a consistent feed of the rice husk ash into the system, while the blower or compressor generates the necessary air pressure to move the material through the pipeline. The pipeline is designed to handle the material's characteristics, preventing blockages or degradation. The receiver collects the material at the end of the conveying line, completing the process.
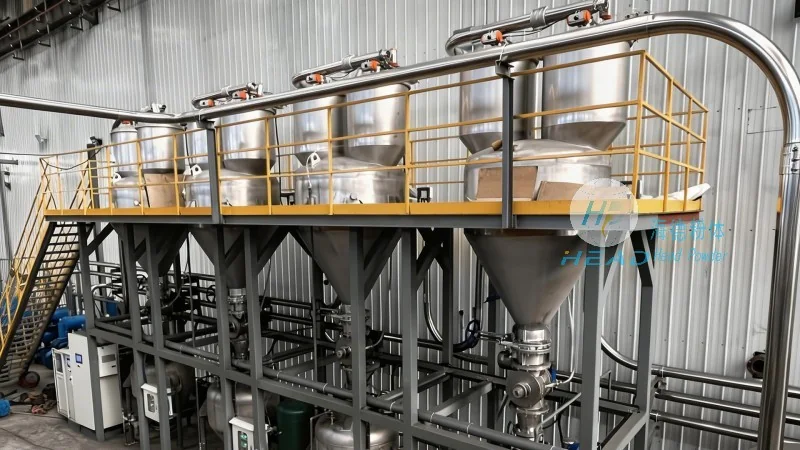
Pneumatic conveying systems for rice husk ash exhibit several notable characteristics that make them suitable for industrial applications. One of the primary advantages is the ability to transport materials in a closed system, which helps maintain cleanliness and prevents dust emissions. This is particularly important for rice husk ash, as it can be a fine or powdery material that may cause respiratory issues or environmental concerns if not handled properly. Additionally, pneumatic conveying allows for the integration of the system with other processing equipment, enabling a seamless flow of materials from one stage to another. The systems are also relatively compact and can be installed in various industrial settings, making them adaptable to different production environments. Another key characteristic is the energy efficiency of the system, especially when compared to traditional methods like bucket elevators or belt conveyors. By using air pressure to move the material, the system can reduce energy consumption and operational costs. Furthermore, the flexibility of pneumatic conveying allows for the adjustment of flow rates and conveying distances, providing versatility in material handling. The systems can handle a wide range of material sizes and densities, making them suitable for diverse applications involving rice husk ash.
In industrial processing, the use of pneumatic conveying for rice husk ash materials offers significant benefits. These systems are commonly used in the production of rice husk ash-based products, such as activated carbon or biofuels, where the material needs to be transported from storage to processing equipment. The efficiency of the system ensures that the material is delivered in a consistent and controlled manner, which is crucial for maintaining product quality. The closed system also helps in maintaining a clean working environment, reducing the risk of contamination and improving safety for workers. Moreover, the ability to handle fine or powdery materials without causing degradation makes pneumatic conveying ideal for applications where the material's integrity is essential. The systems can be integrated with other processing steps, such as grinding or mixing, to streamline the production process and enhance overall efficiency. The reliability of pneumatic conveying systems also contributes to reduced downtime and maintenance costs, as they are designed to operate continuously with minimal interruptions.
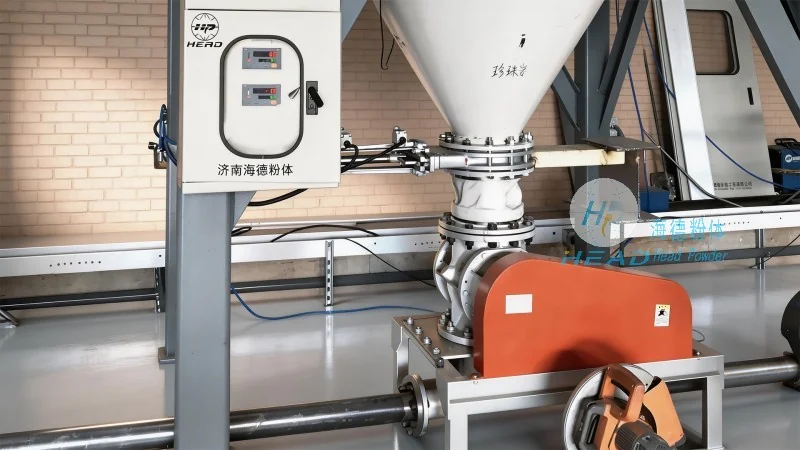
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of pneumatic conveying solutions for various industrial materials, including rice husk ash. With a focus on innovation and quality, the company specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of its clients. HeadPowder's expertise lies in understanding the unique properties of materials like rice husk ash and developing systems that ensure efficient, clean, and reliable transport. The company's facilities are located in Shandong, China, where it leverages advanced technology and skilled engineering to deliver high-performance pneumatic conveying solutions. By combining years of experience in the industry with a commitment to customer satisfaction, HeadPowder has established itself as a trusted partner for businesses seeking effective material handling solutions. The company's products are designed to meet international standards and are backed by comprehensive technical support and after-sales service, ensuring that clients receive the best possible solution for their material transport needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top