HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and supply of advanced pneumatic conveying systems tailored for fertilizer handling. This article explores the fundamental working principles and key characteristics of pneumatic conveying technology, which is widely used in the fertilizer industry to efficiently transport bulk materials.
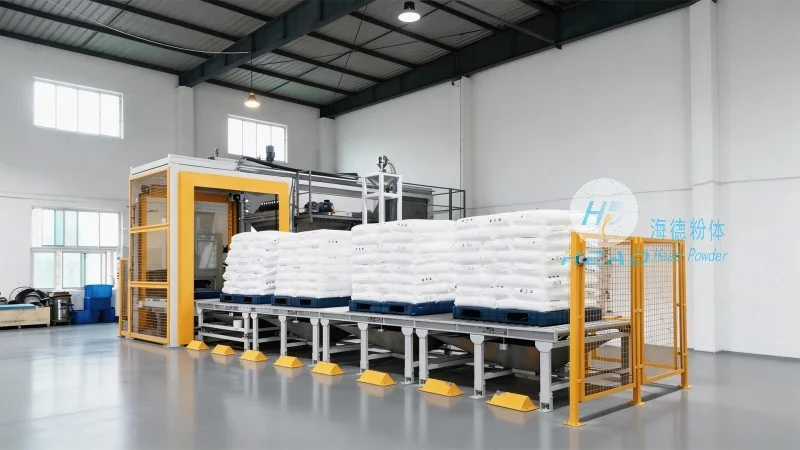
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using a stream of air. The process typically involves two main types: aspiration (or suction) systems and compression (or pressure) systems. Both systems rely on the same core principle: creating a pressure differential to move material through the pipeline.
In an aspiration system, a vacuum is created at the material inlet, drawing the fertilizer into the pipeline. The material is then carried by the air stream to the discharge point. This method is ideal for short to medium distances and for handling materials that are light and free-flowing. The system includes a vacuum pump, a material hopper, a filter, and a discharge valve.
On the other hand, a compression system uses a positive pressure from a blower or fan to push the fertilizer through the pipeline. This approach is suitable for longer distances and for materials that are dense or have higher moisture content. The system comprises a positive displacement blower, a material hopper, a pressure vessel, and a discharge valve.
Regardless of the system type, the basic components of a pneumatic conveying system for fertilizers include: a air mover (vacuum or pressure), a material feed device (hopper or feeder), a conveying pipeline, a separator (to separate air from material), and a discharge device. The air mover generates the necessary airflow to create the pressure differential, while the material feed device ensures a consistent flow of fertilizer into the pipeline. The pipeline transports the material and air mixture to the destination, where the separator separates the air and returns it to the system, and the material is discharged into a storage or processing unit.
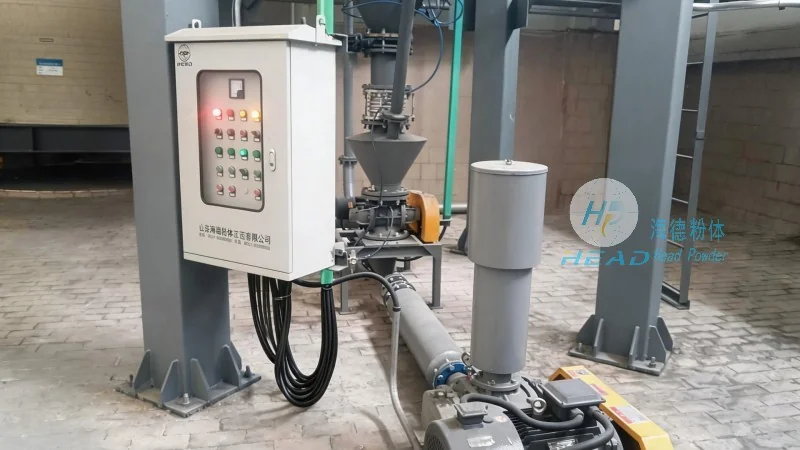
The application of pneumatic conveying in the fertilizer industry offers several distinct advantages that make it a preferred choice over traditional methods like belt conveyors or bucket elevators.
Efficiency and Speed is a primary characteristic. Pneumatic systems can transport large volumes of fertilizer quickly over considerable distances, often at rates of several tons per hour. This high throughput is crucial for meeting the demands of modern fertilizer production and distribution. The ability to handle bulk materials in a continuous flow reduces downtime and increases overall operational efficiency.
Space Efficiency is another notable feature. Unlike traditional conveyors that require extensive horizontal or vertical space, pneumatic systems can be installed in confined areas or even vertically, making them ideal for facilities with limited floor space. The compact design of the system, including the pipeline and air mover, allows for flexible layout options without compromising performance.
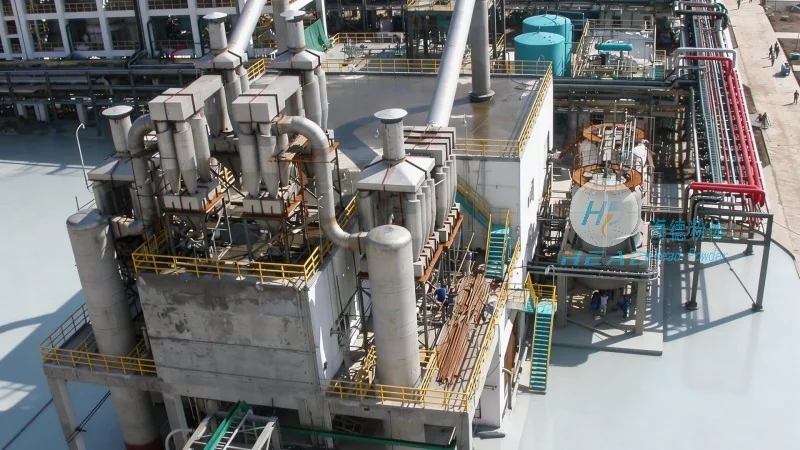
Safety and Environmental Benefits are significant advantages. Pneumatic conveying eliminates the need for manual handling of bulk materials, reducing the risk of dust exposure and potential health hazards. The enclosed pipeline system prevents dust from escaping into the environment, contributing to a cleaner and safer workplace. Additionally, the system can be equipped with dust collection and filtration systems to further minimize environmental impact.
Flexibility and Versatility are also key characteristics. Pneumatic conveying systems can be designed to handle a wide range of fertilizer types, including granular, powdered, or even wet materials. The system can be easily adapted to different production processes, such as blending, storage, or packaging, by adjusting the pipeline layout or adding additional components like mixers or classifiers. This flexibility allows manufacturers to scale their operations and respond to changing market demands.
Low Maintenance Requirements are an important consideration for long-term operational costs. Compared to mechanical conveyors, pneumatic systems have fewer moving parts, reducing the likelihood of wear and tear and the need for frequent maintenance. The air mover and pipeline components are designed for durability, and regular cleaning and inspection can ensure reliable performance over extended periods.
Pneumatic conveying is a highly effective and versatile method for transporting fertilizer materials, offering significant advantages in efficiency, safety, and flexibility. As a leading provider in the industry, Shandong HeadPowder Engineering Co., Ltd. specializes in developing customized pneumatic conveying solutions that meet the specific needs of fertilizer manufacturers. By leveraging advanced technology and engineering expertise, HeadPowder ensures that their systems deliver optimal performance and contribute to the overall productivity and sustainability of fertilizer operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top