HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder handling equipment. Among their product lineup is the vacuum suction type powder pneumatic conveying machine, which is widely used in various industrial sectors for efficient material transport. This article will delve into the working principle and key features of this equipment, providing a comprehensive understanding for potential users.
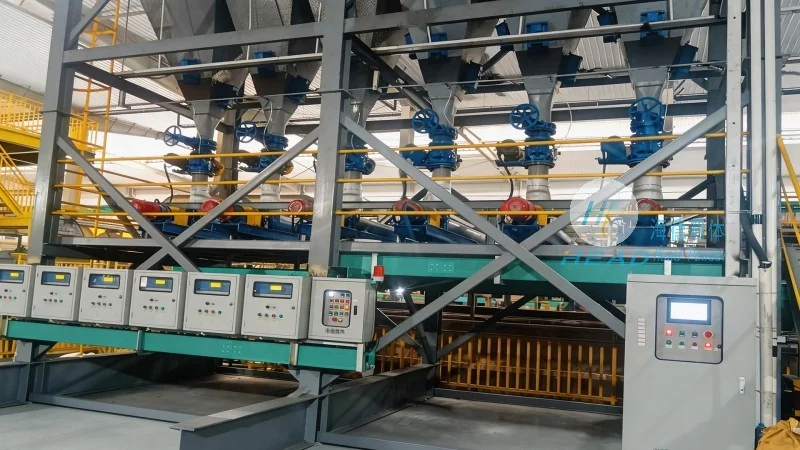
The vacuum suction type powder pneumatic conveying system operates on the principle of creating a negative pressure environment in the conveying pipeline. This is achieved by using a vacuum pump or a fan to draw air and the powder material from the source container into the pipeline. The process begins with the powder being fed into the suction hopper or the material container. As the vacuum pump starts, it reduces the pressure inside the pipeline, causing the air and powder mixture to be drawn into the system. The mixture then travels through the pipeline to the discharge point, where the powder is separated from the air using a separator or a cyclone. The separated air is then either recirculated or released, while the powder is collected in the receiving container.
Key components of this system include the vacuum pump, suction hopper, conveying pipeline, and a separator. The vacuum pump is responsible for maintaining the negative pressure, ensuring a continuous flow of the powder-air mixture. The suction hopper is designed to hold the bulk material and facilitate the initial feeding process. The conveying pipeline is typically made of stainless steel or other corrosion-resistant materials to handle different types of powders. The separator, often a cyclone or a bag filter, separates the powder from the air, ensuring that the powder is delivered to the destination without contamination.
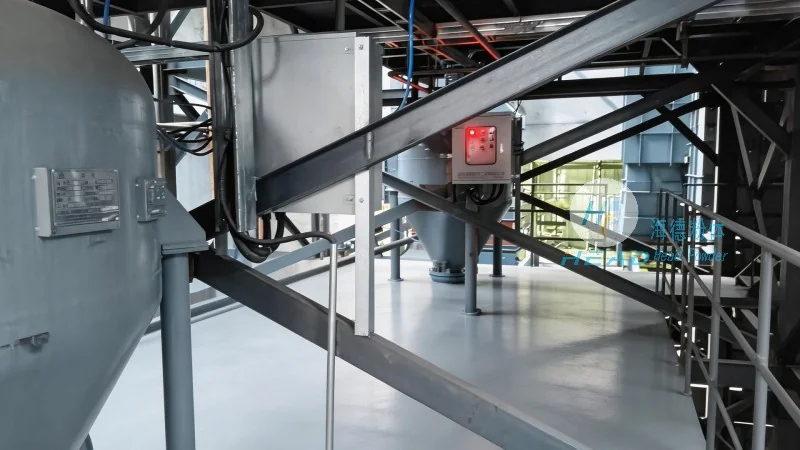
One of the primary advantages of the vacuum suction type system is its ability to transport powders over long distances with minimal pressure drop. This makes it suitable for applications where the material needs to be moved from a central storage area to multiple processing points. The system is also highly flexible, as it can handle a wide range of powder types, including fine powders, granules, and even bulk materials with varying moisture content. The negative pressure operation ensures that dust and particles are contained within the system, reducing the risk of environmental contamination and improving workplace safety.
Another notable feature is the low energy consumption compared to positive pressure systems. The vacuum pump operates at lower pressures, which results in reduced energy costs and longer equipment lifespan. Additionally, the system is easy to install and maintain, with modular components that can be replaced or upgraded as needed. The compact design of the equipment allows for space-saving installations in industrial facilities, making it ideal for both new and existing production lines.
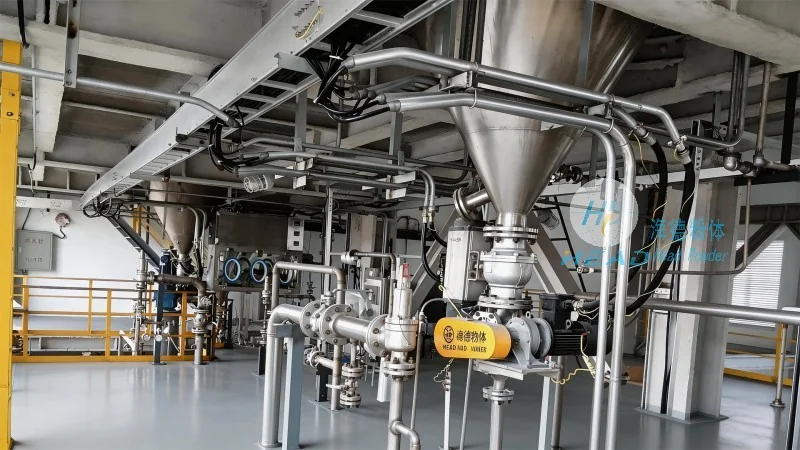
The vacuum suction type powder pneumatic conveying equipment is widely used in industries such as food processing, pharmaceuticals, chemicals, and minerals. In the food industry, it is used to transport ingredients like flour, sugar, and spices, ensuring hygienic and dust-free handling. In the pharmaceutical sector, the system is crucial for transporting active pharmaceutical ingredients (APIs) and other sensitive materials, maintaining strict contamination control. The chemical industry utilizes this equipment for handling powders like pigments, catalysts, and reagents, where precise dosing and minimal material loss are essential.
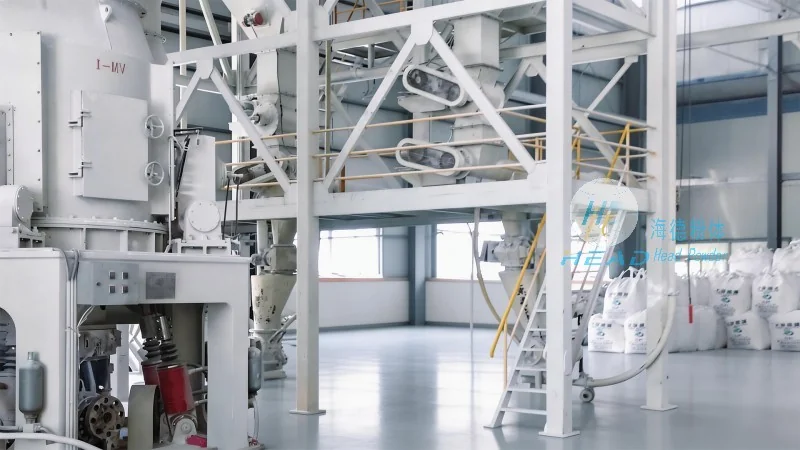
One of the significant advantages of this technology is its ability to handle materials that are difficult to transport using traditional methods, such as powders with high moisture content or those that are prone to caking. The vacuum suction system prevents material buildup in the pipeline, reducing the risk of blockages and ensuring consistent flow rates. Furthermore, the system is scalable, allowing manufacturers to adjust the conveying capacity based on their production needs, from small-scale operations to large industrial plants.
HeadPowder's vacuum suction type powder pneumatic conveying equipment offers a reliable and efficient solution for powder handling in various industrial applications. By understanding the working principle and key features of this technology, businesses can make informed decisions about integrating it into their operations. The combination of low energy consumption, flexible design, and effective material transport makes it a preferred choice for industries seeking to improve productivity and maintain high standards of safety and hygiene.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top