For industrial applications involving the transport of cement mineral powders, specialized equipment is essential to ensure efficient and reliable material handling. This article provides an overview of the working principles and key features of cement mineral powder material handling equipment, highlighting the technological advancements and operational benefits offered by such systems.
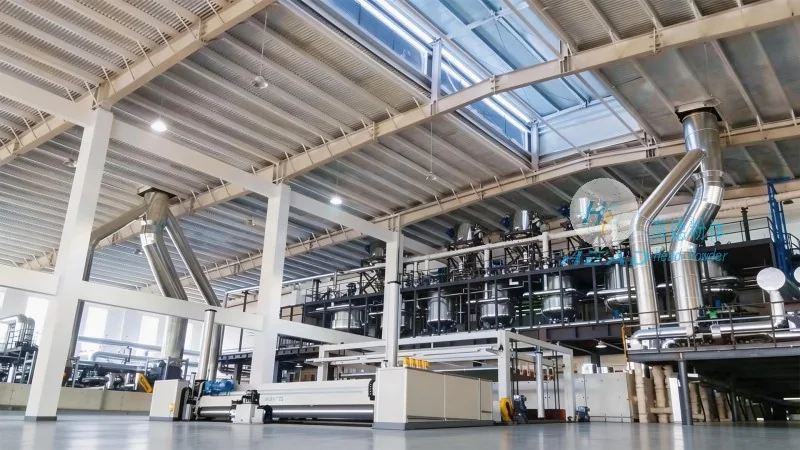
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced material handling solutions. With a strong commitment to quality and innovation, the company has established itself as a trusted provider of equipment tailored to the cement and mineral processing industries. The company’s facilities and expertise are dedicated to delivering robust and efficient systems that meet the demanding requirements of modern industrial operations.
The core working principle of cement mineral powder material handling equipment revolves around the efficient transfer of fine powders from one location to another. These systems typically utilize a combination of mechanical components, including conveyor belts, screw conveyors, pneumatic transport systems, or a combination of both, depending on the specific application and material characteristics. The equipment is engineered to handle the unique properties of cement mineral powders, such as their fine particle size, cohesive nature, and potential for dust generation, ensuring safe and effective transport.
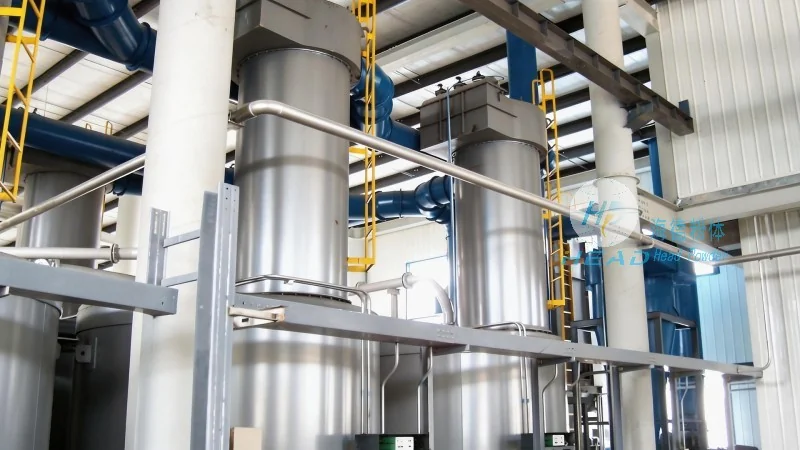
One common mechanism involves the use of screw conveyors, which are particularly effective for vertical or inclined transport of powders. The screw, rotating within a trough, moves the material forward through friction and gravity. This method is ideal for handling dry, free-flowing powders and is often integrated with control systems to regulate speed and flow rate, preventing blockages and maintaining consistent performance. Additionally, pneumatic conveying systems may be employed for longer distances or more complex layouts, using air pressure to transport powders through pipelines. These systems are particularly useful for handling dusty or abrasive materials, as they minimize direct contact and reduce wear on components.
Modern cement mineral powder material handling equipment from HeadPowder is characterized by several key features that enhance performance and reliability. One of the primary advantages is the high efficiency in material transport, with systems designed to minimize energy consumption while maximizing throughput. The equipment is engineered for durability, using high-quality materials and robust construction to withstand the abrasive nature of mineral powders and the demanding operating conditions in industrial settings.
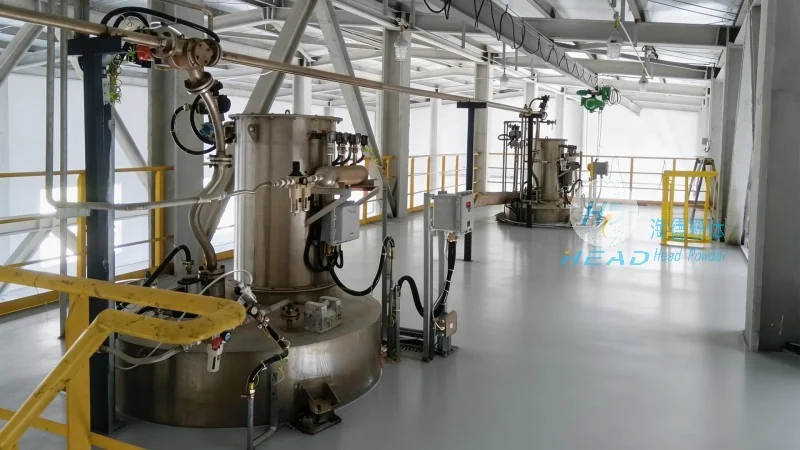
Another significant feature is the integration of advanced control systems, which allow for precise monitoring and adjustment of the transport process. These systems may include sensors to detect material levels, flow rates, and potential blockages, enabling automated responses to maintain optimal operation. The equipment also emphasizes safety, incorporating features such as dust suppression systems and enclosed designs to prevent dust emissions and protect operators from hazardous materials.
Furthermore, the equipment is designed for flexibility and adaptability, allowing for customization to suit various production requirements. Whether for short-distance transport within a plant or long-distance transfer between facilities, the systems can be configured to meet specific needs, including variations in material type, volume, and operational parameters. This adaptability ensures that the equipment remains effective and efficient across different applications and operational scenarios.
The implementation of cement mineral powder material handling equipment offers numerous operational benefits for industrial facilities. By improving the efficiency of material transport, these systems reduce downtime and increase overall productivity. The reliable and consistent performance of the equipment minimizes the risk of material loss or contamination, which is critical in processes where quality control is paramount. Additionally, the advanced control features contribute to energy savings and lower operational costs over time.
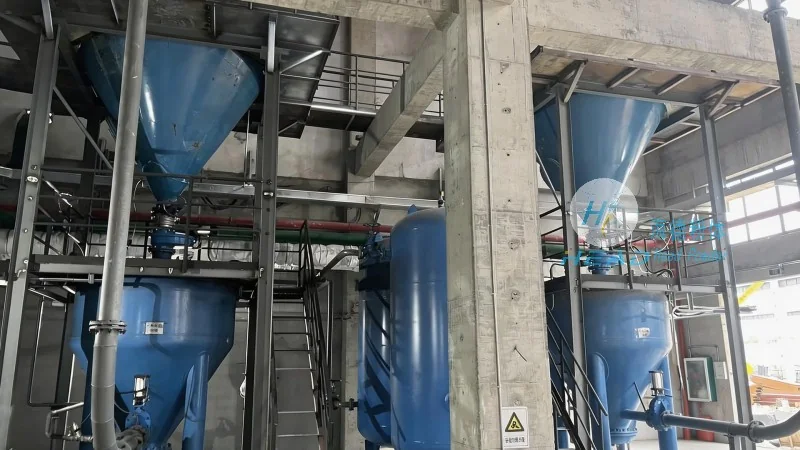
These equipment solutions are widely used in various industries, including cement manufacturing, mineral processing, and chemical production. In cement plants, for example, the equipment is essential for transporting raw materials and finished products, facilitating the production of high-quality cement. In mineral processing facilities, it enables the efficient handling of ore powders, supporting the extraction and processing of valuable minerals. The versatility of the equipment makes it suitable for a range of applications, from small-scale operations to large-scale industrial plants.
Cement mineral powder material handling equipment, as exemplified by the solutions from Shandong HeadPowder Engineering Co., Ltd., represents a critical component in modern industrial operations. By understanding the working principles and leveraging the key features of such equipment, industries can enhance their material handling processes, improve efficiency, and ensure compliance with safety and quality standards. The continued innovation and advancement in this field will further optimize material transport systems, supporting the growth and sustainability of industrial applications worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top