This article introduces the working principle and key features of sodium hypochlorite material handling systems, providing a comprehensive overview for industry professionals and potential clients. The system is designed to efficiently transport sodium hypochlorite, a critical chemical widely used in water treatment, disinfection, and other industrial applications.
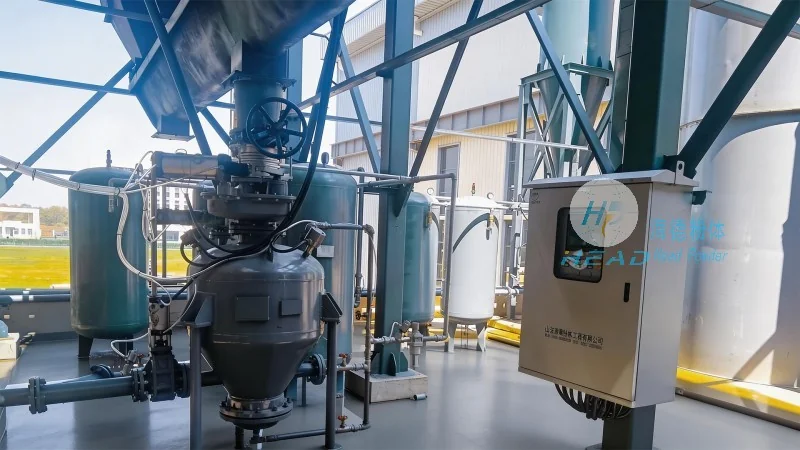
At the core of the system is the sodium hypochlorite solution, which is typically stored in a dedicated tank. The solution is then pumped through a network of pipes and valves to the desired destination. The pumping mechanism, often powered by electric or hydraulic motors, ensures consistent flow rates and pressure levels, maintaining the chemical's stability and effectiveness. This process involves precise control of flow and pressure to prevent degradation or splashing, which is crucial for safety and operational efficiency.
The material handling system incorporates several key components that work in tandem to ensure reliable operation. These include storage tanks, pumps, piping systems, and control valves. The storage tanks are constructed from corrosion-resistant materials, such as stainless steel, to withstand the chemical's aggressive nature and extend the system's lifespan. The pumps, usually centrifugal or positive displacement types, are selected based on the required flow rate and pressure, ensuring optimal performance under varying conditions. The piping system is designed with smooth, non-porous surfaces to minimize chemical buildup and facilitate easy cleaning. Control valves, including ball valves and gate valves, allow for precise regulation of flow and pressure, enabling operators to adjust the system's output as needed.
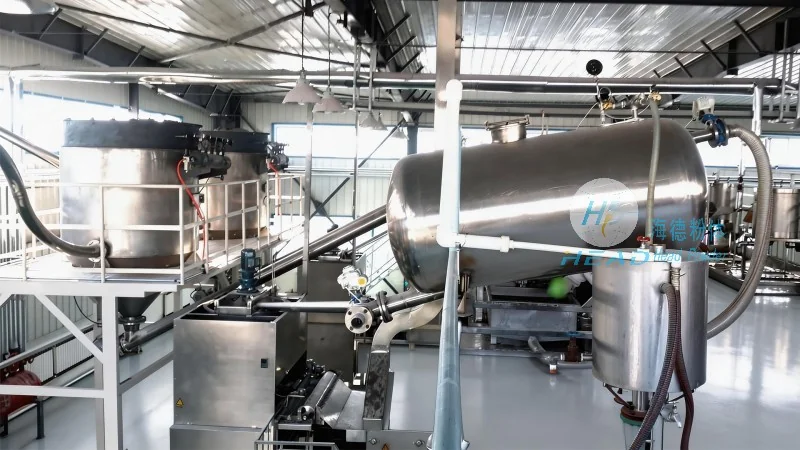
One of the primary advantages of the sodium hypochlorite material handling system is its ability to deliver the chemical in a concentrated form, reducing transportation costs and storage space requirements. The system's design minimizes the need for dilution, as the solution is delivered directly to the point of use, ensuring consistent concentration levels. This feature is particularly beneficial for large-scale industrial applications where high volumes of sodium hypochlorite are required. Additionally, the system's modular design allows for easy expansion or integration with existing infrastructure, providing flexibility for growing businesses.
The system also prioritizes safety and environmental compliance. The use of corrosion-resistant materials and sealed components prevents leaks and spills, reducing the risk of environmental contamination. The control system includes safety interlocks and alarms to alert operators of any abnormal conditions, such as pressure fluctuations or temperature changes. This proactive approach to safety ensures that the system operates within regulatory standards and minimizes the potential for accidents. Furthermore, the system's energy-efficient design reduces operational costs and aligns with sustainability goals, making it an attractive choice for environmentally conscious industries.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in the design, manufacturing, and installation of sodium hypochlorite material handling systems. With years of experience and a commitment to quality, the company has established itself as a trusted partner for businesses seeking reliable and efficient chemical handling solutions. The company's products are engineered to meet the highest industry standards, ensuring durability, performance, and safety. Based in Shandong, China, HeadPowder leverages its local expertise and resources to deliver tailored solutions that address the unique needs of each client. Whether for water treatment plants, industrial facilities, or other applications, the company's systems are designed to enhance operational efficiency and reduce downtime.
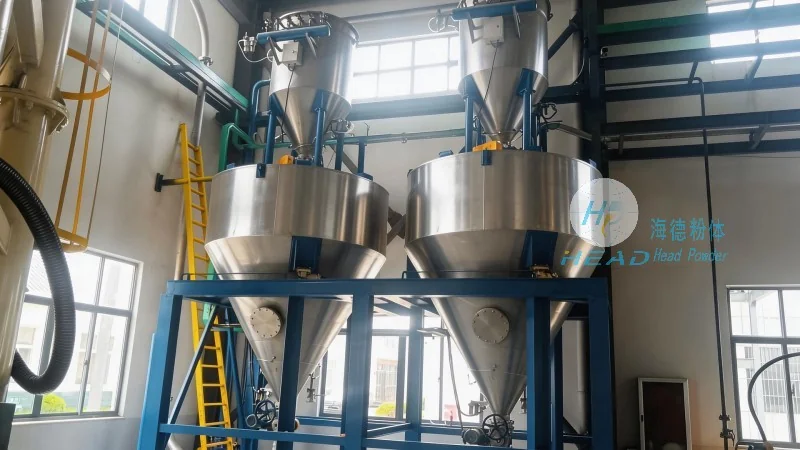
The company's approach to product development is centered on customer needs and technological advancements. By incorporating feedback from clients and staying abreast of industry trends, HeadPowder continuously improves its systems to offer the most effective solutions. The company's team of engineers and technicians work closely with clients to understand their specific requirements, from system capacity to integration with existing equipment. This collaborative process ensures that the final product meets all operational and safety criteria. Additionally, HeadPowder provides comprehensive after-sales support, including maintenance services and technical assistance, to ensure the long-term performance of its systems.
In conclusion, the sodium hypochlorite material handling system is a sophisticated and essential component for industries relying on this chemical. Its efficient design, safety features, and adaptability make it a valuable asset for businesses seeking to optimize their operations. With the expertise and commitment of Shandong HeadPowder Engineering Co., Ltd., companies can access high-quality systems that meet their specific needs and contribute to their success. The combination of advanced technology and reliable service ensures that the system operates at peak performance, delivering consistent results and supporting the growth of the business.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top