Ammonium nitrate is a widely used industrial chemical, and efficient material handling systems are crucial for its safe and effective transportation. This article explores the working principles and key features of modern ammonium nitrate material handling systems, highlighting the technological advancements and operational benefits they offer.
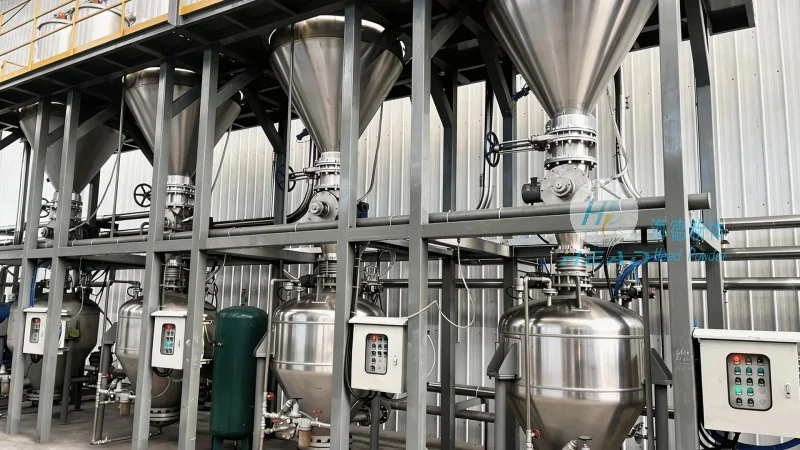
The core working principle of ammonium nitrate material handling systems revolves around the integration of specialized equipment designed to handle the unique properties of ammonium nitrate. These systems typically include components such as feeders, conveyors, storage silos, and control mechanisms. The process begins with the storage of ammonium nitrate in bulk storage silos, where it is kept under controlled conditions to prevent caking or segregation. From the silos, the material is transferred to feeders, which regulate the flow rate and consistency of the material before it enters the conveying system. Conveyors, often using belt or screw mechanisms, transport the ammonium nitrate to processing or packaging areas. Advanced systems may incorporate sensors and automation to monitor flow rates, detect blockages, and adjust operations in real-time, ensuring smooth and continuous material movement. The entire process is designed to maintain the integrity of the ammonium nitrate, minimizing dust generation and ensuring compliance with safety regulations.
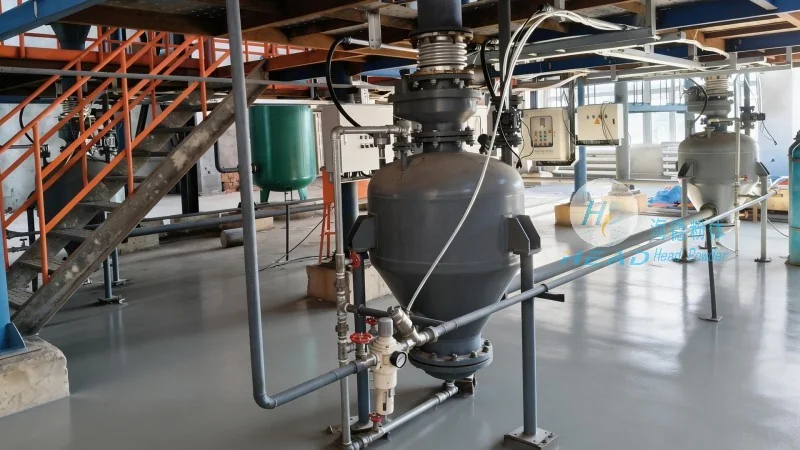
Modern ammonium nitrate material handling systems are characterized by several key features that enhance performance, safety, and efficiency. One of the primary features is the use of dust suppression and containment technologies. Ammonium nitrate is a fine powder that can generate significant dust, which poses health and safety risks. Advanced systems employ enclosed conveyor systems, dust collection units, and air filtration to minimize dust exposure and ensure a safe working environment. Another critical feature is the integration of automation and control systems. These systems use sensors, programmable logic controllers (PLCs), and variable frequency drives (VFDs) to monitor and control various parameters, such as flow rates, pressure, and temperature. Automation allows for precise control over the material handling process, reducing human error and improving operational consistency. Additionally, many systems incorporate material flow monitoring and diagnostic tools. These tools provide real-time data on the system's performance, enabling proactive maintenance and reducing downtime. The use of durable and corrosion-resistant materials is also a key feature, as ammonium nitrate can be corrosive to certain metals. Systems are often constructed with stainless steel or other corrosion-resistant materials to ensure longevity and maintain material purity. Furthermore, safety features, such as emergency stop buttons, overfill protection, and explosion-proof designs, are integral to modern systems, ensuring compliance with industrial safety standards and protecting personnel and equipment.
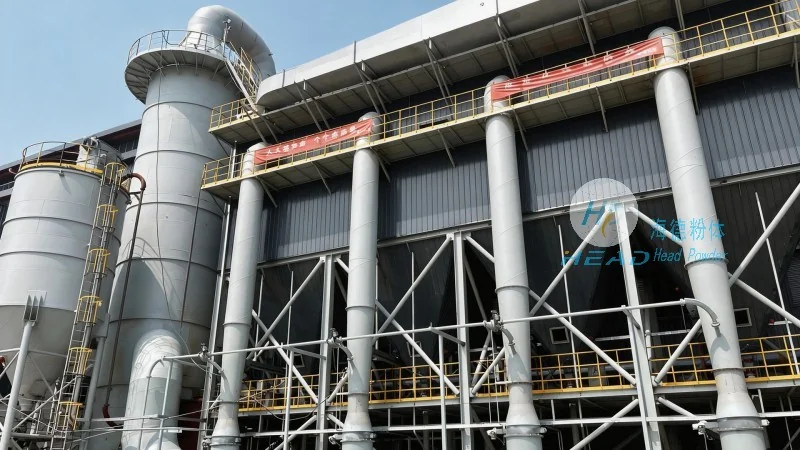
The implementation of advanced ammonium nitrate material handling systems offers numerous operational benefits. These systems improve material flow efficiency, reducing processing times and increasing overall productivity. By minimizing downtime and ensuring consistent material supply, they contribute to higher throughput and better cost management. The safety features integrated into these systems also reduce the risk of accidents, lowering insurance costs and improving workplace safety. Additionally, the use of automation and real-time monitoring enables better decision-making and process optimization. For example, operators can quickly identify and address issues such as blockages or abnormal flow rates, preventing costly delays. The systems are widely used in various industries, including agriculture, where ammonium nitrate is a key component of fertilizers, and in industrial applications where it is used as an oxidizer or in the production of other chemicals. The adaptability of these systems allows them to be customized for different applications, from small-scale operations to large industrial facilities. Overall, the features and working principles of modern ammonium nitrate material handling systems make them essential for the efficient and safe handling of this critical material.
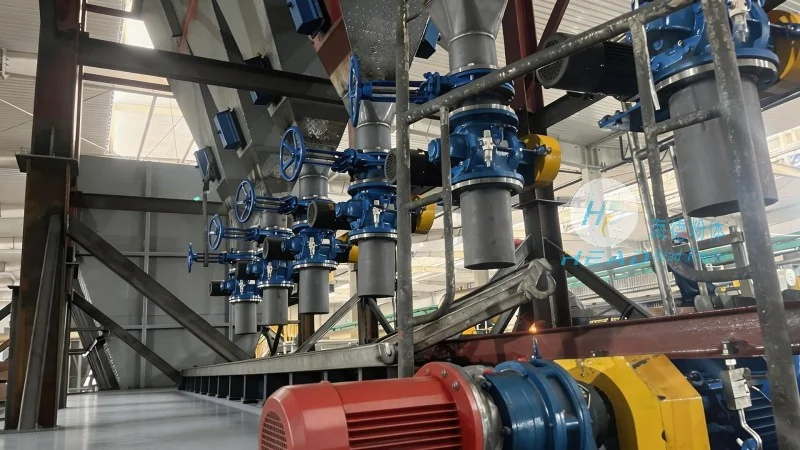
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized material handling solutions for industrial chemicals. With a focus on innovation and safety, the company designs and manufactures advanced systems tailored to the unique needs of industries dealing with ammonium nitrate and other hazardous materials. Headpowder's expertise lies in integrating cutting-edge technology with robust engineering to deliver reliable and efficient material handling solutions. The company's commitment to quality and customer satisfaction has established it as a trusted partner in the chemical processing industry. Based in Shandong, China, headpowder leverages its local expertise and resources to serve clients both domestically and internationally, providing comprehensive support from system design to installation and maintenance. The company's products are designed to meet stringent safety and performance standards, ensuring that clients can operate their facilities with confidence and efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top