For industrial applications, the efficient and reliable transport of cement auxiliary materials is crucial for maintaining production line stability and ensuring product quality. This article explores the working principles and distinctive characteristics of cement auxiliary material conveying systems, providing insights into how these technologies enhance operational efficiency in construction material processing industries.
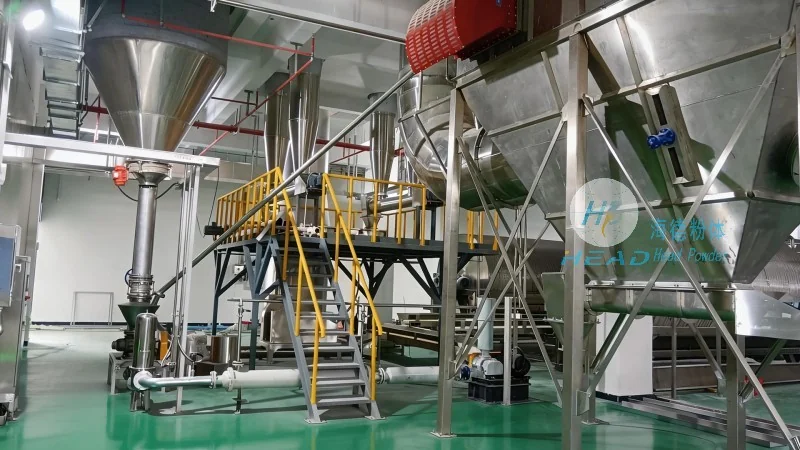
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in the design, manufacturing, and implementation of advanced conveying solutions tailored to the unique demands of cement and related material handling processes. With a focus on precision engineering and robust system design, the company's expertise ensures that auxiliary materials such as limestone, clay, and iron ore are transported with minimal loss and maximum efficiency.
The core working principle of cement auxiliary material conveying involves the use of specialized equipment, including belt conveyors, screw conveyors, and pneumatic systems, which are selected based on the material properties, processing requirements, and environmental conditions. Belt conveyors, for instance, are widely used for bulk material transport due to their high load capacity and ability to handle a variety of particle sizes. These systems operate by utilizing a continuous belt loop that moves material from the loading point to the discharge point, often incorporating idlers, pulleys, and tensioning mechanisms to maintain optimal performance.
Screw conveyors, another common solution, utilize a rotating helical screw to move materials through a trough or pipe. This mechanism is particularly effective for handling dry, free-flowing materials and can be adjusted for different angles and speeds to control the flow rate. The design of screw conveyors allows for compact installations and easy integration into existing production lines, making them a versatile choice for auxiliary material transport.
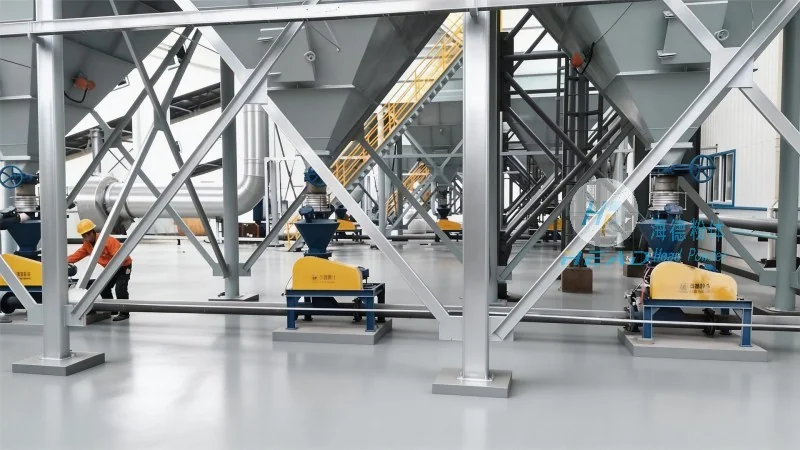
Pneumatic conveying systems, on the other hand, employ air or gas to transport materials in a closed pipeline. This method is ideal for handling fine powders and dusty materials, as it minimizes material degradation and contamination. The system typically consists of a blower, a hopper, and a pipeline network, with the material being drawn into the system by the airflow. Pneumatic conveyors offer advantages such as low maintenance requirements and the ability to transport materials over long distances without the need for multiple transfer points.
Key characteristics of cement auxiliary material conveying systems include high efficiency, which is achieved through optimized equipment selection and system design. These systems are engineered to minimize energy consumption while maximizing material throughput, contributing to cost savings and reduced operational expenses. Reliability is another critical feature, as consistent performance is essential for maintaining production schedules and avoiding downtime. Advanced control systems and monitoring technologies are often integrated into modern conveying solutions to ensure real-time performance tracking and prompt maintenance interventions.
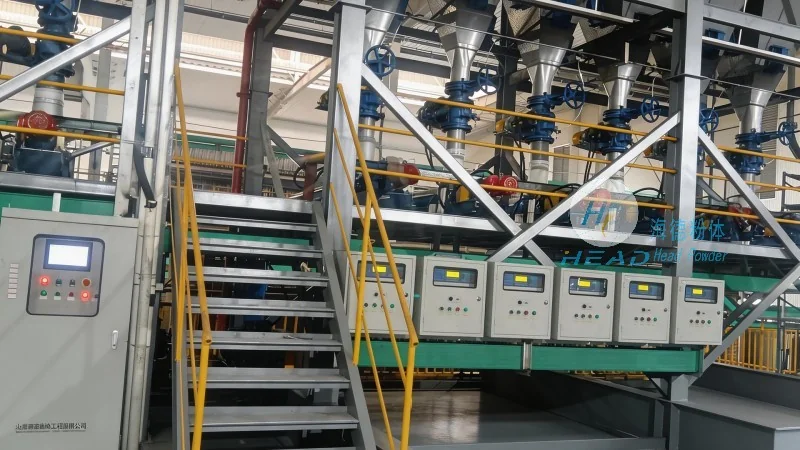
Another important characteristic is adaptability, as auxiliary materials can vary significantly in terms of particle size, moisture content, and bulk density. Modern conveying systems are designed to accommodate these variations through adjustable speed controls, variable pitch screws, and flexible pipeline configurations. This adaptability ensures that the system can handle different material types without the need for extensive modifications, enhancing its versatility and long-term utility.
Environmental considerations also play a role in the design of cement auxiliary material conveying systems. Dust suppression measures, such as sealing and filtration, are commonly incorporated to minimize airborne particulate emissions and comply with environmental regulations. Additionally, energy-efficient motors and sustainable operational practices are adopted to reduce the carbon footprint of the conveying process, aligning with industry standards for sustainable manufacturing.
In conclusion, the working principles and characteristics of cement auxiliary material conveying systems are integral to the efficient operation of cement production facilities. By leveraging advanced engineering and tailored solutions, companies like Shandong HeadPowder Engineering Co., Ltd. ensure that auxiliary materials are transported safely, reliably, and efficiently. The combination of high performance, adaptability, and environmental responsibility makes these systems essential for modern cement processing, supporting the industry's commitment to quality and sustainability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top