Barley material handling systems are essential in agricultural and food processing industries, designed to efficiently transport, store, and manage barley grains from harvest to processing. These systems integrate advanced engineering and material handling technologies to ensure optimal performance and reliability. The following sections explore the core working principles and key features that define modern barley material handling solutions.
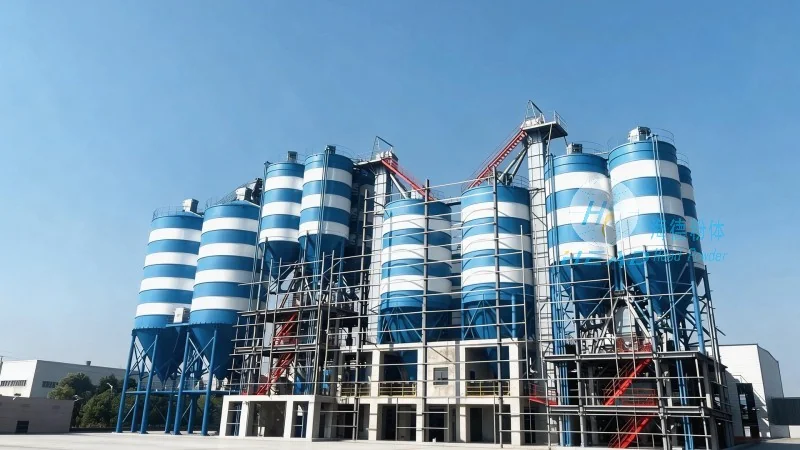
Barley material handling systems are specialized equipment and processes used to handle barley in various stages of production. From field collection to storage and subsequent processing, these systems play a critical role in maintaining grain quality and operational efficiency. The design of these systems is tailored to the physical properties of barley, such as its size, density, and moisture content, ensuring that handling operations are conducted with minimal damage and maximum throughput.
The working principle of barley material handling systems revolves around the use of mechanical and gravitational forces to move barley through different stages. Common components include conveyor belts, bucket elevators, and pneumatic conveying systems, each serving a specific function in the overall material flow. For instance, conveyor belts are typically used for horizontal or slight incline transport, while bucket elevators are employed for vertical lifting and horizontal transfer. Pneumatic systems, on the other hand, utilize air pressure to transport barley in a dust-free environment, which is particularly beneficial for maintaining grain quality and reducing contamination risks.
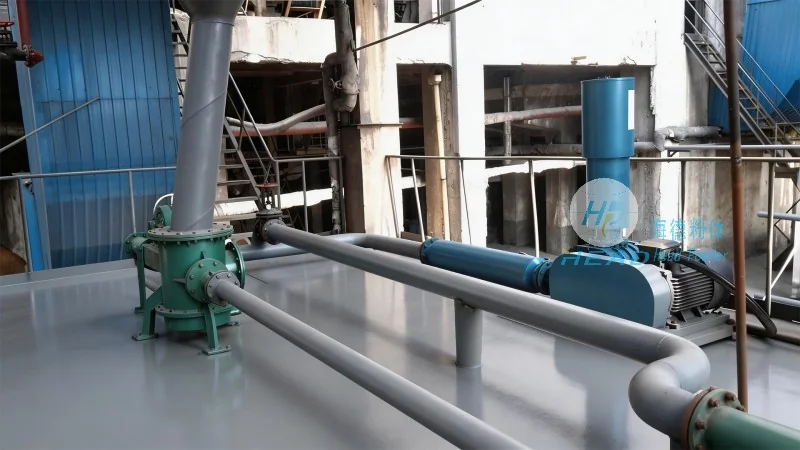
Modern barley material handling solutions are characterized by several distinctive features that enhance their performance and adaptability. One key feature is the integration of automation and control systems, which allow for real-time monitoring and adjustment of material flow rates. This automation helps in optimizing energy consumption and reducing operational costs while ensuring consistent processing quality. Another notable feature is the use of durable and corrosion-resistant materials in the construction of handling equipment, such as stainless steel and high-grade plastics, which are resistant to the abrasive nature of barley and harsh environmental conditions.
Efficiency and reliability are paramount in barley material handling operations. The systems are engineered to minimize downtime and maximize throughput, which is crucial for meeting production demands in agricultural and food processing facilities. Advanced sensors and feedback mechanisms are incorporated to detect and address any disruptions in the material flow, ensuring continuous operation. Additionally, the design of these systems emphasizes ease of maintenance, with modular components that can be easily replaced or serviced, reducing maintenance time and costs.
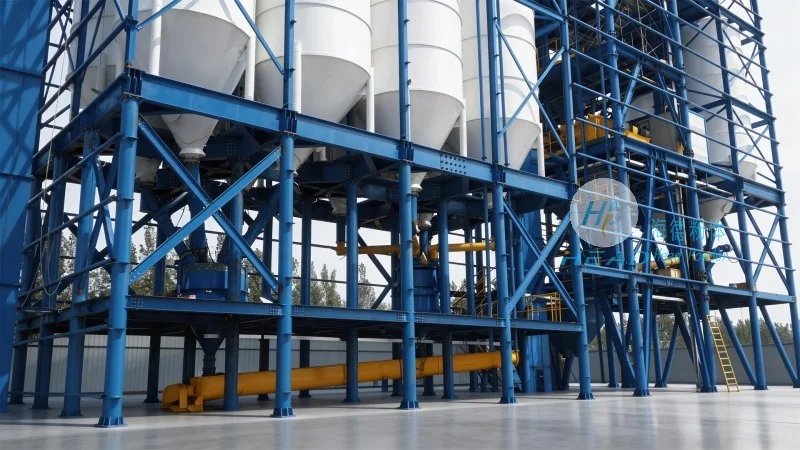
Barley material handling systems are highly customizable to meet the specific needs of different applications. Whether for small-scale farms or large industrial processing plants, these systems can be tailored to handle varying volumes and types of barley. The modular design allows for the integration of additional components, such as sorting or cleaning mechanisms, to enhance the overall functionality of the system. This adaptability ensures that the system can evolve with changing production requirements and technological advancements.
Barley material handling systems represent a critical component in the efficient management of barley from field to processing. The integration of advanced working principles and distinctive features ensures that these systems deliver high performance, reliability, and adaptability. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized barley material handling solutions that meet the unique needs of agricultural and food processing industries. HeadPowder, with its headquarters in Shandong, China, leverages advanced engineering and manufacturing capabilities to deliver high-quality, reliable systems. The company's commitment to innovation and customer-centric solutions ensures that clients receive tailored equipment that enhances operational efficiency and grain quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top