Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in the design, development, and production of negative pressure dilute phase powder conveying equipment. The company is located in Shandong, China, and has been committed to providing high-quality solutions for powder handling and transportation in various industries. This article will introduce the working principle and key features of this equipment, helping readers understand its application and advantages.
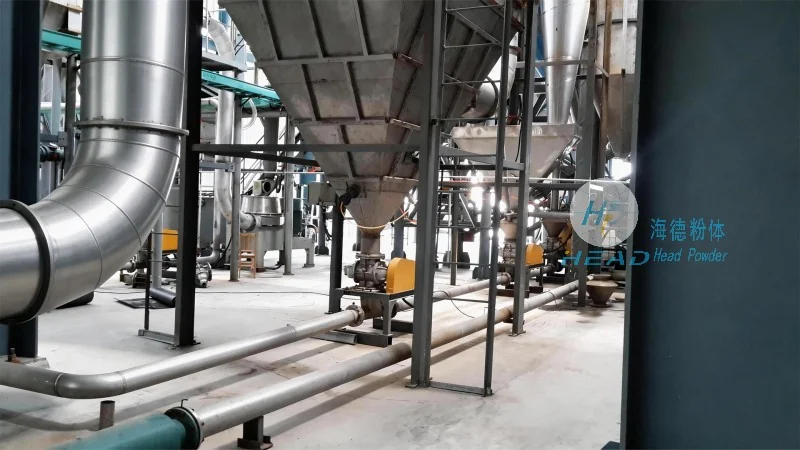
Shandong HeadPowder Engineering Co., Ltd. is a leading enterprise in the field of powder conveying technology. The company's headquarters is situated in Shandong, China, where it has established a comprehensive production and research base. With years of experience and continuous innovation, HeadPowder has become a trusted partner for customers seeking efficient and reliable powder handling solutions. The company's products are widely used in industries such as food, chemical, pharmaceutical, and cement, meeting the diverse needs of different sectors.
The negative pressure dilute phase powder conveying equipment operates based on the principle of creating a negative pressure environment in the conveying pipeline. This is achieved by using a vacuum pump or other suction devices to generate a pressure difference between the conveying system and the external environment. The equipment draws the powder material from the source, such as a hopper or storage tank, and transports it through the pipeline under the action of the negative pressure. The key components of this system include a vacuum pump, a conveying pipeline, a filter system, and a control unit. The vacuum pump continuously extracts air and powder particles from the pipeline, maintaining a stable negative pressure to ensure the smooth flow of the material. The filter system is designed to separate the powder from the air, preventing dust pollution and ensuring the purity of the conveyed material. The control unit monitors the pressure, flow rate, and other parameters, allowing for real-time adjustment and optimization of the conveying process.
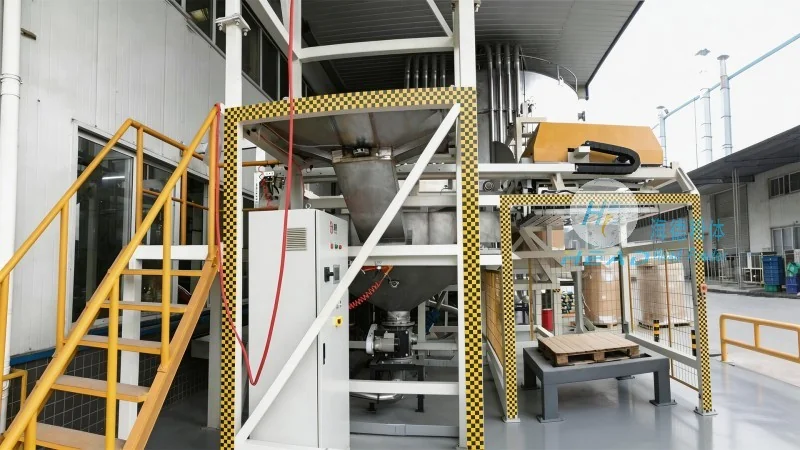
1. Efficient and Stable Conveying: The equipment can transport powder materials over long distances with high efficiency and stability. The negative pressure system ensures that the material is conveyed continuously without interruption, reducing the risk of material accumulation or blockage. The dilute phase design allows for a lower material concentration in the pipeline, which minimizes the risk of clogging and improves the overall conveying performance.
2. Low Energy Consumption: Compared to other conveying methods, such as positive pressure or pneumatic conveying with high pressure, the negative pressure system consumes less energy. The vacuum pump operates at a lower pressure, resulting in reduced energy costs and lower operating expenses for the user.
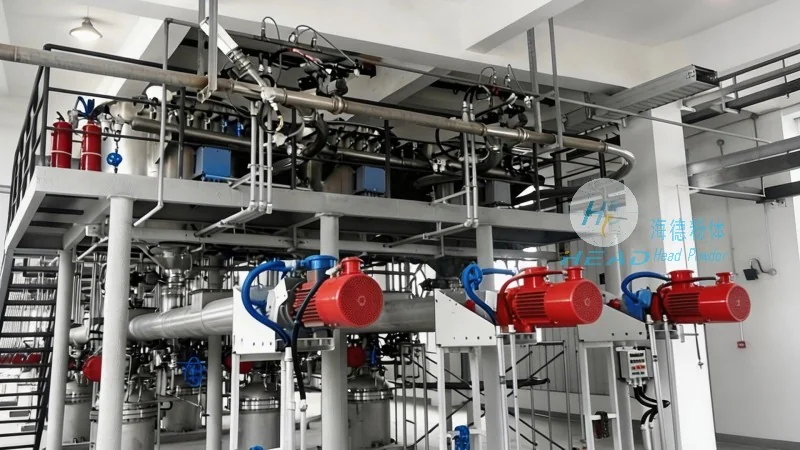
3. Wide Application Range: The equipment is suitable for conveying various types of powder materials, including fine powders, granules, and bulk materials. It can handle materials with different particle sizes, moisture contents, and flow properties, making it a versatile solution for different industries. The system can also be customized to meet specific customer requirements, such as different conveying distances, material types, and environmental conditions.
4. Environmental Protection: The negative pressure system is designed to minimize dust pollution and environmental impact. The filter system effectively separates the powder from the air, preventing dust emissions into the atmosphere. This helps to comply with environmental regulations and maintain a clean working environment. Additionally, the equipment is equipped with safety features, such as pressure relief valves and overcurrent protection, to ensure safe operation and prevent accidents.
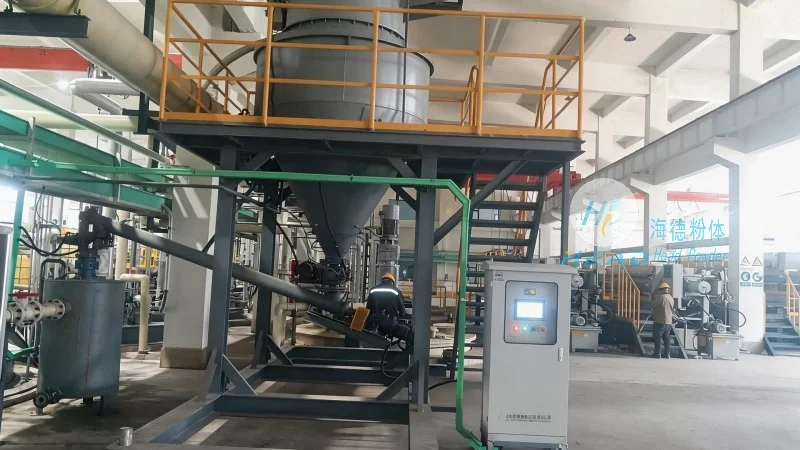
HeadPowder's negative pressure dilute phase powder conveying equipment is designed with advanced technology and high-quality materials to ensure durability and reliability. The equipment features a compact structure, easy installation, and low maintenance requirements. The vacuum pump is equipped with a high-efficiency motor and a robust impeller, providing stable and efficient suction. The conveying pipeline is made of corrosion-resistant materials, such as stainless steel or polyethylene, to prevent material corrosion and ensure long service life. The filter system uses high-efficiency filters, such as HEPA or activated carbon filters, to achieve high filtration efficiency and maintain the purity of the conveyed material. The control unit is equipped with a user-friendly interface, allowing for easy operation and monitoring of the conveying process. The equipment is also designed with safety features, such as pressure sensors and emergency stop buttons, to ensure safe operation and prevent accidents.
In conclusion, the negative pressure dilute phase powder conveying equipment is an efficient and reliable solution for powder handling and transportation. It offers advantages such as stable conveying, low energy consumption, wide application range, and environmental protection. HeadPowder's products are designed with advanced technology and high-quality materials, ensuring durability and reliability. The company's commitment to innovation and customer satisfaction has made it a leading provider of powder conveying solutions in the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top