HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and installation of efficient dust and powder conveying systems. This article delves into the fundamental working principles and key characteristics of such systems, offering insights into their operational efficiency and practical applications.
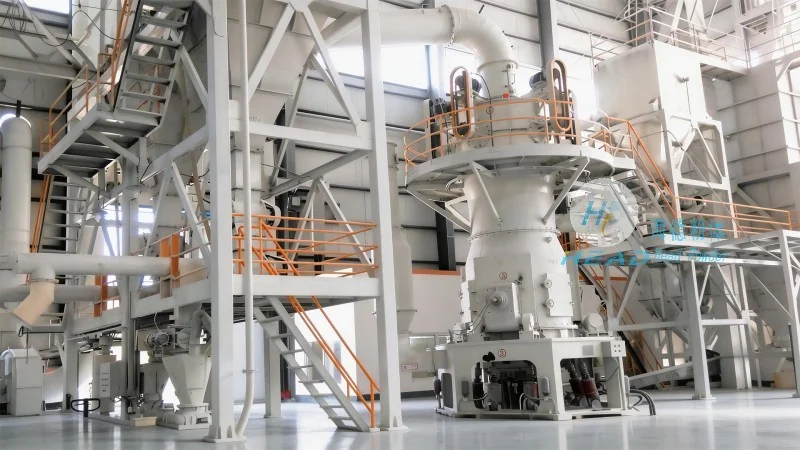
The core working principle of dust and powder conveying systems revolves around the transport of particulate materials from a source to a destination through a closed or semi-closed pipeline. These systems typically employ mechanical forces, such as air pressure or vacuum, to move the material. The process begins with the material being fed into the system, often through a hopper or feeder, where it is then introduced into the conveying line. The system uses a combination of air flow and mechanical components, like rotary valves or blowers, to create the necessary pressure differential or vacuum to propel the material forward. The design of the pipeline, including the selection of appropriate materials and internal diameters, plays a crucial role in ensuring smooth and efficient transport, minimizing material degradation and system wear.
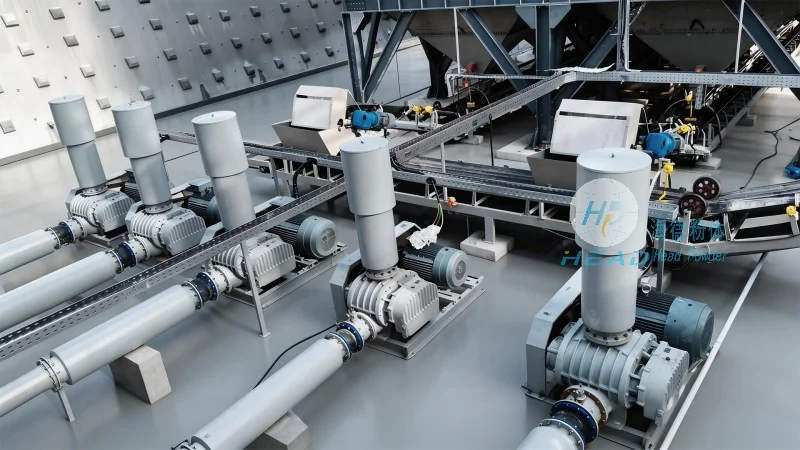
Efficient dust and powder conveying systems exhibit several distinct characteristics that contribute to their effectiveness in various industrial applications. One of the primary characteristics is their ability to handle a wide range of particle sizes and densities, from fine powders to larger granules. This versatility makes them suitable for diverse industries, including pharmaceuticals, food processing, and chemical manufacturing. Another critical characteristic is the system's ability to maintain material integrity during transport. Advanced designs incorporate features like low shear and gentle handling mechanisms to prevent agglomeration or degradation of the material, which is essential for maintaining product quality. Additionally, these systems are designed for high efficiency and low energy consumption, with optimized air flow and pressure management to reduce operational costs. The closed system design also ensures environmental safety by containing dust and preventing emissions, aligning with modern industrial standards for air quality and occupational health.
HeadPowder's dust and powder conveying systems offer several operational advantages that enhance productivity and reliability in industrial settings. The systems are engineered for continuous operation, minimizing downtime and ensuring consistent material flow. Their modular design allows for easy integration into existing production lines and facilitates maintenance and repairs. The use of durable materials and robust components ensures long-term performance and reduces the need for frequent replacements. These systems are widely applied in industries where material transport is a critical step, such as in the production of powders, granules, and bulk materials. By providing a reliable and efficient means of conveying, these systems contribute to improved overall process efficiency and reduced operational costs.
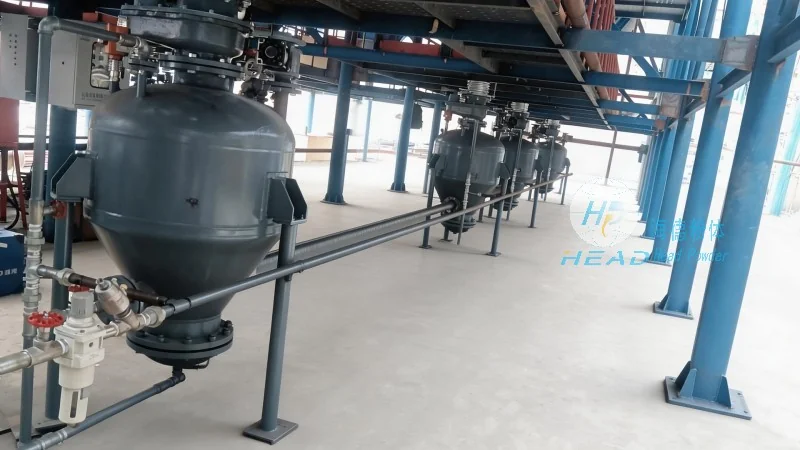
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a reputable company dedicated to delivering high-quality dust and powder conveying solutions. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the material handling industry. The company's expertise lies in designing customized systems that meet the specific needs of clients, ensuring optimal performance and reliability. By adhering to strict quality standards and leveraging advanced technology, HeadPowder continues to provide effective solutions for the efficient transport of dust and powders, supporting the growth and success of its clients in various industrial sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top