For agricultural operations dealing with sorghum, an efficient material handling system is crucial for optimizing workflow and ensuring consistent quality. A sorghum material handling system encompasses various components designed to transport, store, and process sorghum from the field to the processing facility. This system is essential for managing the entire sorghum handling process, from harvesting to final product distribution. Understanding the components and design principles of such a system can significantly enhance operational efficiency and reduce labor costs. HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., specializes in designing and manufacturing tailored material handling systems for sorghum processing, helping businesses achieve optimal performance and productivity.
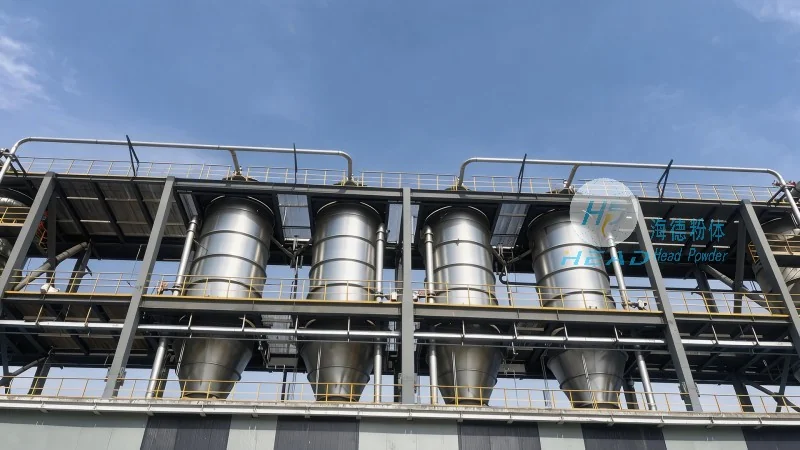
The core components of a sorghum material handling system typically include conveyors, elevators, storage silos, and processing equipment. Conveyors, such as belt conveyors or chain conveyors, are used to transport sorghum from one location to another within the facility. Elevators, like bucket elevators or screw conveyors, are employed to lift sorghum vertically, often from ground level to storage silos or processing areas. Storage silos are critical for bulk storage, allowing for controlled release of sorghum as needed. Processing equipment may include cleaning machines, dehusking units, and grinding or milling systems, depending on the final product requirements.
The design of a sorghum material handling system follows several key principles to ensure optimal performance. First, the system must be tailored to the specific characteristics of sorghum, including its moisture content, bulk density, and potential for dust generation. This involves selecting appropriate equipment that can handle the material's properties without causing degradation or loss. Second, the system should be designed for scalability, allowing for future expansion as the operation grows. This includes modular components that can be added or modified without major reconfigurations. Third, energy efficiency is a critical design consideration, as reducing energy consumption lowers operational costs and aligns with sustainability goals. Finally, safety is paramount, with features like enclosed conveyors, dust suppression systems, and emergency stop mechanisms to protect workers and prevent accidents.
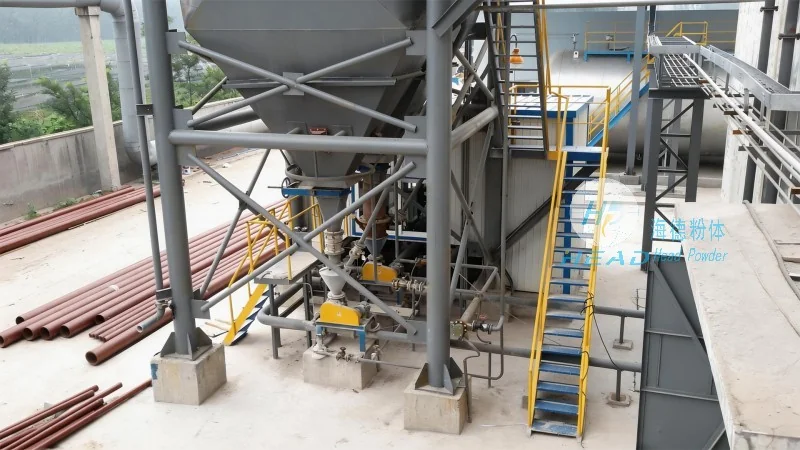
In the context of sorghum processing, the material handling system plays a vital role in maintaining product quality and consistency. Proper handling minimizes the risk of damage to the grain, which can affect its market value and usability. For example, gentle handling during transport and storage helps preserve the grain's texture and nutritional content. Additionally, an efficient system ensures that the processing line operates smoothly, reducing downtime and increasing overall throughput. This is particularly important for commercial operations where consistent output is essential for meeting market demands.
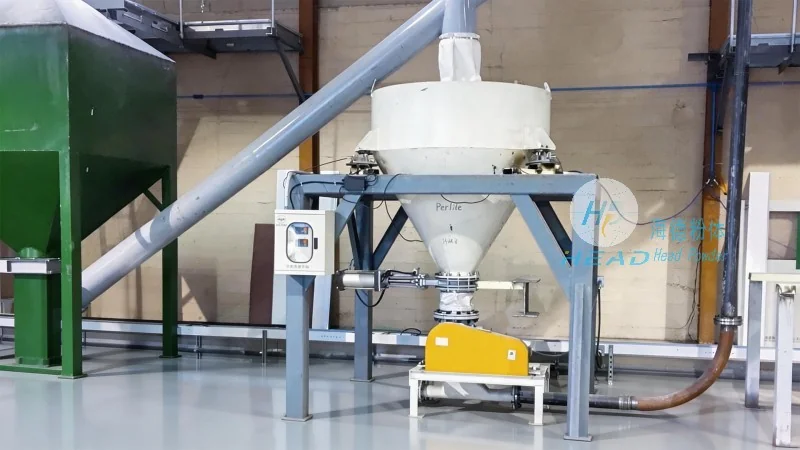
Many sorghum material handling systems are designed to integrate seamlessly with existing processing lines. This integration allows for a streamlined workflow, where the handling system feeds directly into the processing equipment without manual intervention. Customization is a key aspect, as each operation may have unique requirements based on the type of sorghum being processed (e.g., grain sorghum for ethanol production versus forage sorghum for animal feed). The system may include specialized components such as destoners for removing stones or separators for separating different grain sizes. These customizations ensure that the system meets the specific needs of the operation while maintaining efficiency and reliability.
Implementing an optimized sorghum material handling system offers numerous benefits for agricultural businesses. Primarily, it enhances operational efficiency by reducing the time and labor required for material transport and storage. This leads to lower labor costs and increased productivity. Additionally, the system improves product quality by minimizing handling-related damage and maintaining consistent moisture levels. This is crucial for meeting quality standards and ensuring customer satisfaction. Furthermore, an efficient system reduces energy consumption and operational costs, contributing to better financial performance and sustainability. Finally, the scalability of the system allows businesses to adapt to changing market demands and expand their operations as needed.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top