For professionals in the construction and industrial sectors, understanding specialized equipment like the silica fume powder conveying system is crucial for optimizing material handling processes. This equipment is designed to efficiently transport silica fume, a fine powder widely used as a supplementary cementitious material in concrete production. The system combines advanced engineering with practical application to ensure reliable and safe material movement, addressing the unique challenges of handling such powders.
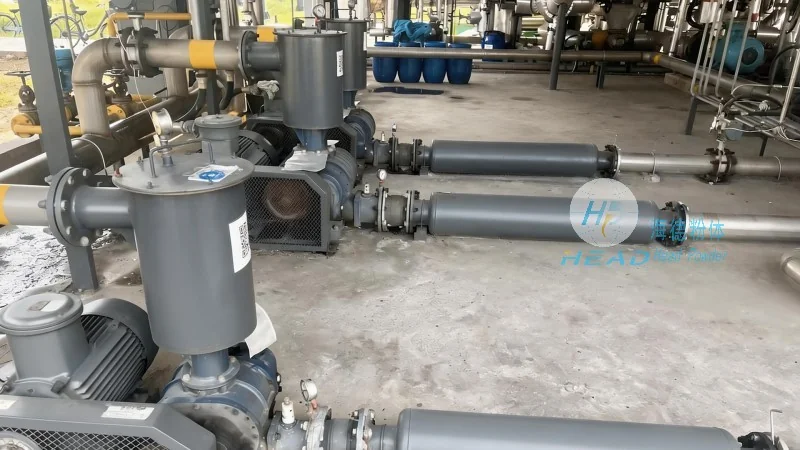
Silica fume, also known as microsilica, is a byproduct of silicon metal or ferrosilicon production. It consists of extremely fine particles that enhance concrete's strength, durability, and resistance to chemical attacks. However, due to its fine particle size and high dust content, transporting silica fume requires specialized equipment to prevent clogging, dust dispersion, and operational inefficiencies. The silica fume powder conveying system is engineered to meet these demands, providing a solution that ensures consistent material flow and minimal environmental impact.
The system typically comprises several critical components that work in tandem to achieve efficient material transport. These include a hopper for material storage, a feeder to control the flow rate, a conveyor system (such as a screw conveyor or pneumatic conveyor) to move the powder, and a dust collection system to maintain air quality. Each component is designed with the specific properties of silica fume in mind, ensuring compatibility and optimal performance.
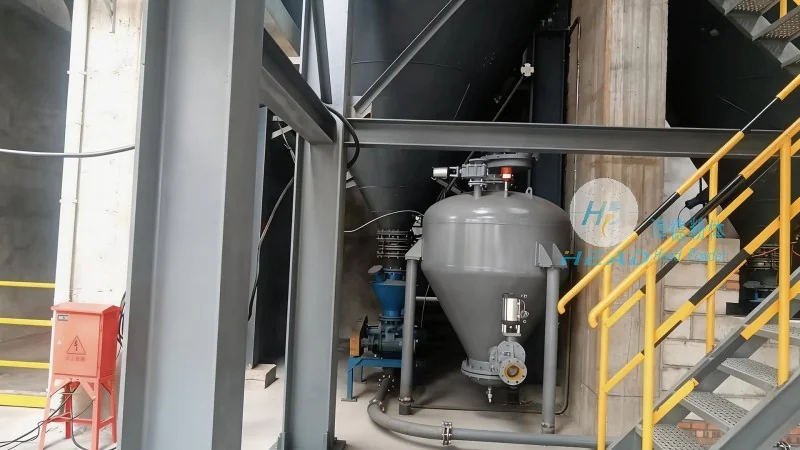
The design of a silica fume powder conveying system is guided by several key principles aimed at maximizing efficiency, safety, and reliability. One of the primary principles is the prevention of material bridging and clogging in the hopper and feeder. This is achieved through the use of specialized hopper designs, such as conical or wedge-shaped hoppers, and the incorporation of vibration or air-assist mechanisms to break up agglomerates. Another critical principle is the control of air flow and pressure within the system, which is essential for maintaining consistent material transport in pneumatic conveyors. Proper sealing and filtration are also integral to the design, ensuring that dust is contained and that the system operates within safe environmental limits.
Implementing a silica fume powder conveying system offers numerous advantages for industrial operations. Firstly, it enhances material handling efficiency by reducing downtime caused by clogging or material loss. The system’s ability to maintain consistent flow rates ensures that production processes are not interrupted, leading to improved productivity. Secondly, it improves safety by containing dust and preventing exposure to fine particles, which can be harmful to workers. The enclosed design of the system minimizes the risk of dust dispersion into the workplace, contributing to a healthier working environment. Additionally, the system’s modular design allows for easy integration with existing production lines, reducing installation time and costs.
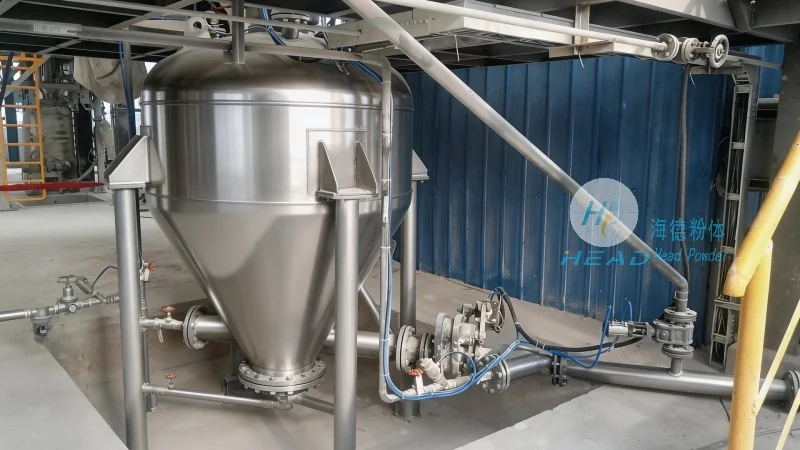
The silica fume powder conveying system is widely used in various industries that rely on concrete production and material processing. In the construction industry, it is essential for ready-mix concrete plants, precast concrete manufacturers, and infrastructure projects that require high-performance concrete. The system is also utilized in the chemical and pharmaceutical industries for handling fine powders, where consistent material flow and dust control are critical. Furthermore, it plays a role in the production of refractory materials and specialty cements, where silica fume is used as a key additive to enhance product properties.
In conclusion, the silica fume powder conveying system is a vital piece of equipment for industries that handle fine powders, particularly silica fume. Its design principles focus on efficiency, safety, and reliability, ensuring that material is transported effectively while minimizing operational risks. For companies seeking to optimize their material handling processes, investing in a well-designed conveying system is a strategic decision that can lead to improved productivity and reduced costs. Shandong HeadPowder Engineering Co., Ltd., a leading provider of such systems, specializes in engineering solutions tailored to the unique needs of industrial applications. With a focus on quality and innovation, HeadPowder offers systems that meet the highest standards of performance and safety, supporting clients in achieving their operational goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top