For industries dealing with bulk powder handling, the efficiency and reliability of material transport systems are critical. An unmanned feeding powder material conveyor, also known as an automated powder conveyor, represents a sophisticated solution designed to handle the challenges of transporting bulk powders without human intervention. This equipment is engineered to ensure seamless, continuous operation, minimizing downtime and enhancing overall production efficiency. In this article, we explore the fundamental aspects of such conveyors, focusing on their design principles and operational capabilities.
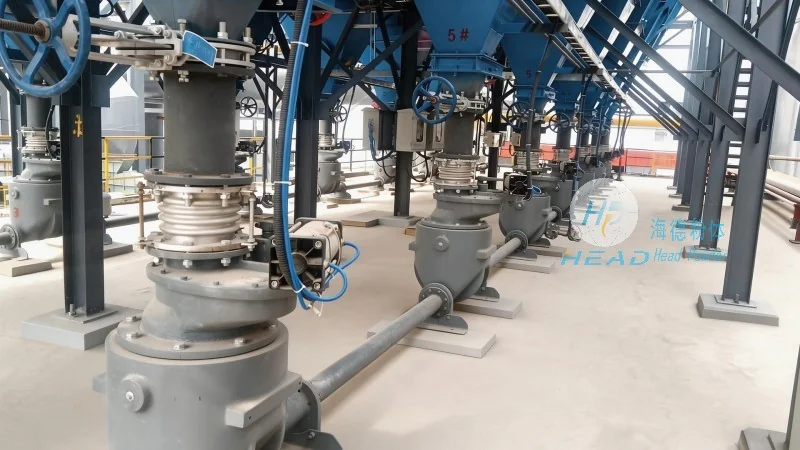
The design of an unmanned feeding powder material conveyor integrates several key components that work in harmony to achieve efficient material handling. These components include a hopper for material storage, a feeding mechanism (such as a screw feeder or vibratory feeder) to control the flow rate, a conveyor system (like a pneumatic or mechanical conveyor) to transport the powder, and a control system to manage the entire process. The hopper is typically designed with a large capacity to accommodate bulk quantities of powder, ensuring a steady supply to the feeder. The feeding mechanism is crucial as it regulates the discharge rate, preventing overloading or underloading of the conveyor. The conveyor system, whether pneumatic (using air pressure) or mechanical (using belts or screws), is selected based on the properties of the powder, such as its density, moisture content, and flowability. The control system, often equipped with sensors and automation software, monitors the process parameters and adjusts the feeding rate in real-time, ensuring optimal performance.
The design principles of an unmanned feeding powder material conveyor are centered on several key objectives: efficiency, reliability, and adaptability. Efficiency is achieved through continuous operation without the need for manual intervention, reducing labor costs and increasing production throughput. Reliability is ensured by robust construction and automated controls, minimizing the risk of material spillage or system failure. Adaptability is achieved by designing the system to handle a wide range of powder types and sizes, making it suitable for various industrial applications. The conveyor's design also emphasizes safety, incorporating features like emergency stop buttons and overload protection to prevent accidents and equipment damage. Additionally, the system is engineered for easy maintenance, with accessible components that can be serviced without extensive downtime.
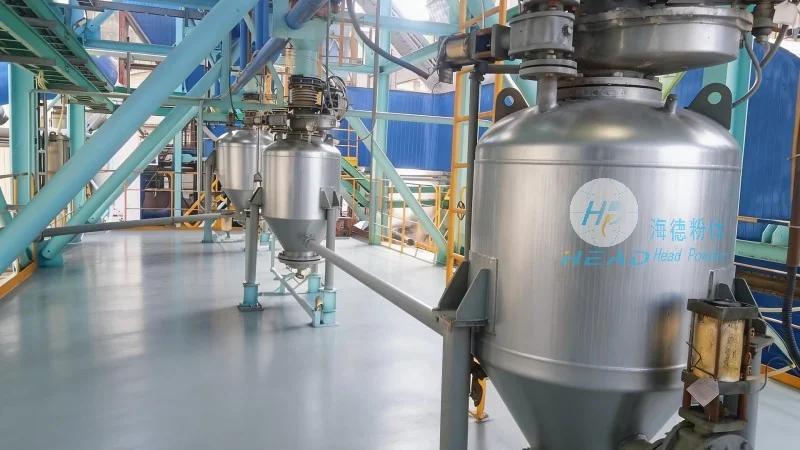
The operational workflow of an unmanned feeding powder material conveyor involves several steps that ensure smooth material transport. First, the bulk powder is loaded into the hopper. The control system then activates the feeding mechanism, which regulates the flow rate based on the desired output. The powder is then transported through the conveyor system to the destination point, such as a processing unit or storage container. Throughout the process, sensors monitor key parameters like flow rate, pressure, and temperature, providing real-time data to the control system. If any deviations are detected, the system automatically adjusts the feeding rate or stops the conveyor to prevent issues. This automated workflow ensures consistent and reliable material handling, reducing the need for manual monitoring and intervention.
Unmanned feeding powder material conveyors are widely used in various industries that require bulk powder handling. These include pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, such systems are used to transport raw materials and finished products, ensuring compliance with stringent quality and safety standards. In food processing, they handle ingredients like flour, sugar, and spices, maintaining hygiene and preventing contamination. In chemical manufacturing, they transport powders like catalysts and reagents, ensuring precise dosing and minimizing waste. In mining, they are used to transport ore and other materials from storage to processing equipment, improving operational efficiency. The versatility of these systems makes them suitable for a wide range of applications, providing a reliable solution for industries that demand consistent and efficient material transport.
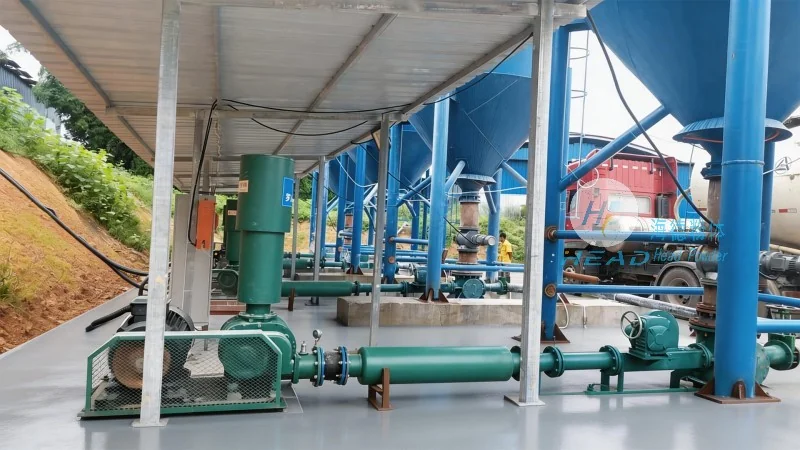
There are several advantages to using an unmanned feeding powder material conveyor. One of the primary benefits is increased efficiency, as the system operates continuously without the need for manual labor. This reduces labor costs and increases production throughput, making it a cost-effective solution for industries with high material handling demands. Another advantage is improved safety, as the system minimizes the risk of human error and accidents associated with manual handling. The automated controls also ensure consistent material flow, reducing the risk of overloading or underloading, which can lead to equipment damage or production delays. Additionally, the system is designed for easy maintenance, with accessible components that can be serviced without extensive downtime. This reduces maintenance costs and ensures the system remains operational for longer periods. Finally, the system is highly adaptable, allowing it to handle a wide range of powder types and sizes, making it suitable for various industrial applications.
Unmanned feeding powder material conveyors play a crucial role in modern industries by providing a reliable and efficient solution for bulk powder handling. The design principles behind these systems, including robust construction, automated controls, and adaptability, ensure that they can meet the demands of various industrial applications. The operational workflow is streamlined, with real-time monitoring and adjustments to maintain optimal performance. The advantages of using such systems, including increased efficiency, improved safety, and reduced maintenance costs, make them a valuable asset for industries dealing with bulk powders. As technology continues to advance, these systems are likely to become even more sophisticated, offering further improvements in performance and reliability. For companies like Shandong HeadPowder Engineering Co., Ltd., based in China, these conveyors represent a key product in their portfolio, designed to meet the evolving needs of modern industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top