Heavy powder material conveying systems are specialized industrial equipment designed to transport bulk powders efficiently and reliably over long distances. These systems are crucial in various industries such as mining, chemical processing, food production, and pharmaceuticals, where the handling of large volumes of fine or heavy powders is a daily operation. The primary goal of these systems is to ensure that powders are moved from one location to another with minimal loss, contamination, and energy consumption. Understanding the components and design principles of such systems is essential for optimizing operational efficiency and maintaining product quality. Developed by companies like Shandong HeadPowder Engineering Co., Ltd., these systems are engineered to meet the specific needs of different industries.
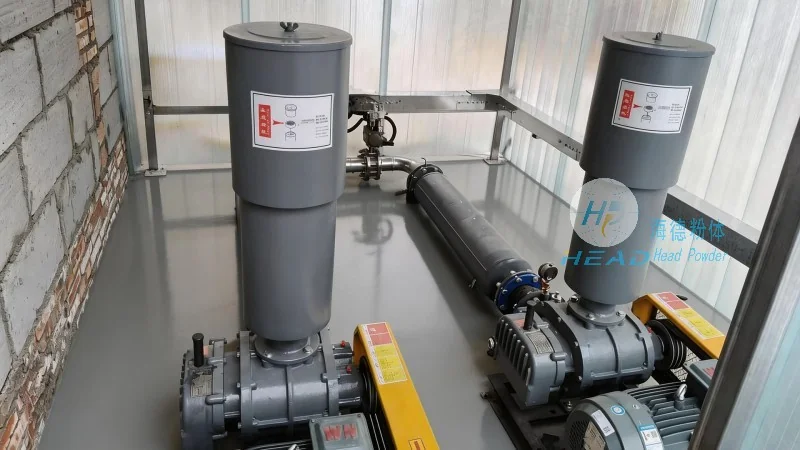
At the core of any heavy powder material conveying system is the ability to handle materials that are difficult to transport due to their physical properties. These materials often include fine powders, granules, or bulk solids that can be prone to caking, segregation, or dust generation. The design of these systems must address these challenges to ensure safe and effective operation. The system typically consists of several key components, including feeders, conveyors, control systems, and accessories, all working in tandem to achieve the desired material flow.
The first component in a typical heavy powder conveying system is the feeder. This device is responsible for feeding the material into the conveyor at a controlled rate. There are various types of feeders, such as screw feeders, vibratory feeders, and rotary valves, each suited for different material characteristics and flow rates. The choice of feeder depends on factors like the bulk density, flowability, and moisture content of the powder. For example, a screw feeder is often used for cohesive materials, while a vibratory feeder is suitable for free-flowing powders. The feeder ensures a consistent and uniform material supply, which is critical for maintaining the performance of the conveyor.
The next major component is the conveyor itself. Heavy powder conveying systems commonly use pneumatic or mechanical conveyors. Pneumatic conveyors utilize air pressure to move powders through a pipeline, while mechanical conveyors rely on mechanical forces like belts, buckets, or screws. The selection of the conveyor type depends on the distance to be covered, the material's properties, and the required capacity. For long-distance transport, pneumatic systems are often preferred due to their ability to handle high volumes and overcome significant vertical or horizontal distances. Mechanical conveyors, on the other hand, are more suitable for shorter distances and can handle a wider range of materials, including those with high moisture content or abrasive properties.
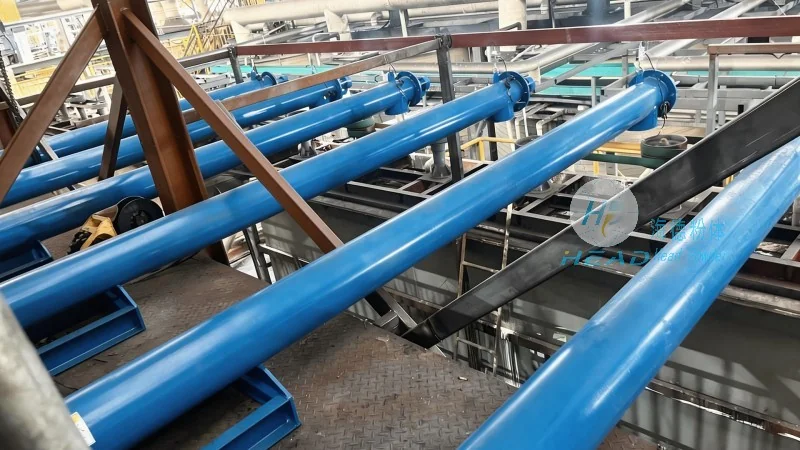
The design principles of a heavy powder material conveying system revolve around several key factors that ensure optimal performance. One of the most critical principles is the minimization of material degradation and loss. This is achieved through the use of smooth, non-stick surfaces in the conveyor and feeder components, as well as proper sealing to prevent dust leakage. The system must also be designed to prevent segregation, where different particle sizes or densities separate during transport. This can be mitigated by using conveyor designs that maintain a consistent flow, such as the use of a continuous belt or a screw conveyor that mixes the material as it moves.
Another important design principle is energy efficiency. Heavy powder conveying systems can consume significant amounts of energy, especially when operating over long distances or with high material loads. To address this, manufacturers often incorporate energy-saving features such as variable speed drives, which adjust the conveyor speed based on the material flow rate. This not only reduces energy consumption but also allows for better control over the material handling process. Additionally, the use of efficient air compressors and proper pipeline design can further enhance energy efficiency.
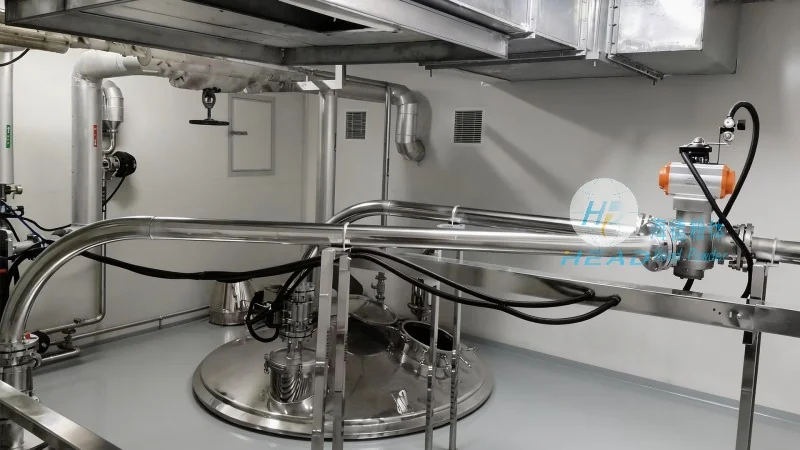
Modern heavy powder material conveying systems are equipped with advanced control and monitoring systems to ensure safe and reliable operation. These systems typically include sensors and control panels that monitor key parameters such as pressure, flow rate, and temperature. The control system can automatically adjust the feeder speed or conveyor speed to maintain a consistent material flow, preventing overloading or underloading of the system. This not only improves operational efficiency but also reduces the risk of equipment damage or material spillage. Additionally, the monitoring system can provide real-time data on the system's performance, allowing operators to identify and address any issues promptly.
Heavy powder material conveying systems are widely used in various industries due to their ability to handle large volumes of powders efficiently. In the mining industry, these systems are used to transport ore from the mine to processing facilities. In the chemical industry, they are used to move raw materials and finished products between processing units. The food and pharmaceutical industries also rely on these systems to handle powders such as flour, sugar, or active pharmaceutical ingredients (APIs). The ability to transport these materials safely and hygienically is crucial in these industries, and the design of the conveying system plays a significant role in meeting these requirements.
Heavy powder material conveying systems are essential equipment in many industrial applications, designed to handle bulk powders efficiently and reliably. The design principles of these systems focus on minimizing material degradation, ensuring energy efficiency, and providing advanced control and monitoring capabilities. By understanding the components and design of such systems, industries can optimize their material handling processes, reduce costs, and improve overall operational efficiency. As technology continues to advance, we can expect to see further improvements in the design and performance of heavy powder conveying systems, making them even more effective in meeting the demands of modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top