Understanding purified ash material conveying is crucial for industries dealing with the handling and transportation of ash byproducts. This process involves the efficient and safe movement of ash materials, often from power plants or industrial facilities, to disposal or reutilization sites. The design principles behind such systems are critical to ensuring optimal performance, minimal environmental impact, and operational reliability.
Purified ash material conveying refers to the specialized technology used to transport ash, which is a byproduct of combustion processes, through various systems. These systems are designed to handle the unique properties of ash, such as its abrasive nature, potential moisture content, and varying particle sizes. The goal is to ensure that the ash is moved efficiently while minimizing wear on equipment and controlling dust emissions. This process is integral to the overall waste management strategies of many industrial operations.
The design of purified ash material conveying systems is guided by several key principles that address the challenges of ash handling. First, the system must be robust enough to withstand the abrasive and corrosive effects of ash particles. This often involves the use of high-quality materials for components like hoppers, conveyor belts, and piping to ensure longevity and reduce maintenance costs. Second, the system needs to be designed for efficient material flow, which may include features like inclined conveyors, pneumatic systems, or mechanical conveyors, depending on the specific application and ash characteristics.
Third, environmental considerations are paramount. The design must incorporate dust control measures, such as sealing systems, filtration, or wetting mechanisms, to prevent airborne particulate matter from contaminating the environment. This is not only a regulatory requirement but also a measure to protect the health and safety of personnel working with the ash. Additionally, the system should be designed for easy maintenance and cleaning to prevent the buildup of ash residues that could lead to blockages or further contamination.
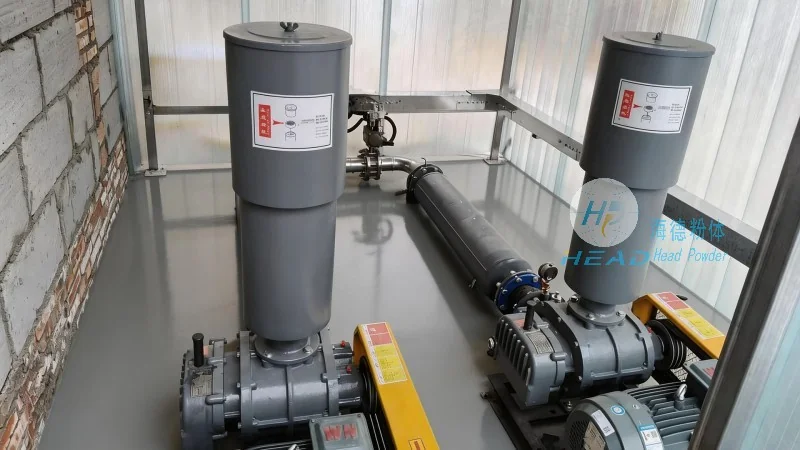
Several components and technologies are commonly employed in purified ash material conveying systems. One of the most common is the mechanical conveyor, which can include belt conveyors, screw conveyors, or bucket elevators. These systems are effective for transporting dry ash over short to medium distances. For longer distances or when dealing with finer ash particles, pneumatic conveying systems may be used. These systems use air pressure to move ash through pipes, which can be more flexible in terms of layout but may require higher energy input.
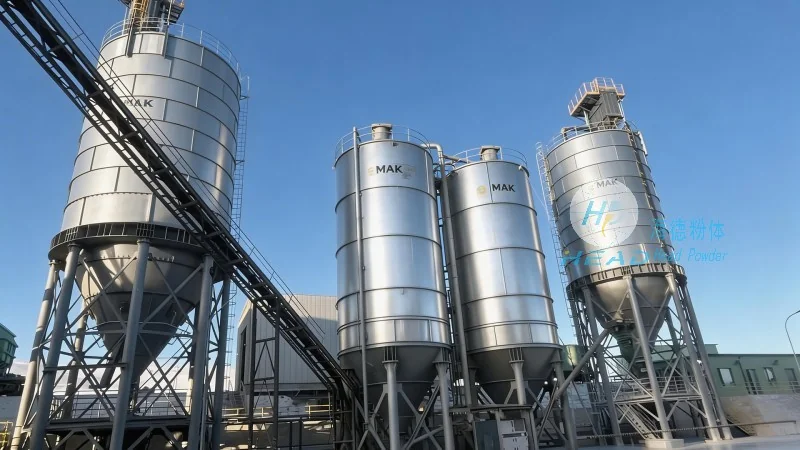
Another important component is the ash hopper or storage silo, which serves as the collection point for ash before it is conveyed. These structures are typically designed to be airtight and equipped with level sensors to monitor the material volume. The design of these hoppers often includes features to prevent dust emissions, such as sealing lids or dust collection systems. Additionally, the use of wear-resistant coatings or linings on the interior surfaces of hoppers and pipes is essential to extend the service life of the equipment.
Operational considerations play a significant role in the effectiveness of purified ash material conveying systems. Regular maintenance is crucial to ensure that the system operates efficiently and safely. This includes inspecting conveyor belts for wear, checking for blockages in pipes, and ensuring that dust control systems are functioning properly. The frequency of maintenance may vary depending on the type of ash being handled and the system's usage, but proactive maintenance is always recommended to avoid unexpected failures.
Furthermore, the system's design should allow for easy access to critical components for inspection and repair. This may involve removable panels or access ports that enable technicians to check for wear, clean surfaces, or replace parts without extensive disassembly. The use of monitoring systems, such as temperature sensors or vibration detectors, can also help in early detection of potential issues, allowing for timely intervention and reducing downtime.
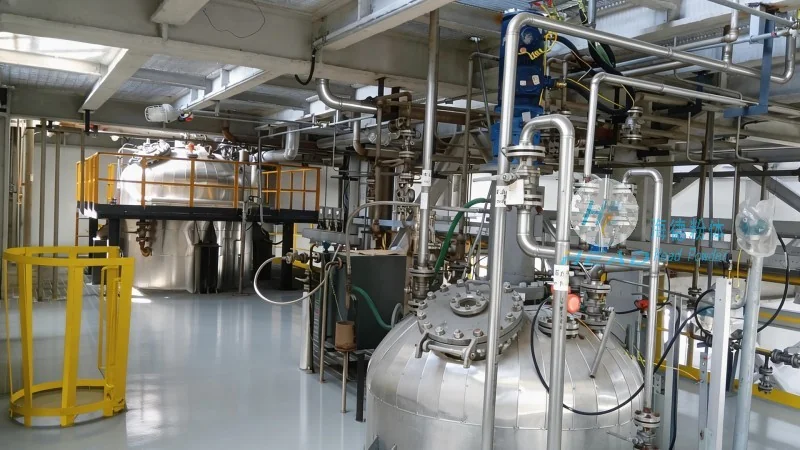
Environmental and safety aspects are integral to the design and operation of purified ash material conveying systems. The systems must comply with local and national regulations regarding air quality and waste management. Dust control measures, as mentioned earlier, are essential to minimize the release of particulate matter into the atmosphere. This may include the use of wet scrubbers, baghouse filters, or electrostatic precipitators, depending on the scale of the operation and the required emission standards.
Personnel safety is another critical consideration. The design of the system should include safety features such as emergency stop buttons, interlocked access panels, and warning signs to prevent accidents. Additionally, the system should be designed to prevent the release of ash into the environment in case of a failure, such as a conveyor belt breakage or a pipe rupture. This may involve secondary containment systems or backup mechanisms to ensure that any spillage is contained and managed appropriately.
Purified ash material conveying is a vital process in the management of ash byproducts from industrial and power generation facilities. The design principles behind these systems focus on efficiency, durability, environmental protection, and safety. By incorporating robust materials, efficient flow designs, and effective dust control measures, these systems can effectively transport ash while minimizing the impact on the environment and ensuring the safety of personnel. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd., based in China, plays a crucial role in developing and implementing such systems, providing tailored solutions to meet the specific needs of various industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top