For those in the cement industry, understanding the machinery used to transport raw materials is crucial for efficient production. One key piece of equipment is the cement raw material powder conveying system, which plays a vital role in moving bulk materials from storage to processing units. This article explores what these systems are and the underlying design principles that make them effective.
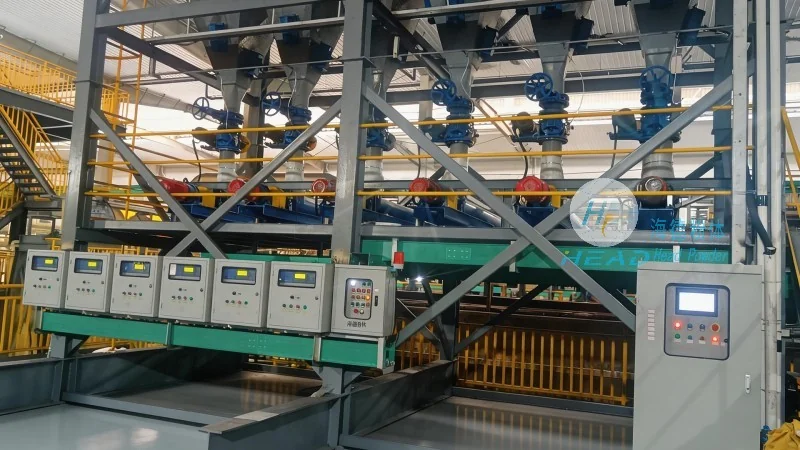
Cement raw material powder conveying equipment, often referred to as bulk material handling systems, is designed to transport dry powders and granular materials used in cement production. These materials, such as limestone, clay, and iron ore, are typically stored in silos or stockpiles before being conveyed to the cement kiln or other processing stages. The primary goal of this equipment is to ensure a continuous, reliable flow of raw materials, minimizing downtime and optimizing production efficiency.
The cement raw material powder conveying system typically consists of several key components that work together to achieve efficient material transport. These components include:
The design of cement raw material powder conveying equipment is based on several key principles to ensure reliability, efficiency, and safety. These principles include:
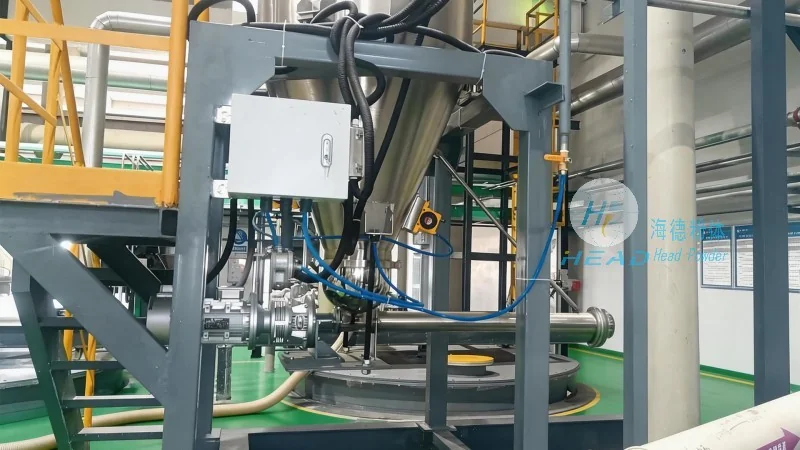
1. Material Compatibility: The equipment must be designed to handle the specific properties of the raw materials, such as particle size, moisture content, and abrasiveness. For example, materials with high abrasiveness may require special wear-resistant components to extend the equipment's lifespan.
2. Flow Control: Precise control of the material flow is essential to prevent blockages or overloading. This is achieved through the use of feeders, rotary valves, and control systems that adjust the flow rate based on real-time conditions.
3. Energy Efficiency: Modern conveying systems are designed to minimize energy consumption. This includes using efficient motors, optimizing air pressure, and reducing friction in the pipeline. Energy efficiency not only reduces operational costs but also aligns with sustainability goals in the cement industry.
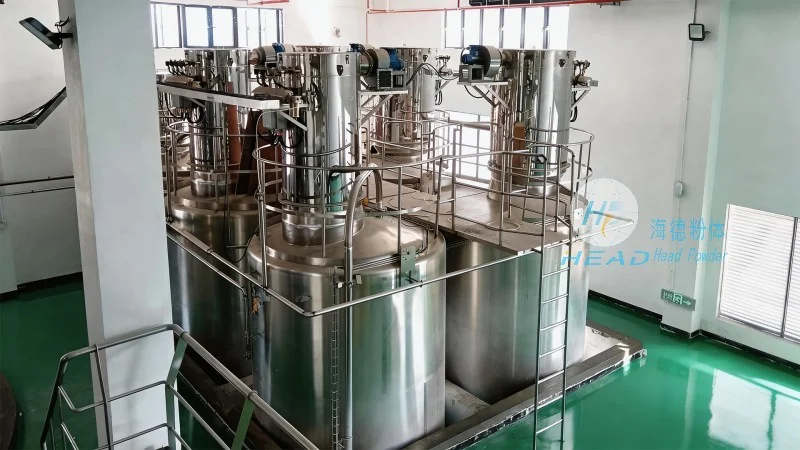
4. Safety and Reliability: The design incorporates safety features to prevent accidents and ensure continuous operation. This includes emergency stop mechanisms, pressure relief valves, and regular maintenance schedules. Reliability is critical in cement production, as downtime can lead to significant financial losses.
Cement raw material powder conveying equipment is a critical component in the cement manufacturing process. The equipment ensures that raw materials are delivered to the cement kiln at the correct rate and consistency, which directly impacts the quality of the final cement product. By maintaining a steady flow of raw materials, the system helps to optimize the kiln's operation, reduce fuel consumption, and improve overall production efficiency.
Cement raw material powder conveying equipment is a sophisticated system that combines mechanical, pneumatic, and control technologies to efficiently transport bulk materials in the cement industry. The design principles, including material compatibility, flow control, energy efficiency, and safety, are crucial for ensuring the equipment operates reliably and effectively. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in designing and manufacturing high-quality conveying systems that meet the specific needs of cement producers, helping them achieve optimal performance and efficiency in their operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top