Activated carbon powder handling equipment is a specialized system designed to transport, store, and manage activated carbon powder efficiently. This equipment is crucial in various industrial applications, including water treatment, air purification, and chemical processing, where activated carbon's adsorption properties are leveraged to remove impurities and contaminants. The design of such equipment must address the unique challenges posed by activated carbon powder, such as its fine particle size, low bulk density, and tendency to create dust and caking. Understanding the design principles behind these systems is essential for optimizing performance, ensuring safety, and maintaining product quality.
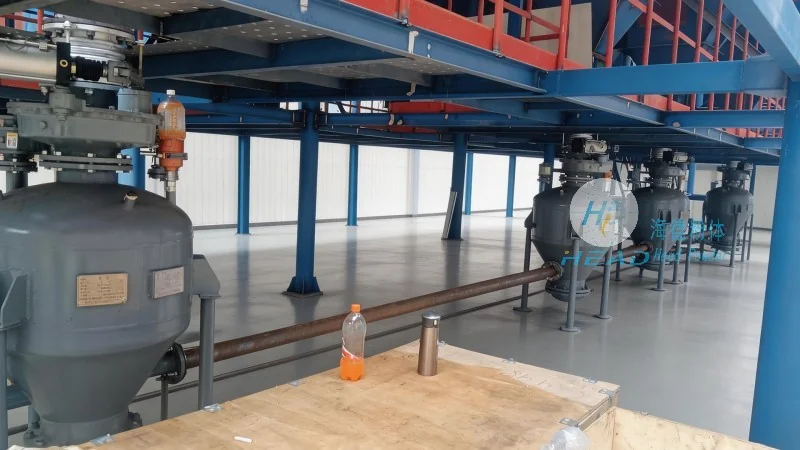
Shandong HeadPowder Engineering Co., Ltd. is a prominent manufacturer and supplier of activated carbon powder handling equipment. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for industries requiring reliable and efficient powder handling solutions. The company's expertise lies in designing equipment that meets the specific needs of clients, ensuring optimal performance and durability. HeadPowder's products are engineered to handle the unique characteristics of activated carbon powder, including its fine particle size and low bulk density, while maintaining high levels of safety and efficiency. The company's focus on customer satisfaction and technical excellence has made it a preferred choice for businesses operating in water treatment, air purification, and related industries.
The design of activated carbon powder handling equipment is guided by several critical principles to ensure effective and safe operation. One of the primary considerations is the prevention of dust generation and caking, which can lead to blockages and equipment failure. To address this, equipment often incorporates features such as dust collection systems, anti-caking agents, and specialized hopper designs. Another key principle is the optimization of material flow, which involves using appropriate conveyor systems, such as screw conveyors, pneumatic conveyors, or bucket elevators, to ensure smooth and consistent movement of the powder. The selection of materials for construction is also crucial, as activated carbon can be corrosive or abrasive in certain applications. Therefore, equipment is typically made from high-quality, corrosion-resistant materials like stainless steel or special alloys to withstand the harsh conditions. Additionally, the design must prioritize safety, including proper ventilation, explosion-proof features, and emergency shutdown systems to protect operators and the environment.
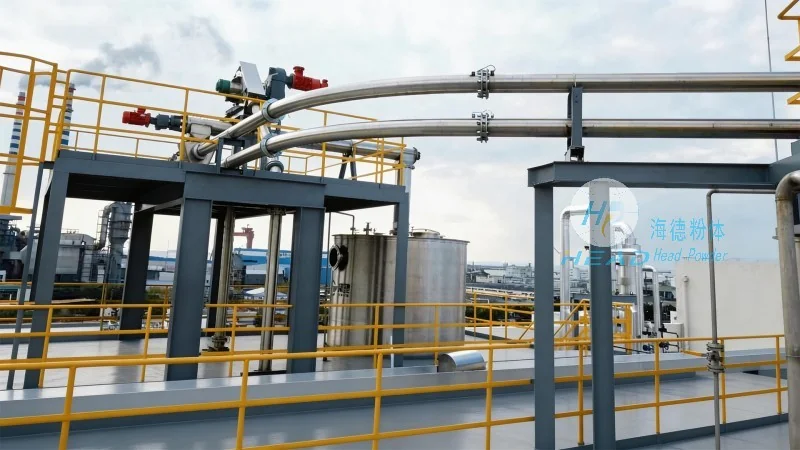
Activated carbon powder handling systems typically consist of several key components, each playing a vital role in the overall operation. The primary components include feeders, hoppers, conveyors, and storage silos. Feeders are used to control the flow of activated carbon powder from the storage hopper to the conveyor system, ensuring a consistent and controlled discharge rate. Hoppers are designed to store the powder and provide a stable feed to the feeder, often incorporating features like anti-caking mechanisms to prevent blockages. Conveyors, such as screw conveyors or pneumatic systems, transport the powder from the storage area to the processing equipment or discharge point. These conveyors are engineered to handle the fine particle size and low bulk density of activated carbon, minimizing the risk of clogging and ensuring efficient transport. Storage silos are used to store large quantities of activated carbon powder, providing a reliable source of material for continuous operation. The design of these silos often includes features like agitators or vibrators to prevent caking and maintain the flowability of the powder. Each component is carefully selected and integrated to create a cohesive system that meets the specific requirements of the application.
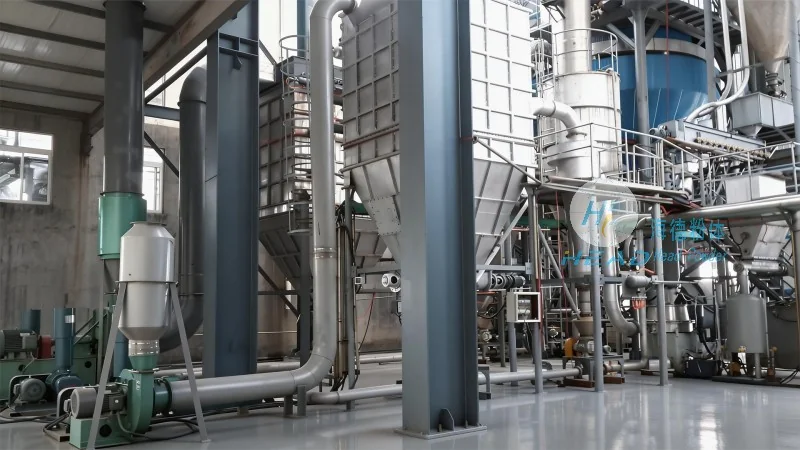
Activated carbon powder handling equipment is widely used in various industrial applications where activated carbon's adsorption properties are essential. In water treatment facilities, these systems are used to transport activated carbon to filters and reactors, ensuring efficient removal of organic contaminants and impurities. In air purification systems, the equipment handles activated carbon for activated carbon filters, which are used to remove volatile organic compounds (VOCs) and other air pollutants. The equipment also plays a crucial role in chemical processing industries, where activated carbon is used for adsorption and separation processes. The benefits of using specialized handling equipment include improved efficiency, reduced downtime, and enhanced safety. By preventing dust and caking, the equipment ensures consistent performance and prolongs the lifespan of the activated carbon. Additionally, the optimized design of the system minimizes material loss and waste, contributing to cost savings and environmental sustainability. The use of reliable handling equipment also ensures that the activated carbon remains in its optimal condition, maximizing its adsorption capacity and effectiveness.
Activated carbon powder handling equipment is a critical component in industries that rely on activated carbon for purification and adsorption processes. The design principles and components of these systems are carefully engineered to address the unique challenges posed by activated carbon powder, ensuring efficient, safe, and reliable operation. Shandong HeadPowder Engineering Co., Ltd. has demonstrated expertise in designing and manufacturing such equipment, providing industries with reliable solutions that meet their specific needs. By adhering to the key design principles and utilizing appropriate components, businesses can optimize their activated carbon handling processes, improve performance, and enhance overall operational efficiency. The proper design and implementation of activated carbon powder handling equipment are essential for maintaining product quality, ensuring safety, and achieving long-term success in industries that rely on activated carbon's unique properties.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top