Wheat flour pneumatic conveying systems are essential equipment in the food processing industry, particularly for handling and transporting wheat flour efficiently and hygienically. These systems use air to move flour from one location to another, offering advantages such as reduced contamination risk, improved process control, and enhanced safety compared to traditional mechanical conveying methods.
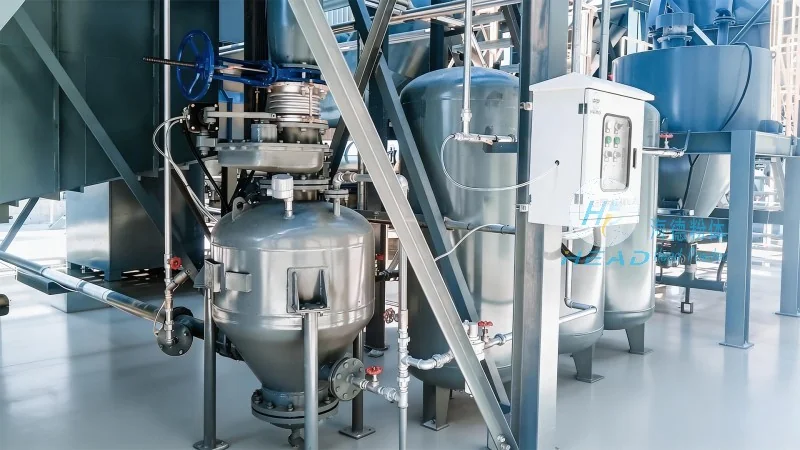
A pneumatic conveying system for wheat flour typically consists of several key components, including a hopper, a conveyor line, a filter, and a dust collection system. The process begins with the flour being fed into the hopper, where it is then drawn into the conveyor line by a vacuum or pressure source. The air, along with the flour particles, travels through the pipeline to the destination point, such as a silo or processing unit. The system is designed to maintain a consistent flow rate and prevent clogging, which is crucial for maintaining product quality and operational efficiency.
The design of a wheat flour pneumatic conveying system involves several critical principles to ensure optimal performance. First, the system must be constructed from materials that are non-corrosive and easy to clean, such as stainless steel, to meet hygiene standards required in food processing. Second, the air velocity within the pipeline must be carefully controlled to prevent flour particles from settling or clogging the system. This is typically achieved by using a combination of vacuum and pressure stages, with the velocity maintained at a level that ensures the flour remains in suspension without causing excessive wear on the equipment. Third, the system includes a filter and dust collection system to capture any flour particles that may escape the pipeline, ensuring that the air is clean and the environment remains safe for operators. Additionally, the system is designed to minimize pressure drops, which helps maintain consistent flow rates and reduces energy consumption.
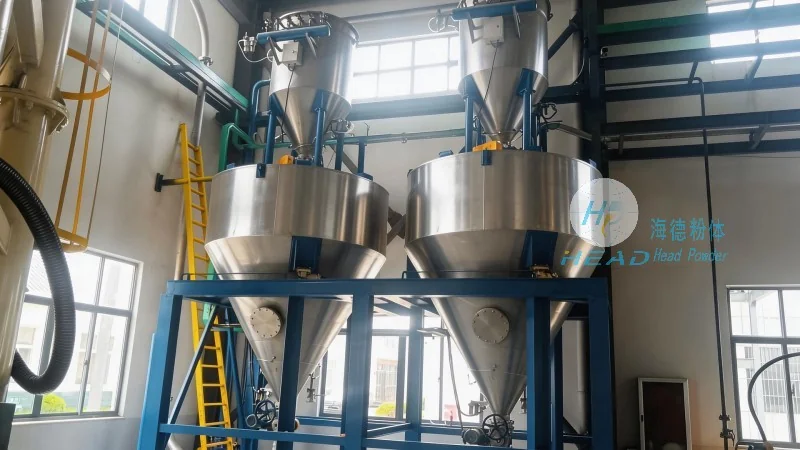
Each component of a wheat flour pneumatic conveying system plays a vital role in its overall performance. The hopper serves as the storage and feeding unit, providing a consistent supply of flour to the system. The conveyor line, which can be either a vacuum or pressure system, is responsible for transporting the flour through the pipeline. The filter and dust collection system are essential for maintaining air quality and preventing flour dust from entering the environment. The system also includes control valves and sensors to monitor and adjust the flow rate and pressure, ensuring that the system operates within optimal parameters.
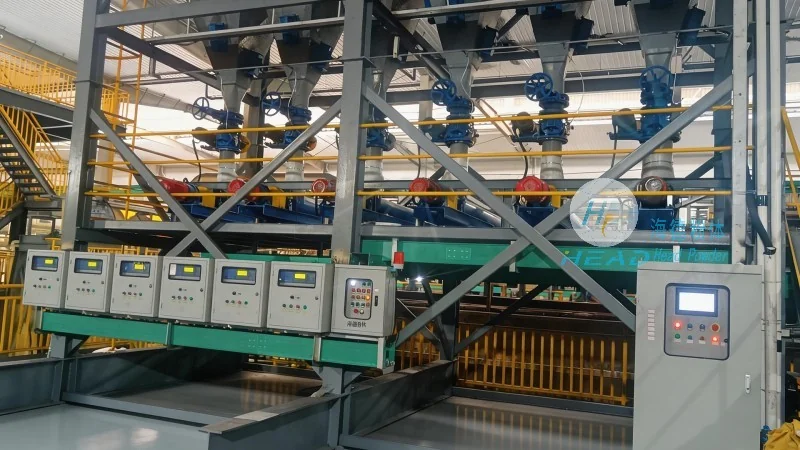
Wheat flour pneumatic conveying systems offer several benefits over traditional mechanical conveying methods. One of the primary advantages is the reduced risk of contamination, as the flour is enclosed within the pipeline and not exposed to the environment. This is particularly important in food processing, where product safety is a top priority. Additionally, the systems are more hygienic and easier to clean, as they are constructed from materials that are non-porous and can be easily sanitized. The systems also offer improved process control, allowing operators to adjust the flow rate and pressure as needed to meet production requirements. Finally, the systems are more energy-efficient than traditional methods, as they use less power to transport the flour over long distances.
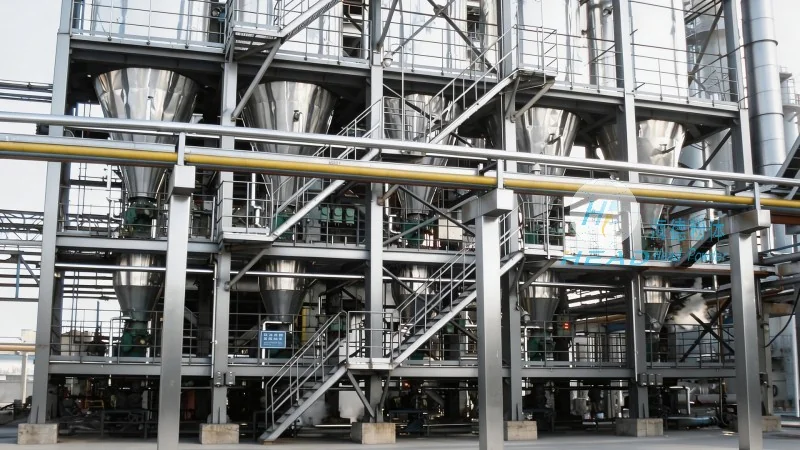
Wheat flour pneumatic conveying systems are widely used in various applications within the food processing industry. They are commonly used in flour mills to transport flour from the grinding process to storage silos, as well as in bakeries and food processing plants to move flour to production lines. The systems are also used in the packaging industry to transport flour into packaging machines, ensuring a consistent and hygienic supply of product. In addition, the systems are used in the pharmaceutical and chemical industries for transporting fine powders, where similar principles apply.
Wheat flour pneumatic conveying systems are a critical component of modern food processing operations, providing efficient, hygienic, and safe methods for transporting wheat flour. The design principles and components of these systems are carefully engineered to meet the specific needs of the food industry, ensuring that the flour is handled and transported in a manner that maintains its quality and safety. As the food processing industry continues to evolve, these systems will remain a vital part of the production process, helping to ensure that high-quality wheat flour is produced and delivered to consumers.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top