When it comes to efficient and clean material handling in industrial settings, the dust-free material feeding pneumatic conveying system stands out as a critical solution. This technology is designed to transport bulk materials with minimal dust generation, ensuring a safe and hygienic working environment. Understanding its functionality and design principles is essential for industries that prioritize precision, cleanliness, and operational efficiency.
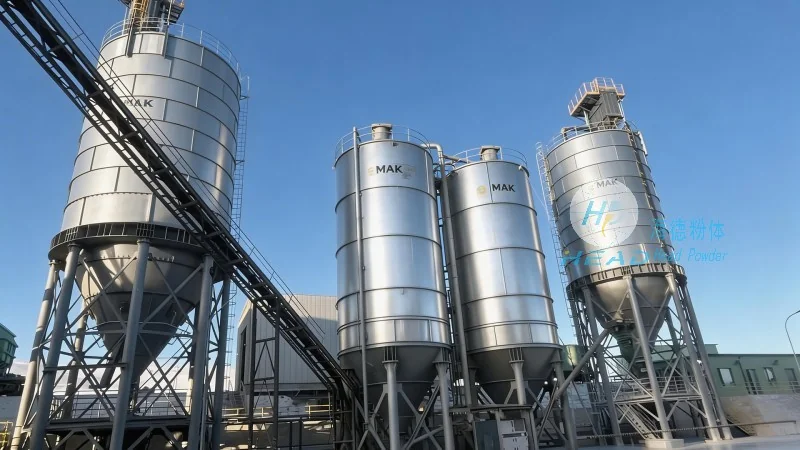
A dust-free material feeding pneumatic conveying system is a specialized equipment used to transport dry bulk materials from one location to another within a facility. Unlike traditional methods that may involve manual handling or open-air conveyors, this system operates by using compressed air to move materials through a sealed pipeline. The key feature is its ability to minimize dust release, making it ideal for applications where contamination control is paramount, such as in pharmaceutical, food processing, and high-purity manufacturing industries.
HeadPowder, a leading name in the field, is dedicated to delivering high-quality dust-free material feeding pneumatic conveying systems. As a professional manufacturer based in Shandong, China, HeadPowder has established itself as a reliable partner for businesses seeking advanced material handling solutions. With years of experience and a commitment to innovation, the company focuses on providing systems that meet stringent industry standards while ensuring durability and performance.
The design of a dust-free material feeding pneumatic conveying system revolves around several core principles aimed at achieving optimal performance and minimal dust generation. The first principle is the use of sealed and airtight pipelines, which prevent material leakage and dust escape. This is achieved through robust construction materials, such as stainless steel or specialized polymers, that can withstand the pressures and abrasion of bulk materials.
Another critical design principle is the incorporation of efficient air distribution and flow control mechanisms. The system uses a combination of blowers or compressors to generate the necessary air pressure, which propels the material through the pipeline. Variable speed drives and pressure regulators are often employed to maintain consistent flow rates, ensuring smooth and continuous material transport. This not only enhances the conveying efficiency but also reduces energy consumption.
Furthermore, the system incorporates advanced filtration and separation components. These include cyclone separators, bag filters, or electrostatic precipitators that capture any fine particles that may escape during the conveying process. The collected dust is then safely disposed of or recycled, maintaining the overall cleanliness of the system and the surrounding environment. This design ensures compliance with environmental regulations and industry hygiene standards.
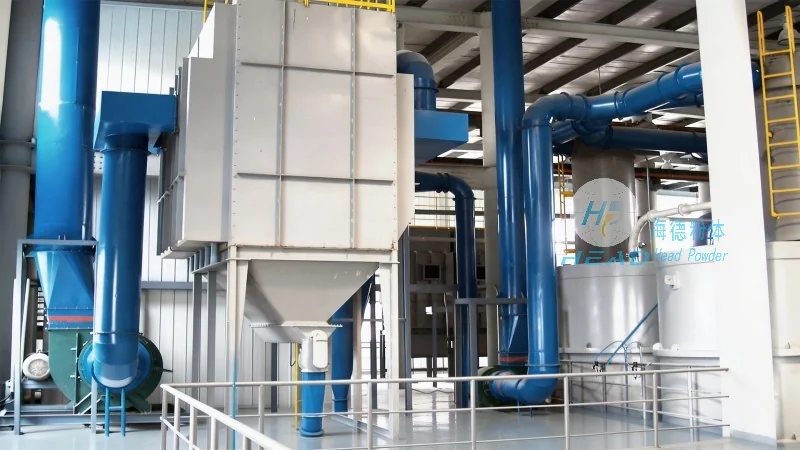
The operation of a dust-free material feeding pneumatic conveying system involves several key steps that work in harmony to achieve effective material transport. First, the bulk material is fed into the system's hopper or feeder, where it is prepared for transport. The feeder may include a rotary valve or a screw conveyor to regulate the flow of material into the pipeline.
Next, compressed air is introduced into the system, creating a pressure differential that propels the material forward. The air and material mixture travels through the sealed pipeline, with the air providing the necessary force to move the material. As the mixture moves, it passes through the filtration and separation components, where any dust or fine particles are removed.
The material then reaches the discharge point, where it is collected in a receiving hopper or container. The air, now filtered and free of dust, is typically vented to the atmosphere or recycled back into the system, depending on the design. This closed-loop operation minimizes waste and ensures that the system operates efficiently and sustainably.
Adopting a dust-free material feeding pneumatic conveying system offers numerous advantages for industrial operations. Firstly, it significantly reduces dust exposure, improving workplace safety and compliance with occupational health regulations. This is particularly important in industries where inhalation of fine particles can lead to health risks.
Secondly, the system enhances operational efficiency by providing a continuous and reliable method of material transport. Unlike manual or mechanical conveyors that may require frequent maintenance or adjustments, pneumatic systems can operate 24/7 with minimal downtime. This leads to increased productivity and reduced labor costs.
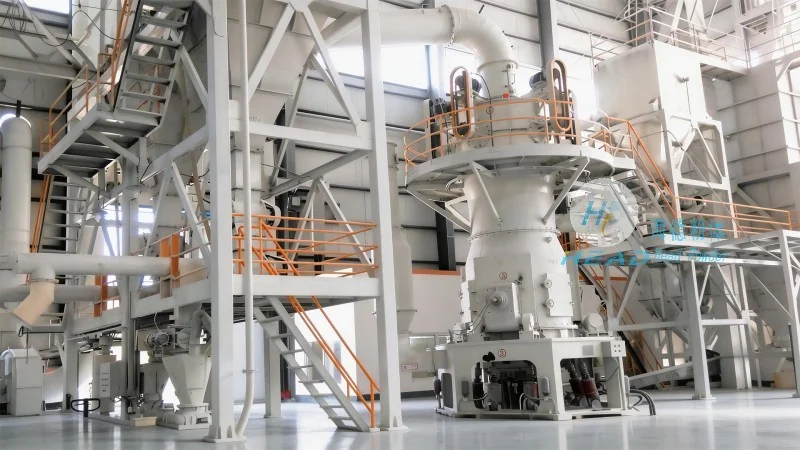
Thirdly, the sealed design of the system prevents material contamination, which is crucial in sectors like pharmaceuticals and food processing where product purity is non-negotiable. The absence of dust also reduces the risk of product degradation or clogging in downstream equipment, ensuring consistent quality throughout the production process.
Additionally, the energy efficiency of modern pneumatic conveying systems makes them a cost-effective solution in the long run. By optimizing air flow and using energy-saving components, businesses can reduce their operational costs while maintaining high performance levels.
HeadPowder understands that each industrial application has unique requirements. Therefore, the company offers customized dust-free material feeding pneumatic conveying systems tailored to specific needs. Whether it's handling fine powders, granules, or bulk solids, the system can be designed to accommodate different material characteristics and flow rates.
The flexibility extends to system size and configuration. From small-scale laboratory systems to large industrial installations, HeadPowder can provide solutions that fit the space and budget constraints of the client. The company works closely with customers to assess their material handling challenges and develop a system that meets their exact specifications.
In conclusion, a dust-free material feeding pneumatic conveying system is a vital technology for industries that demand clean, efficient, and safe material handling. By understanding its design principles and benefits, businesses can make informed decisions when selecting a system. HeadPowder, with its expertise and commitment to quality, is a trusted partner in providing these advanced solutions. Whether you are in the pharmaceutical, food, or chemical industry, investing in a reliable dust-free pneumatic conveying system from HeadPowder can enhance your operational efficiency, ensure workplace safety, and maintain product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top