Sulfur, a vital industrial material utilized in sectors like chemical manufacturing, rubber production, and pharmaceuticals, demands efficient and reliable handling methods. Traditional approaches such as manual handling or mechanical conveyors often encounter challenges in preserving product quality and operational efficiency. This is where sulfur pneumatic conveying systems emerge as a modern solution, enabling precise and low-risk transportation of sulfur while minimizing contamination or degradation. Grasping the fundamentals of these systems and their design principles is crucial for industries dependent on consistent sulfur supply and processing.
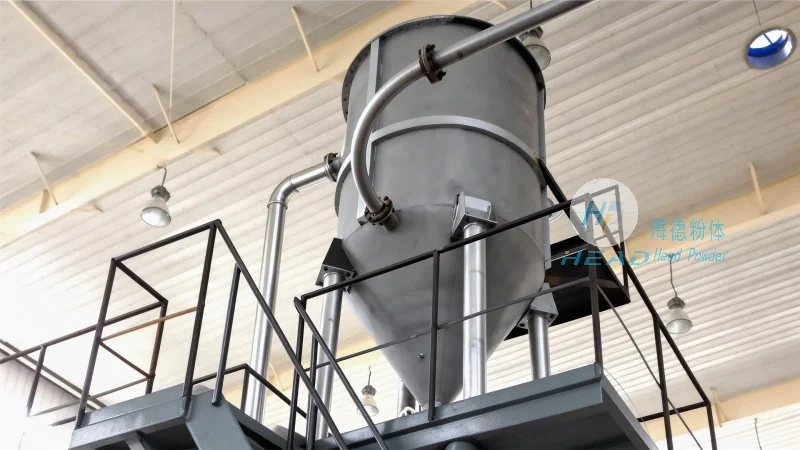
HeadPowder, a leading manufacturer headquartered in Shandong, China, specializes in developing advanced pneumatic conveying equipment tailored to the unique requirements of sulfur and other bulk materials. With years of industry experience, HeadPowder has established itself as a trusted partner for companies seeking high-performance, durable, and cost-effective conveying solutions. The company’s dedication to quality, innovation, and customer satisfaction drives its mission to deliver systems that meet the most demanding operational needs. Located in Shandong, China, HeadPowder leverages local expertise and resources to provide comprehensive support, from system design and manufacturing to installation and after-sales service.
The design of a sulfur pneumatic conveying system is grounded in the fundamental principles of pneumatic transport, which involves moving bulk materials through a pipeline using air or other gases. For sulfur, typically in powder or granular form, the system must account for its physical properties, including particle size, density, and flow characteristics. The key components of a typical sulfur pneumatic conveying system include the material hopper, feed mechanism, air compressor, conveying line, and discharge equipment. Each component plays a critical role in ensuring the system operates efficiently and safely.
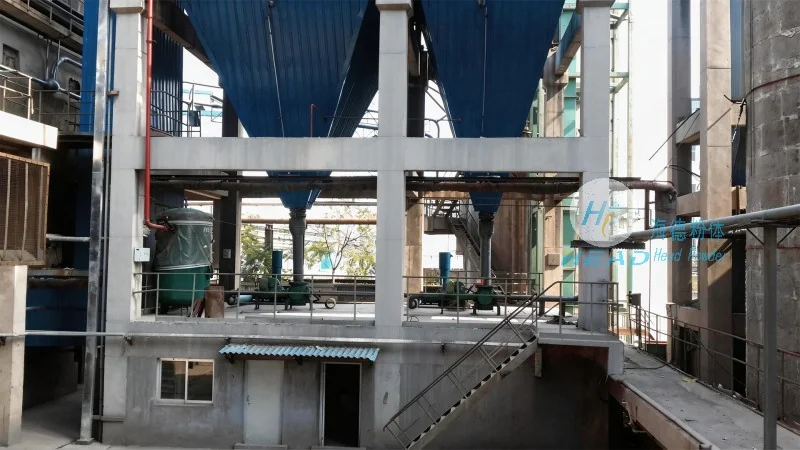
First, the material hopper is designed to store and feed sulfur into the system. It typically features a hopper with a conical bottom to facilitate uniform material flow. The feed mechanism, often a rotary valve or a star feeder, controls the rate of sulfur discharge into the conveying line. This ensures a consistent flow rate, preventing overloading or underloading of the system. Next, the air compressor generates the necessary pressure to move sulfur particles through the pipeline. The choice of compressor type (e.g., positive displacement or centrifugal) depends on the system’s capacity and the required pressure. The conveying line, usually made of stainless steel or other corrosion-resistant materials, is designed to withstand sulfur’s chemical properties and maintain airtight integrity to prevent leakage.
Another critical aspect of the design is the air-to-material ratio, which determines the efficiency of the conveying process. The ratio is calculated based on the material’s density, particle size, and the desired conveying velocity. A higher air-to-material ratio can increase the conveying speed but may also lead to higher energy consumption. Conversely, a lower ratio may reduce energy use but could result in slower transport or even system blockages. Engineers at HeadPowder carefully optimize this ratio to balance efficiency and cost, ensuring the system operates at its peak performance. Additionally, the system incorporates features such as pressure relief valves and filters to maintain system safety and prevent dust accumulation, which is crucial for handling sulfur—a material that can be both abrasive and potentially hazardous if not managed properly.
Sulfur pneumatic conveying systems offer several advantages over traditional conveying methods. One primary benefit is the ability to transport sulfur in a closed system, minimizing exposure to environmental factors and reducing the risk of contamination. This is particularly important for sulfur, which can be sensitive to moisture or other impurities. The closed system also helps maintain product quality by preventing dust dispersion and protecting the material from external contaminants. Another advantage is the flexibility of the system, which can be easily adjusted to handle varying sulfur feed rates or different particle sizes. This adaptability makes the system suitable for a wide range of industrial applications, from small-scale processing to large-scale production.
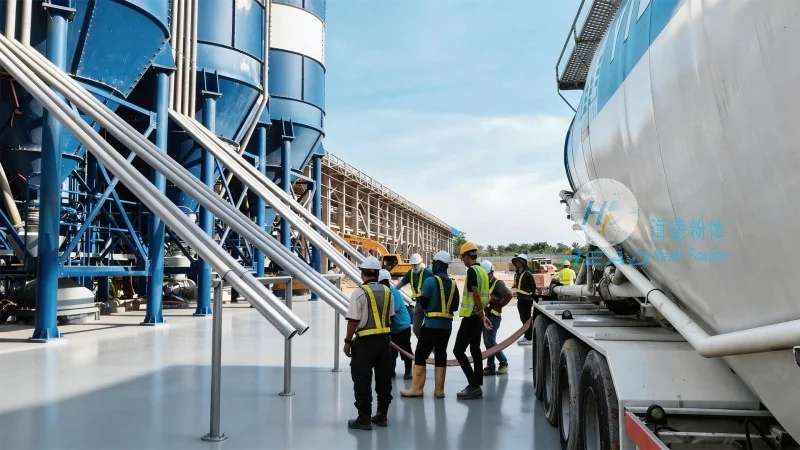
Furthermore, pneumatic conveying systems are generally more energy-efficient compared to mechanical conveyors, especially for long-distance transport. The use of compressed air allows for the movement of sulfur over considerable distances without the need for complex mechanical components like belts or chains. This not only reduces maintenance costs but also enhances the overall reliability of the system. Additionally, the system’s design allows for easy integration with other processing equipment, such as reactors or mixers, enabling seamless workflow in sulfur processing plants. HeadPowder’s systems are engineered with these advantages in mind, ensuring customers receive a solution that is both effective and sustainable.
As industries continue to rely on sulfur for their operations, the importance of efficient and reliable conveying systems cannot be overstated. Sulfur pneumatic conveying systems, with their advanced design principles and robust construction, provide a superior solution for handling this critical material. HeadPowder, with its expertise and commitment to quality, offers customized pneumatic conveying systems that meet the specific needs of sulfur processing facilities. By leveraging the company’s experience and innovative approach, businesses can enhance their operational efficiency, reduce costs, and ensure the consistent quality of their sulfur products. For more information about sulfur pneumatic conveying systems or to learn how HeadPowder can assist with your conveying needs, please contact us at our Shandong location.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top