A powder electrolyte pneumatic conveying system is a specialized industrial equipment designed to transport fine powders, such as electrolytes, through a pipeline using air or other gas as the conveying medium. This system is widely used in various industries, including chemical, pharmaceutical, and food processing, where the safe and efficient handling of powders is critical. The system typically consists of a hopper, a blower or compressor, a pipeline network, and a discharge device, all working together to move the powder from the source to the destination.
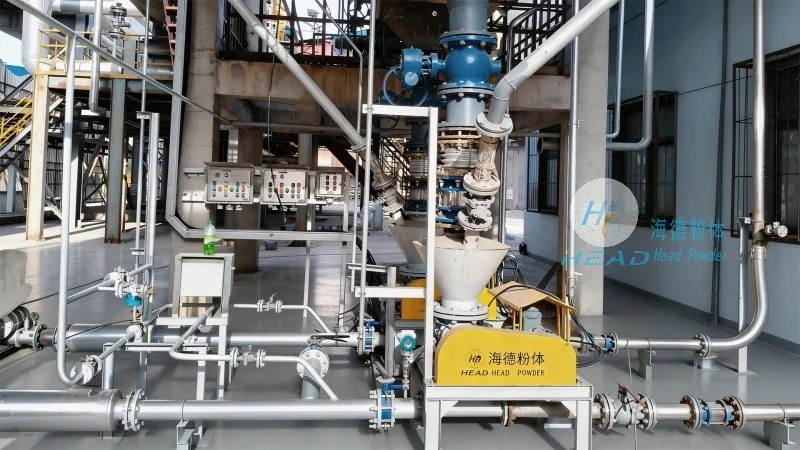
HeadPowder, a leading manufacturer in the field, specializes in the design, development, and production of advanced pneumatic conveying systems. With a strong presence in Shandong, China, the company has built a reputation for delivering high-quality, reliable solutions tailored to the unique needs of its clients. The company's full name is Shandong HeadPowder Engineering Co., Ltd., and its operational base is located in Shandong, providing a solid foundation for its engineering and manufacturing capabilities.
The design of a powder electrolyte pneumatic conveying system is based on several key principles that ensure efficient and safe operation. The primary principle is the use of differential pressure to move the powder through the pipeline. The system operates by creating a pressure difference between the inlet and outlet of the pipeline, which propels the powder particles forward. This is achieved through the use of a blower or compressor that generates the necessary air flow and pressure.
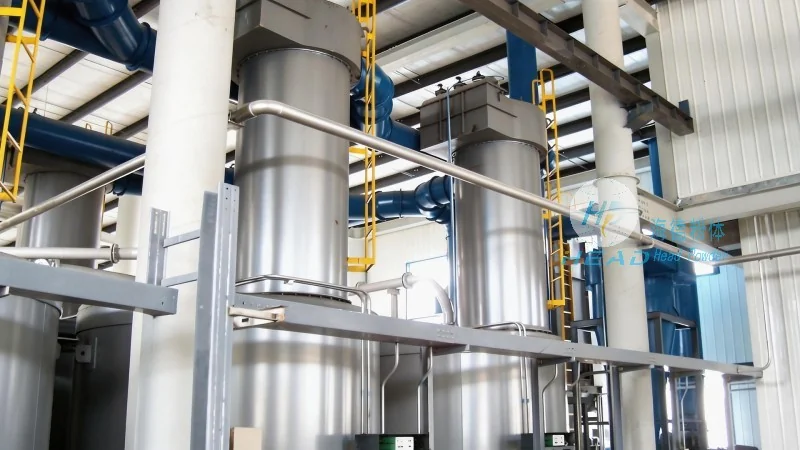
Another crucial principle is the selection of appropriate air velocity and particle size. The air velocity must be sufficient to keep the powder particles suspended in the air stream, preventing them from settling or clogging the pipeline. The particle size of the electrolyte powder is also a critical factor, as larger particles may require higher air velocities or different conveying methods to ensure smooth transport. Engineers at HeadPowder carefully consider these parameters to design a system that optimizes performance and minimizes energy consumption.
The effectiveness of a powder electrolyte pneumatic conveying system depends on the proper integration of several key components. The hopper serves as the storage and feeding unit, where the powder is loaded and then discharged into the pipeline. The blower or compressor provides the necessary air pressure and flow rate to move the powder. The pipeline network connects the hopper to the discharge point and may include bends, valves, and filters to ensure smooth and unobstructed flow. The discharge device, such as a rotary valve or a venturi, controls the release of the powder at the destination. Each component is designed and manufactured to meet the specific requirements of the electrolyte powder being conveyed, ensuring optimal performance and reliability.
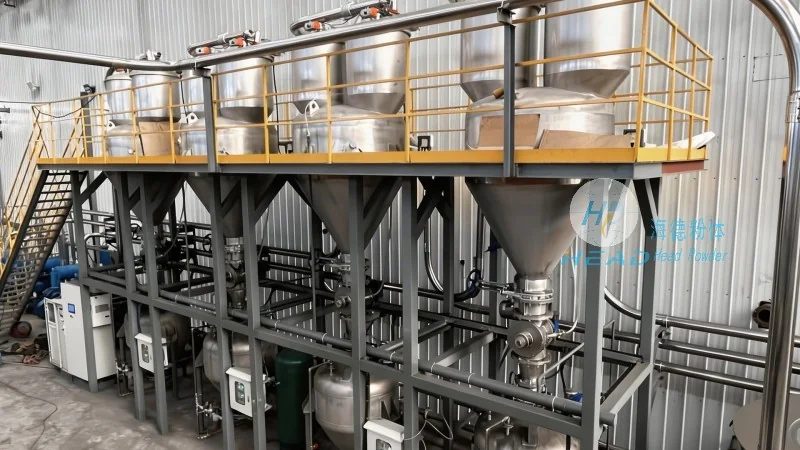
Implementing a powder electrolyte pneumatic conveying system offers several advantages over traditional methods, such as belt conveyors or manual handling. One of the main benefits is the ability to transport powders over long distances without the need for multiple transfer points, reducing the risk of contamination and material loss. The system also provides a closed-loop operation, which helps maintain the purity of the electrolyte powder and prevents dust emissions into the environment. Additionally, pneumatic conveying systems are more flexible and can be easily adapted to changes in production requirements, allowing for scalability and adaptability. HeadPowder's systems are engineered to maximize these advantages, providing clients with a cost-effective and efficient solution for their powder handling needs.
Powder electrolyte pneumatic conveying systems are widely used in various industrial applications. In the chemical industry, they are used to transport chemicals, such as lithium carbonate or sodium hydroxide, which are essential components in battery production. In the pharmaceutical industry, the system is used to handle active pharmaceutical ingredients (APIs) and excipients, ensuring that the powders are transported in a sterile and controlled environment. The food processing industry also benefits from these systems, as they are used to transport food powders, such as sugar or flour, while maintaining hygiene and preventing contamination. HeadPowder has successfully implemented these systems in numerous projects across different industries, demonstrating its expertise in providing tailored solutions for diverse applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top