HeadPowder, a prominent engineering company headquartered in Shandong, China, is dedicated to delivering high-performance pneumatic conveying solutions for the handling of powdered milk. This article delves into the core concepts of pneumatic conveying systems, outlining their working principles and practical applications in industrial settings. By understanding these systems, stakeholders in the dairy and food processing sectors can make informed decisions about equipment selection and operational strategies.
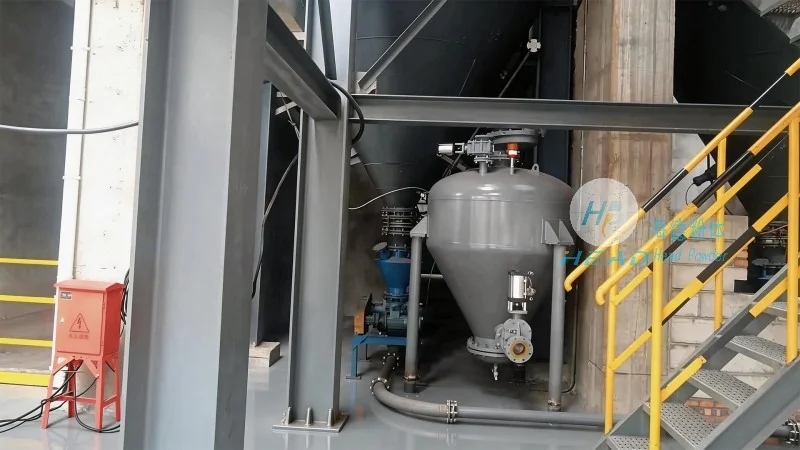
Pneumatic conveying systems utilize compressed air or gas to transport bulk materials, such as powdered milk, through a network of pipes. The process typically operates under either positive pressure (where air is forced into the system) or negative pressure (where air is drawn out, creating a vacuum). For powdered milk, positive pressure systems are commonly preferred due to their ability to maintain product integrity and prevent contamination. The system comprises several key components: a material feeder to introduce the powder into the pipeline, a blower or compressor to generate the necessary airflow, a conveying pipeline to transport the material, a separation and collection unit to discharge the product, and a filter to capture any fine particles and return clean air to the system.
Each component plays a critical role in ensuring the efficient and safe transport of powdered milk. The material feeder, often a rotary valve or a star feeder, ensures a consistent and controlled flow of the powder into the pipeline, preventing blockages and maintaining system stability. The blower or compressor provides the driving force, with pressure levels carefully calibrated to match the material's characteristics and pipeline length. The conveying pipeline, typically made of stainless steel or other corrosion-resistant materials, is designed to minimize friction and maintain product purity. The separation unit, such as a cyclone or a bag filter, separates the product from the air stream, allowing the powder to be collected in a container while the air is filtered and recirculated. This design ensures minimal product loss and maintains a clean working environment.
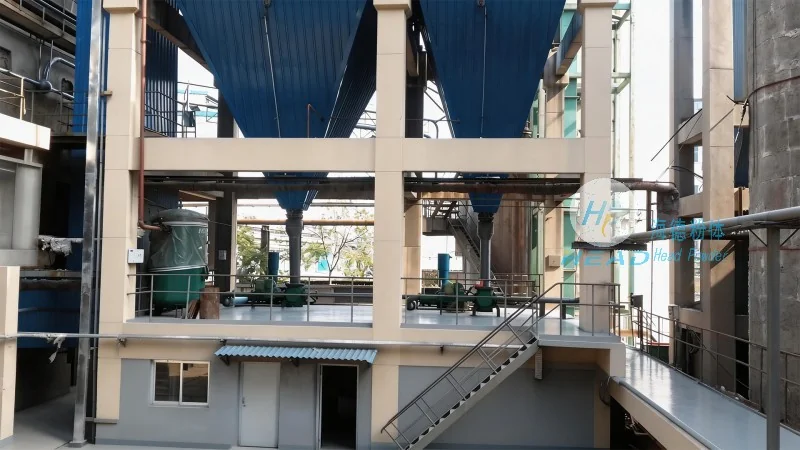
Pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. Firstly, they eliminate the need for moving parts in contact with the product, reducing the risk of contamination and mechanical wear. This is particularly important for sensitive products like powdered milk, where hygiene and product quality are paramount. Secondly, the systems are highly flexible, allowing for changes in material flow rates and pipeline configurations without significant modifications. Thirdly, they can be integrated with automated control systems, enabling remote monitoring and operation, which enhances operational efficiency and reduces labor costs. Additionally, pneumatic conveying systems are capable of handling a wide range of powder properties, including different particle sizes, densities, and moisture contents, making them versatile for various applications in the dairy industry.
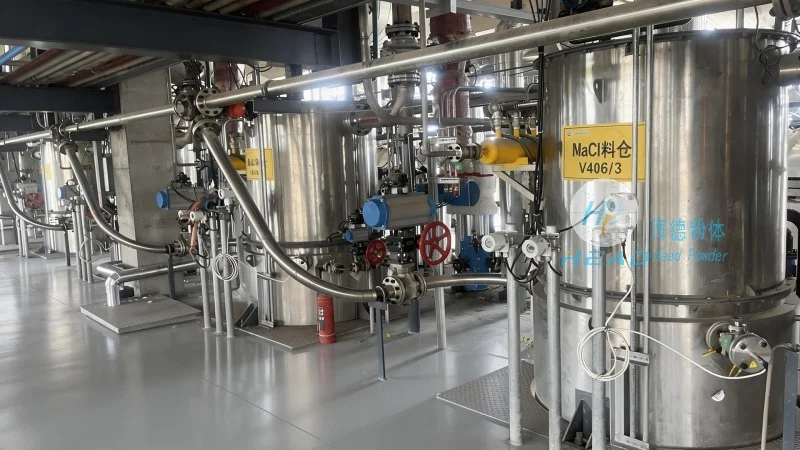
The application of pneumatic conveying systems in the dairy industry is widespread, particularly in the processing and packaging of powdered milk. For instance, in a typical milk powder production line, the system may be used to transport raw milk powder from storage silos to mixing tanks, or to move finished product from the packaging line to storage containers. In such scenarios, the system ensures a continuous and hygienic flow of material, minimizing downtime and improving overall production throughput. Furthermore, the ability to handle large volumes of powder efficiently makes pneumatic conveying an ideal solution for high-capacity dairy processing facilities.
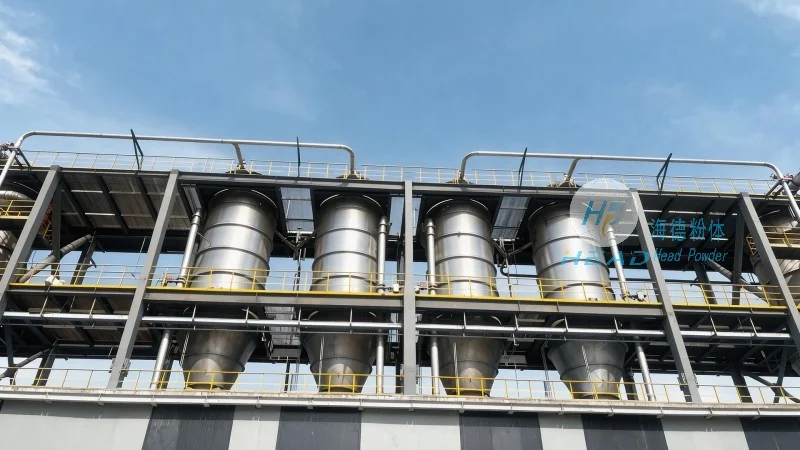
HeadPowder, with its headquarters in Shandong, China, specializes in providing customized pneumatic conveying solutions tailored to the specific needs of each client. The company's engineering team works closely with clients to assess their operational requirements, material characteristics, and facility constraints, then designs a system that optimizes performance, cost, and safety. Whether it's a new installation or an upgrade to an existing system, HeadPowder offers comprehensive services, including system design, equipment supply, installation, and commissioning. The company's expertise in material handling and process engineering ensures that the final solution meets the highest industry standards, delivering reliable and efficient operation for years to come.
Pneumatic conveying systems represent a sophisticated and effective method for handling powdered milk, offering numerous benefits over traditional conveying technologies. By leveraging the principles of air flow and material transport, these systems enhance product quality, operational efficiency, and safety in dairy processing facilities. HeadPowder, as a leading provider in this field, continues to innovate and deliver tailored solutions that meet the evolving needs of the industry, ensuring that clients can achieve optimal performance and reliability in their material handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top