Cement dust pneumatic conveying systems are critical in industrial applications for efficiently transporting fine powders like cement dust. The core components of such systems are designed to ensure reliable, low-maintenance operation while maintaining high material transfer efficiency. Understanding the key components is essential for optimizing performance and ensuring longevity of the equipment.
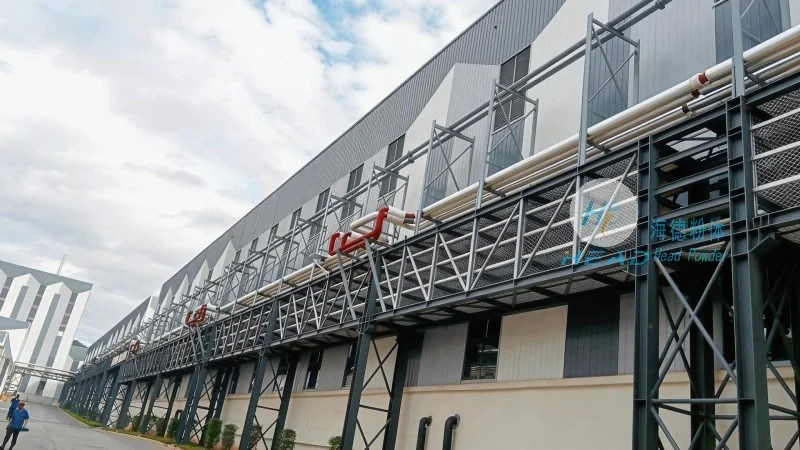
The pneumatic conveying system for cement dust typically comprises several integral parts, each playing a vital role in the overall operation. These components work in synergy to facilitate the movement of cement dust from the source to the destination. The primary components include the material feed system, the conveying pipeline, the air supply unit, the separation and filtration system, and the control mechanisms.
The material feed system is the initial stage where cement dust is introduced into the conveying line. This component ensures a consistent and controlled flow of the material, preventing blockages and maintaining system efficiency. For cement dust, which is often fine and prone to caking, specialized feeders like rotary valves or star feeders are commonly used. These devices provide a smooth, continuous feed, minimizing the risk of material degradation or system downtime.
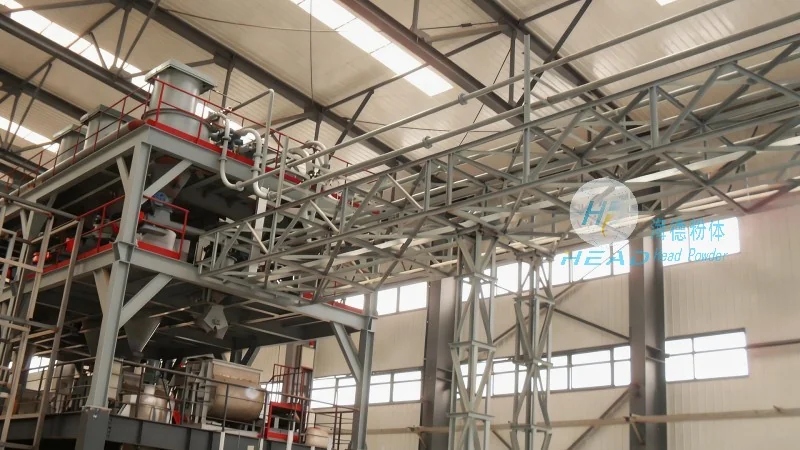
The conveying pipeline is the main channel through which cement dust travels under the influence of air. The design of the pipeline is crucial, as it must withstand the pressure and flow conditions while maintaining low friction losses. Typically, pipelines are made from materials like stainless steel or high-density polyethylene (HDPE) to resist corrosion and abrasion from the cement dust. The pipeline layout, including bends and vertical sections, is carefully engineered to minimize pressure drop and ensure smooth material flow. For long-distance conveying, the pipeline may include expansion joints or flexible connectors to accommodate thermal expansion and reduce stress on the system.
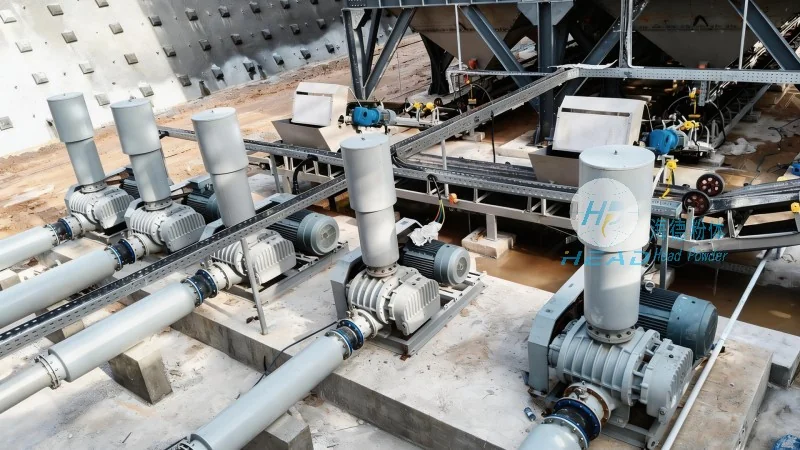
The air supply unit generates the necessary airflow to move the cement dust through the pipeline. This component can be either a positive displacement blower or a centrifugal fan, depending on the system requirements. Positive displacement blowers are preferred for high-pressure, low-volume applications, providing consistent pressure to overcome the resistance in the pipeline. The air supply unit is equipped with a motor and a control system to regulate the airflow and pressure, ensuring optimal performance under varying load conditions. Proper maintenance of the air supply unit, including regular cleaning of air filters and checking for wear on moving parts, is essential to prevent performance degradation.
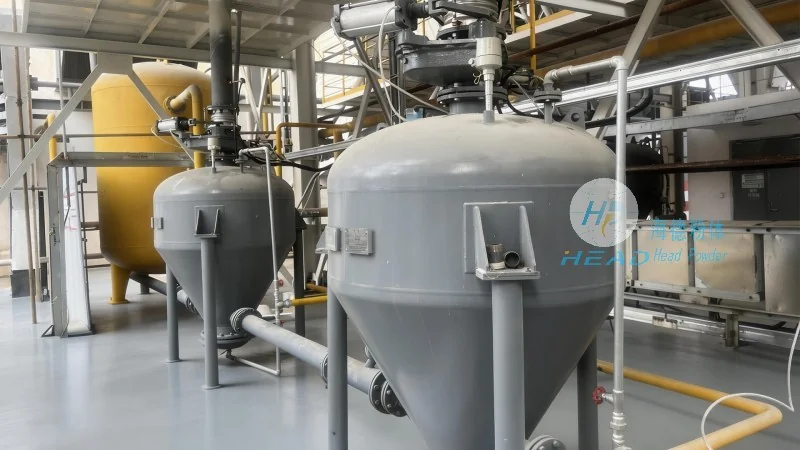
At the receiving end of the conveying system, the separation and filtration system is responsible for separating the cement dust from the air and returning the air to the system or releasing it to the environment. This component typically includes a cyclone separator, which uses centrifugal force to separate the dust from the air, followed by a bag filter or cartridge filter to capture any remaining fine particles. The separated cement dust is collected in a hopper or silo, while the cleaned air is either recirculated or discharged, depending on the system design. The efficiency of the separation and filtration system is critical to maintaining air quality and preventing dust emissions, which is essential for compliance with environmental regulations.
Control mechanisms are integral to the operation of the cement dust pneumatic conveying system, allowing for automated and precise management of the process. These systems typically include sensors to monitor pressure, flow rate, and material level, as well as control valves and actuators to adjust the feed rate and air pressure as needed. Modern systems may also incorporate programmable logic controllers (PLCs) or human-machine interfaces (HMIs) to provide real-time monitoring and remote control capabilities. The control mechanisms ensure that the system operates within safe and efficient parameters, reducing the risk of overpressure, underflow, or other operational issues. Regular calibration and maintenance of the control equipment are necessary to maintain system reliability and performance.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer specializing in the design and supply of pneumatic conveying systems for industrial applications. With a focus on cement dust and other fine powders, the company provides comprehensive solutions tailored to the specific needs of clients. HeadPowder's expertise lies in the integration of advanced components and engineering, ensuring that their systems meet the highest standards of efficiency, reliability, and environmental compliance. The company's headquarters is located in Shandong, China, where it maintains a state-of-the-art manufacturing facility and technical support team. By leveraging years of experience in the industry, HeadPowder delivers customized pneumatic conveying solutions that enhance operational performance and reduce maintenance costs for its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top