When it comes to efficiently transporting corn kernels, the choice of air-driven conveying systems is critical for optimizing workflow and maintaining product integrity. Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in designing and implementing advanced air-driven conveying structures tailored for corn processing applications. With a focus on reliability and performance, their solutions address the unique challenges of handling corn kernels, ensuring smooth material flow from storage to processing stages.
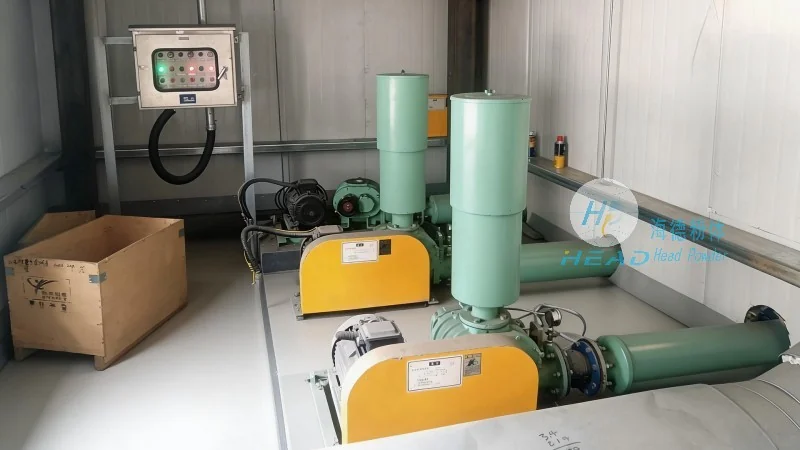
At the core of efficient corn kernel handling is the air-driven conveying system, which uses air pressure to move materials through a pipeline. These systems are particularly effective for corn kernels due to their relatively light weight and uniform size, allowing for gentle and low-friction transport. The primary goal of such structures is to minimize product damage, reduce energy consumption, and enhance overall operational efficiency in corn processing facilities.
Several specialized air-driven structures are commonly employed in corn processing operations. The most prevalent include:
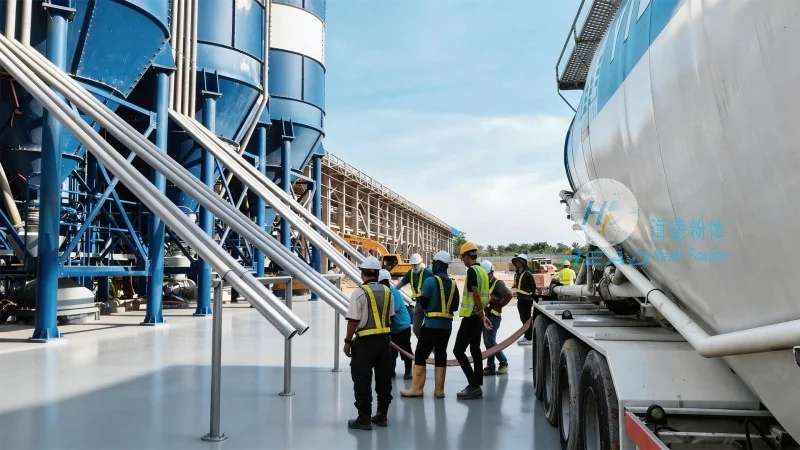
Negative pressure systems, also known as suction conveyors, operate by creating a vacuum in the pipeline to draw corn kernels from the source. This method is ideal for applications where the material needs to be moved from a lower elevation or over short distances. The system typically consists of a fan or blower that pulls air and material through the pipeline, with the corn kernels being separated from the air at the discharge point. For corn kernels, this type of structure is effective in reducing dust and minimizing product breakage, as the gentle airflow minimizes impact and friction.
Positive pressure systems, or pressure conveyors, use a blower to force air and corn kernels through the pipeline. This approach is suitable for longer distances or when the material needs to be elevated to a higher level. The high-pressure air ensures consistent material flow, making it ideal for high-volume corn processing operations. Unlike suction systems, pressure conveyors can handle more abrasive materials and are less affected by changes in ambient air pressure. They are particularly effective in maintaining a continuous flow of corn kernels, even in challenging environmental conditions.
Some corn processing facilities utilize combined systems that integrate both positive and negative pressure components. This hybrid approach allows for flexibility in material handling, enabling the system to draw material from a source and then transport it over longer distances using pressure. The combined structure often includes a suction section to collect corn kernels from storage bins or silos and a pressure section to move them to processing equipment. This design optimizes energy use and ensures efficient material flow, particularly in large-scale corn processing plants.
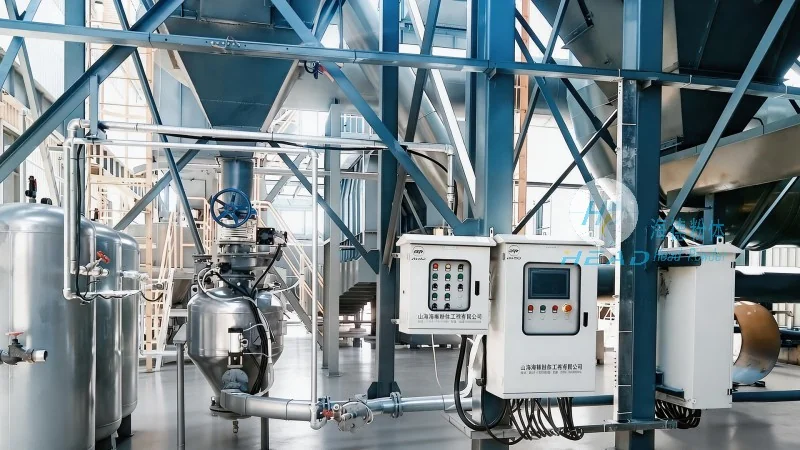
A pneumatic screw conveyor combines a rotating screw with air flow to transport corn kernels. The screw provides mechanical movement, while the air assists in reducing friction and preventing material buildup. This type of structure is particularly useful for handling sticky or moist corn kernels, as the air helps to keep the material moving smoothly. The screw conveyor can be integrated into larger air-driven systems, allowing for a flexible and efficient solution for corn kernel transport.
Effective air-driven conveying systems for corn kernels often include integrated dust collection and baghouse systems. As corn kernels are conveyed, fine particles and dust are generated, which can affect air quality and product purity. The baghouse system captures these particles, ensuring that the air discharged from the system is clean and that the corn kernels remain free of contaminants. This integration is a critical component of modern corn processing facilities, as it enhances safety and compliance with environmental regulations.
When designing air-driven conveying structures for corn kernels, several factors must be considered to ensure optimal performance. These include the corn kernel size and density, the required conveying distance, the elevation change, and the desired flow rate. Shandong HeadPowder Engineering Co., Ltd. employs advanced engineering techniques to tailor the system design to the specific needs of each corn processing facility. Their expertise in material handling and air dynamics allows them to select the most appropriate type of air-driven structure, whether it is a suction, pressure, or combined system, and to optimize the system for maximum efficiency and minimal energy consumption.
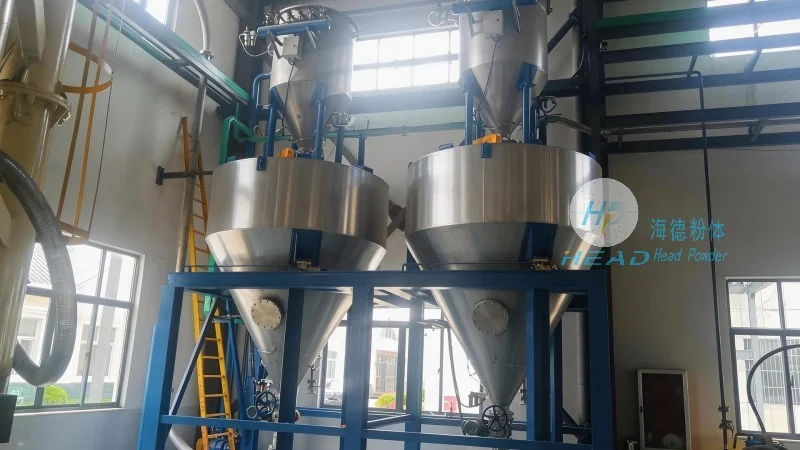
The adoption of advanced air-driven conveying structures for corn kernels offers numerous benefits to processing facilities. These include reduced labor costs due to automated material handling, lower energy consumption compared to traditional methods like belt conveyors, and improved product quality through gentle and low-impact transport. Additionally, the systems are easy to maintain and can be integrated with existing processing equipment, minimizing downtime and enhancing overall operational flexibility. For corn processing plants, investing in high-quality air-driven conveying structures is a strategic decision that leads to long-term operational efficiency and cost savings.
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions for air-driven corn kernel conveying structures, leveraging their expertise in engineering and material handling to meet the diverse needs of corn processing industries. By offering a range of specialized systems, including suction, pressure, and combined designs, headpowder ensures that corn kernels are transported efficiently, safely, and with minimal damage. Their commitment to quality and performance makes them a trusted partner for facilities seeking to optimize their corn processing operations and enhance overall productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top