HeadPowder, a leading provider in the field of material handling solutions, specializes in advanced pneumatic conveying systems designed for the efficient and reliable transport of powdered products, including powdered milk. This article explores the fundamentals of powdered milk pneumatic conveying, outlines the various classifications of such systems, and highlights their practical applications in industrial settings.
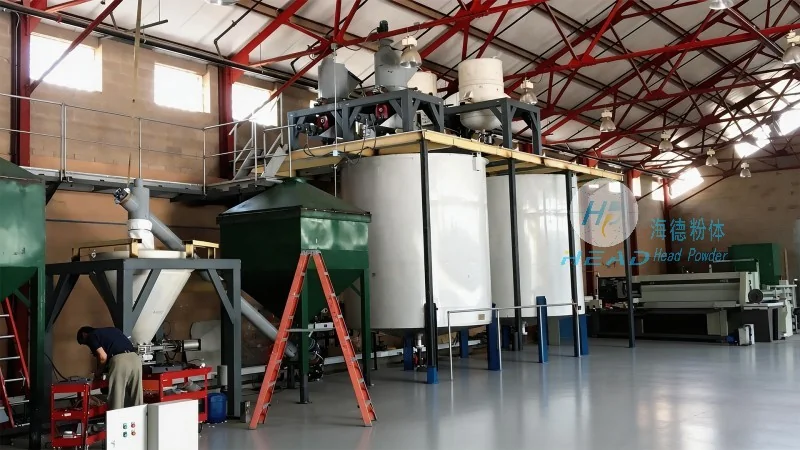
Pneumatic conveying is a method of transporting bulk materials through a pipeline using air or other gases as the conveying medium. In the context of powdered milk, this technology enables the safe and hygienic movement of sensitive products from storage to processing or packaging areas. The process involves creating a pressure differential within the system, which propels the powder particles through the pipeline. This approach offers significant advantages over traditional mechanical conveying methods, such as reduced contamination risk, lower maintenance requirements, and improved product quality preservation.
A typical powdered milk pneumatic conveying system consists of several critical components that work in tandem to ensure efficient operation. These include a hopper or feeder to store and meter the powder, a blower or compressor to generate the necessary air pressure, a pipeline network to transport the material, and a receiver or discharge unit to collect the material at the destination. Additionally, features like cyclones, filters, and dust collectors may be integrated to maintain system efficiency and product purity. The design of each component is tailored to the specific characteristics of powdered milk, such as its fine particle size and hygroscopic nature, ensuring optimal performance and minimal product degradation.
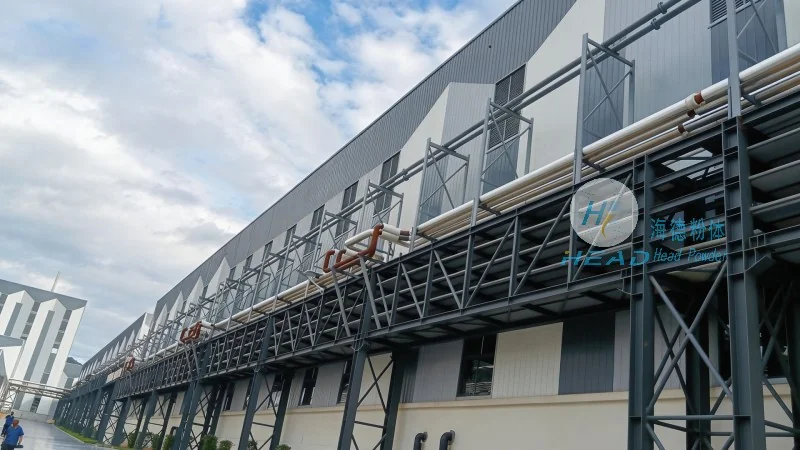
Pneumatic conveying systems are broadly classified based on the pressure used to move the material. The two primary categories are pressure and vacuum systems. Pressure systems operate by forcing air or gas into the pipeline under positive pressure, while vacuum systems create a negative pressure environment to draw material into the system. Within these categories, further sub-classifications exist, such as dilute phase and dense phase systems. Dilute phase systems use low air-to-material ratios, suitable for high-velocity transport over short distances, whereas dense phase systems employ higher material concentrations and lower velocities, ideal for handling abrasive or sensitive materials like powdered milk over longer distances. The choice of system type depends on factors like material properties, distance, and required flow rates.
Powdered milk pneumatic conveying systems find extensive applications across various industries, particularly in dairy processing and food manufacturing. One of the most common uses is the transfer of powdered milk from storage silos to production lines, where it is blended with other ingredients to create dairy products like yogurt, cheese, or infant formula. The systems are also employed in packaging operations, where the powder is conveyed from bulk storage to filling machines for bottling or bagging. Additionally, in industrial settings, these systems facilitate the integration of powdered milk into larger production workflows, ensuring seamless material handling and process efficiency. The hygienic design of these systems, with smooth surfaces and easy-to-clean components, makes them suitable for food-grade applications, adhering to stringent industry standards for product safety and quality.
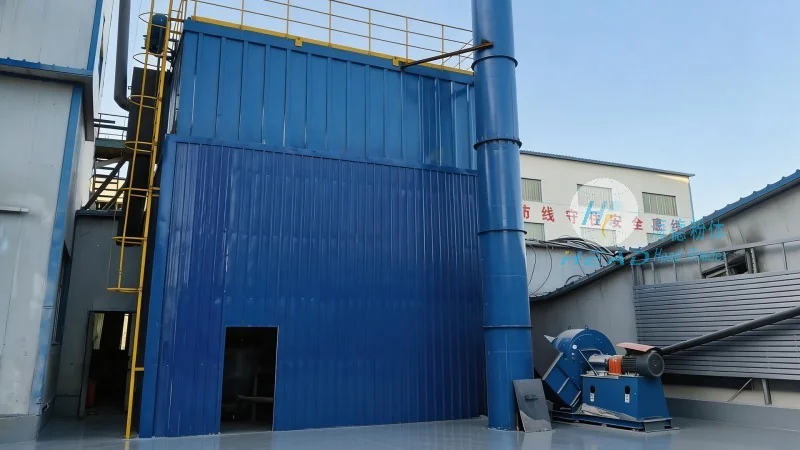
Implementing pneumatic conveying systems for powdered milk offers numerous benefits that enhance operational efficiency and product quality. Firstly, the technology minimizes product contamination, as the material is enclosed within the pipeline, reducing exposure to external pollutants. This is particularly crucial for sensitive dairy products where purity is paramount. Secondly, pneumatic systems reduce labor costs and maintenance requirements compared to mechanical conveyors, as they involve fewer moving parts and require less frequent servicing. Thirdly, the ability to handle fine, abrasive materials without causing wear and tear on equipment extends the lifespan of the conveying system. Furthermore, the flexibility of pneumatic systems allows for easy integration into existing production lines, enabling businesses to adapt to changing production demands without significant infrastructure modifications.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted manufacturer of high-quality pneumatic conveying systems tailored to the needs of the dairy industry. By leveraging advanced technology and adhering to industry best practices, the company provides reliable solutions for the efficient handling of powdered milk. Whether for short-distance transfers or long-distance transport, the classification and application of pneumatic conveying systems ensure optimal performance and product integrity. As a leading provider, HeadPowder continues to innovate and deliver solutions that meet the evolving demands of the food processing sector, supporting businesses in achieving operational excellence and maintaining product quality standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top