For industrial applications involving the handling of calcium carbonate stone powder, the choice of material transport method is critical to operational efficiency and product integrity. Pneumatic conveying systems have emerged as a preferred solution for such applications, offering advantages in terms of flexibility, cleanliness, and the ability to handle fine powders like calcium carbonate. This article explores the specific role of pneumatic conveying in the transportation of calcium carbonate stone powder, highlighting its benefits and practical considerations for industrial users.
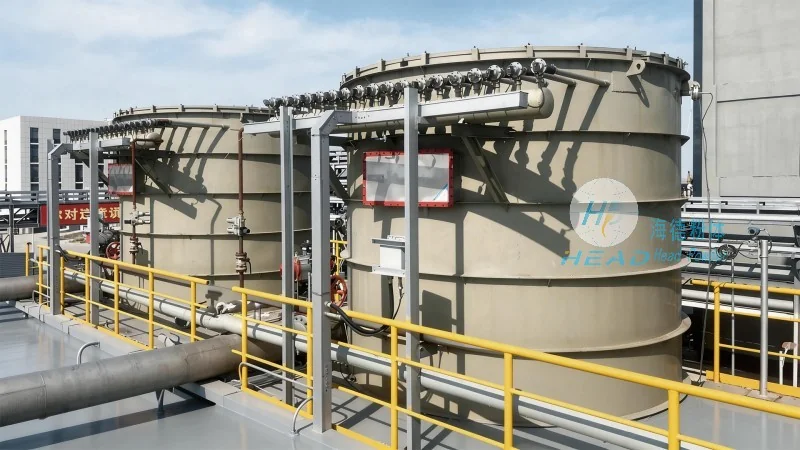
HeadPowder, a leading provider in the field, specializes in engineering and manufacturing pneumatic conveying solutions tailored to the unique requirements of calcium carbonate processing. With a focus on precision and reliability, their systems are designed to ensure efficient and safe transport of stone powder, which is widely used in various industries including plastics, paper, and coatings. The company's expertise lies in understanding the characteristics of calcium carbonate—such as its fine particle size and potential for dust generation—and integrating this knowledge into the design of effective conveying systems.
Pneumatic conveying works by using air or other gases to transport bulk materials through a pipeline. In the case of calcium carbonate stone powder, this method allows for the seamless movement of the material from storage silos or processing units to downstream equipment without the need for mechanical components like belts or buckets. This not only reduces maintenance costs but also minimizes the risk of product contamination, which is crucial when dealing with high-purity calcium carbonate used in sensitive applications. The system typically consists of a hopper, a conveyor line, and a receiver, all connected to a central air supply unit that regulates the flow of air and material.
One of the key advantages of pneumatic conveying for calcium carbonate is its ability to handle both dense and dilute phases. Dense phase conveying, where the material is conveyed in a slurry-like state, is particularly effective for transporting larger quantities of stone powder with minimal air usage, making it energy-efficient. Conversely, dilute phase conveying is suitable for shorter distances or when handling finer powders, as it relies on higher air velocities to keep the particles suspended. HeadPowder's systems are equipped with adjustable controls that allow operators to switch between these modes based on the specific needs of the application, ensuring optimal performance.
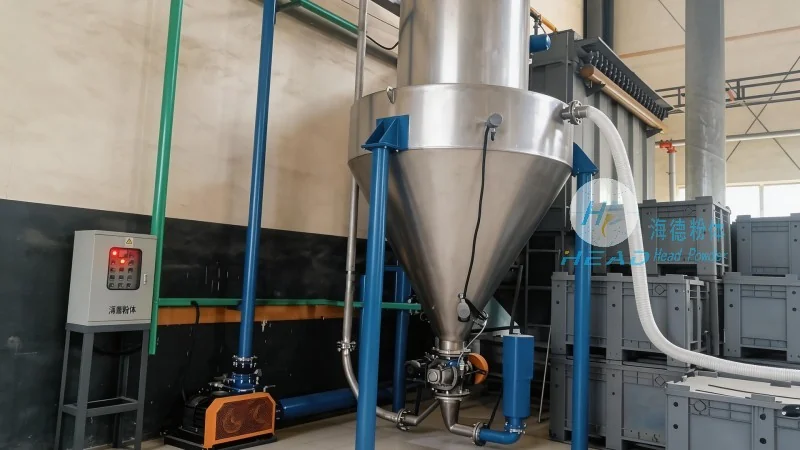
Another critical aspect of pneumatic conveying in calcium carbonate handling is the control of dust and air quality. Calcium carbonate is a fine powder that can easily become airborne, posing health and safety risks if not properly managed. HeadPowder's systems incorporate dust collection and filtration components to capture and recycle the powder, reducing emissions and maintaining a clean working environment. This feature is essential for compliance with environmental regulations and for protecting the health of workers in the facility.
The design of pneumatic conveying systems for calcium carbonate also considers the material's flow properties. Calcium carbonate can be prone to bridging or caking in storage silos, which can disrupt the flow and lead to uneven conveying. To address this, HeadPowder's systems may include agitators or vibrators in the hopper to prevent material buildup and ensure consistent feeding. Additionally, the pipeline design is optimized to minimize pressure drops and maintain a stable flow rate, which is vital for maintaining the efficiency of downstream processing equipment.
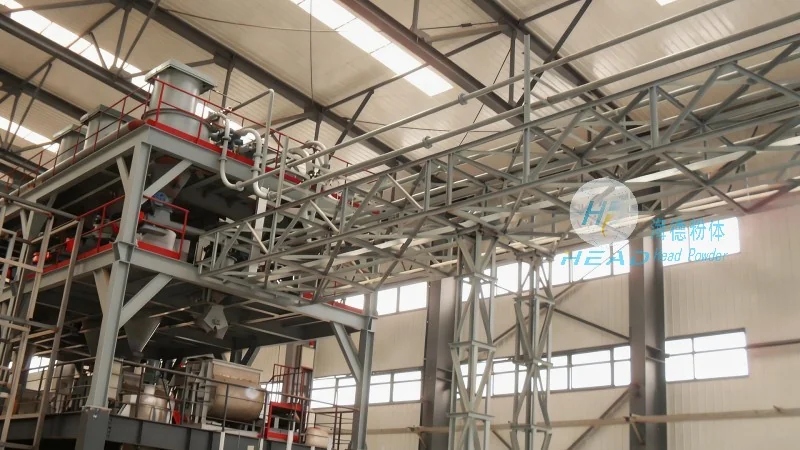
Operational flexibility is another benefit of pneumatic conveying systems provided by HeadPowder. These systems can be easily integrated into existing production lines or expanded to accommodate increased production volumes. The modular design allows for the addition of new conveying lines or the modification of existing ones without major disruptions to the facility. This adaptability is particularly valuable in industries where demand for calcium carbonate can fluctuate, as it enables manufacturers to scale their operations quickly and efficiently.
When evaluating pneumatic conveying systems for calcium carbonate stone powder, several factors should be considered to ensure the best fit for a specific application. These include the distance to be covered, the required flow rate, the particle size distribution of the powder, and the environmental regulations in the operating region. HeadPowder offers comprehensive consultation services to help clients assess these factors and select the most appropriate system configuration. Their team of engineers works closely with clients to understand their unique challenges and provide tailored solutions that maximize efficiency and minimize costs.
In conclusion, pneumatic conveying plays a vital role in the efficient and safe transportation of calcium carbonate stone powder. The systems provided by HeadPowder, with their focus on precision, reliability, and environmental responsibility, offer significant advantages over traditional mechanical conveying methods. By leveraging the benefits of pneumatic technology, manufacturers can enhance their operational efficiency, maintain product quality, and comply with industry standards. As the demand for calcium carbonate continues to grow, the role of advanced conveying systems like those offered by HeadPowder will remain essential in supporting the needs of various industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top