For industries dealing with fine sand and gravel, efficient material handling is crucial for maintaining operational efficiency and reducing costs. Pneumatic conveying systems have emerged as a highly effective solution, offering a reliable method to transport these materials over long distances and in various environments. This article explores the role of pneumatic conveying in the transport of fine sand and gravel, highlighting its benefits, technical considerations, and practical applications.
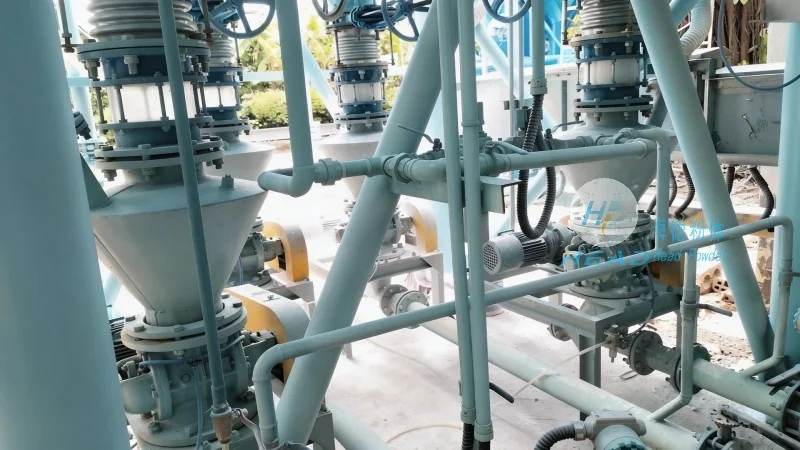
Pneumatic conveying, also known as air conveying, is a technology that uses pressurized or vacuum air to move bulk materials through a pipeline. It is widely used in industries such as mining, construction, and manufacturing for transporting materials like sand, gravel, and other granular substances. The system typically consists of a hopper, a conveyor line, and a receiver, with air being supplied by a blower or vacuum pump. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and wear.
When transporting fine sand and gravel, traditional methods such as belt conveyors or bucket elevators may face challenges like material degradation, blockages, and increased friction. Pneumatic conveying systems address these issues by providing a smooth, continuous flow of material. The primary advantages include:
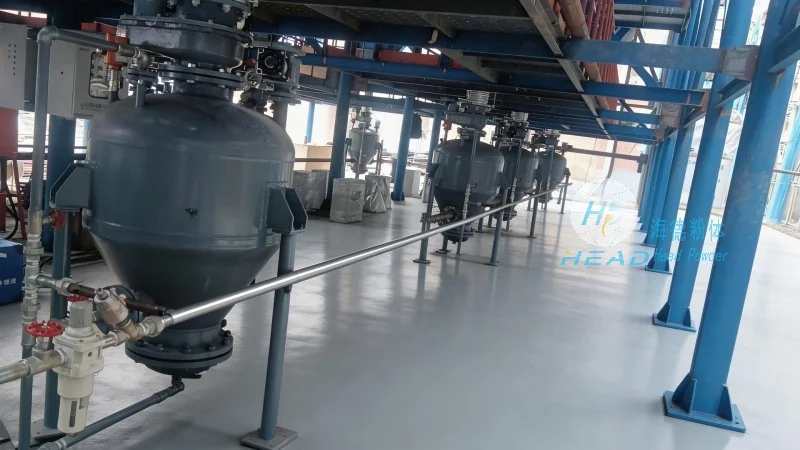
Transporting fine sand and gravel requires careful consideration of several technical factors to ensure optimal performance. The first is the particle size and density, as these affect the air velocity needed for proper conveying. The system must be designed to maintain a sufficient air-to-material ratio to prevent blockages and ensure smooth flow. Additionally, the choice of pipeline material and diameter is critical; larger diameters reduce friction losses, while materials like stainless steel or PVC are chosen for their resistance to corrosion and abrasion.
Pneumatic conveying systems are widely applied in various industries for fine sand and gravel transport. For instance, in the construction sector, these systems are used to move sand from storage silos to mixing plants, ensuring a consistent supply of material for concrete production. In mining operations, pneumatic conveyors transport crushed gravel from processing plants to storage areas, facilitating efficient material handling and reducing the need for manual labor.
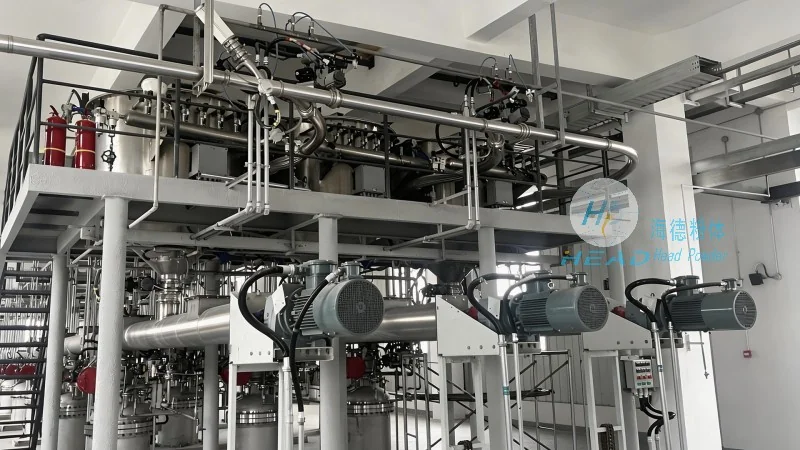
Headquartered in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer specializing in pneumatic conveying systems for fine sand and gravel transport. With a strong commitment to quality and innovation, the company has built a reputation for delivering reliable and efficient material handling solutions. Their team of engineers and technicians work closely with clients to understand their specific requirements, ensuring that the designed systems meet the highest standards of performance and durability.
Pneumatic conveying plays a vital role in the efficient transport of fine sand and gravel, offering numerous advantages over traditional methods. By leveraging advanced technology and careful system design, industries can achieve improved material handling efficiency, reduced costs, and enhanced product quality. As a trusted partner in material handling solutions, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide reliable pneumatic conveying systems that meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top