HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of pneumatic conveying systems for rare earth powders. This article delves into the various types of rare earth powder pneumatic conveying, their distinct characteristics, and the diverse applications where these systems are employed, offering a comprehensive overview for industry professionals and potential clients.
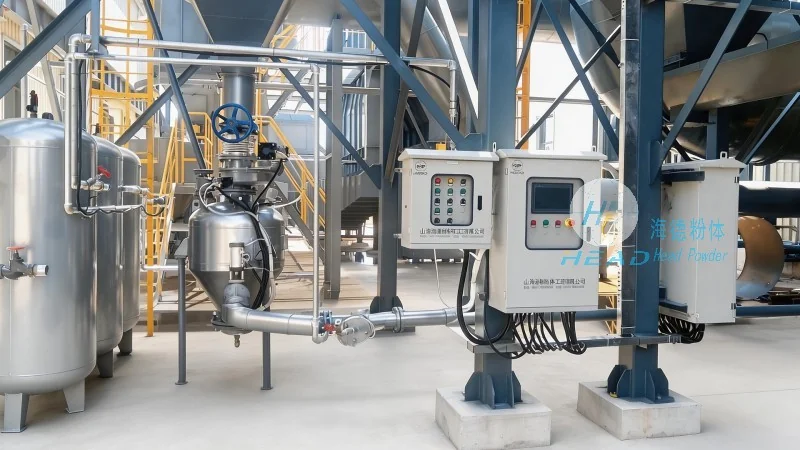
Rare earth powders, due to their fine particle size and high reactivity, require specialized handling methods to ensure efficient and safe transport. Pneumatic conveying systems have emerged as a preferred solution for moving these materials from one location to another within industrial facilities. These systems utilize air or gas as the conveying medium, enabling the transport of powders through pipelines without the need for mechanical components like belts or buckets. The choice of system type depends on factors such as material properties, distance, and throughput requirements.
There are primarily three types of pneumatic conveying systems used for rare earth powders: suction (or negative pressure) systems, pressure (or positive pressure) systems, and mixed (or combined) systems. Each type has unique operational principles and is suited to different operational scenarios.
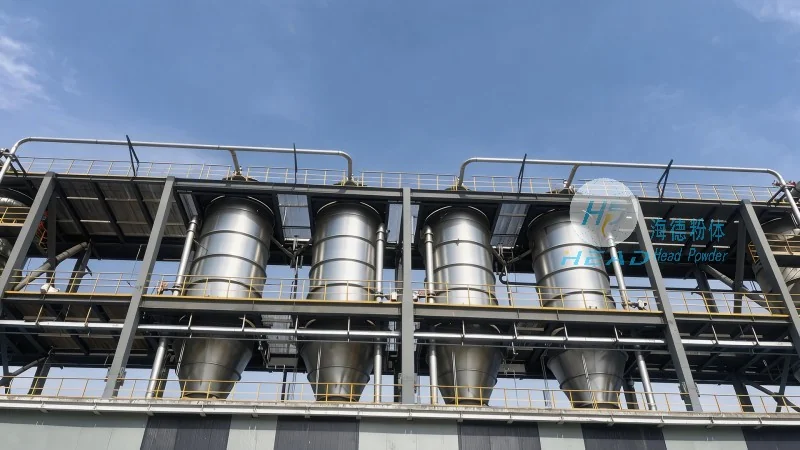
Suction systems operate by creating a negative pressure in the conveying line, drawing the material from the source (e.g., a hopper or storage silo) into the pipeline. This type of system is ideal for applications where the material is to be transferred from a lower elevation to a higher one, or when the material is to be collected from multiple points and consolidated into a single line. The primary characteristic of suction systems is their ability to handle powders with low to moderate flow rates and relatively short conveying distances. They are commonly used in industries where the material is to be transported from a storage area to a processing unit, such as in rare earth metal production facilities.
Pressure systems, conversely, operate by creating positive pressure at the material source, pushing the powder through the pipeline. These systems are well-suited for conveying materials over longer distances and at higher flow rates. They are particularly effective when the material is to be transported from a higher elevation to a lower one, or when the material needs to be distributed to multiple destinations from a single source. The key advantage of pressure systems is their ability to handle abrasive or corrosive materials without significant wear on the system components. This makes them ideal for rare earth powders that may contain hard particles or be mixed with other chemicals during processing.
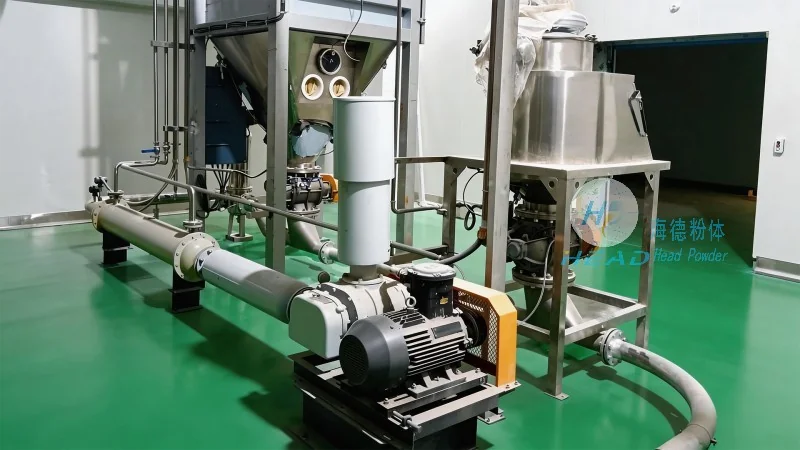
Mixed systems combine elements of both suction and pressure systems, offering greater flexibility in material handling. These systems can start with a suction phase to draw material from a source and then transition to a pressure phase to transport it over longer distances or to multiple destinations. This hybrid approach allows for efficient handling of materials with varying flow rates and distances, making them suitable for complex industrial setups where material is sourced from multiple points and distributed to several processing units. The mixed system is particularly valuable in rare earth processing plants where materials need to be transferred between different stages of production, such as from grinding to separation or from storage to packaging.
Regardless of the system type, rare earth powder pneumatic conveying systems share several key characteristics that contribute to their effectiveness and reliability. These include:
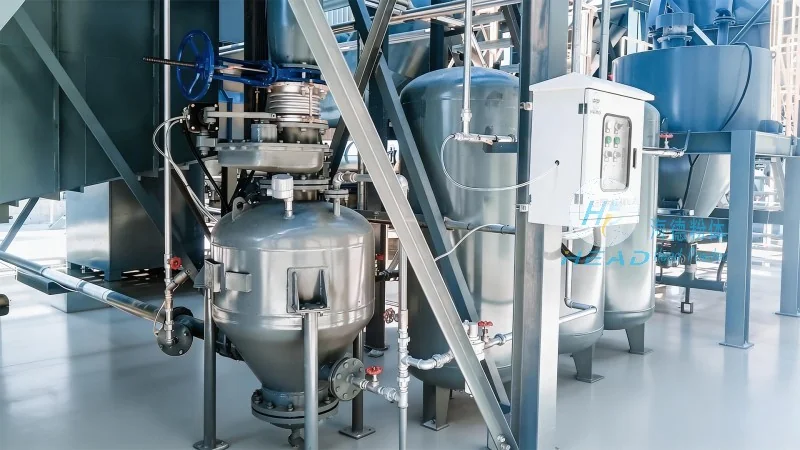
Rare earth powder pneumatic conveying systems are widely used across various industries due to their ability to handle fine, reactive powders efficiently. Some of the key applications include:
HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in providing customized pneumatic conveying solutions for rare earth powders. By understanding the unique characteristics of rare earth materials and the operational requirements of different industries, HeadPowder designs and implements systems that enhance efficiency, safety, and cost-effectiveness. Whether through suction, pressure, or mixed systems, the company's expertise ensures that rare earth powders are handled with precision, meeting the demands of modern industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top