Efficient handling of sintered dust is a critical aspect in industrial processes, particularly in the steel and metallurgical sectors. Pneumatic conveying systems offer a reliable method to transport these fine particles, and understanding the different operational modes—positive pressure and negative pressure—is essential for optimizing performance and ensuring safety. This article, presented by Shandong HeadPowder Engineering Co., Ltd. (headpowder), provides a detailed analysis of these two modes, highlighting their characteristics, applications, and key considerations for implementation.
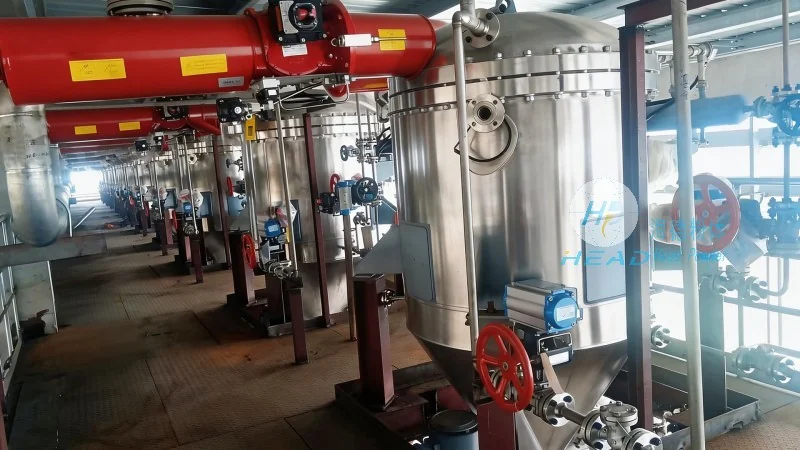
Pneumatic conveying systems utilize air or gas to transport bulk materials like sintered dust through a pipeline. The primary advantage of this technology is the ability to transport materials without mechanical contact, reducing wear and tear on equipment and minimizing the risk of contamination. For sintered dust, which is often fine and abrasive, selecting the appropriate conveying mode is crucial to maintain system efficiency and longevity.
Positive pressure systems operate by blowing air or gas into the conveying line, creating a pressure higher than the ambient air pressure. This method is commonly used for short to medium-distance transport and is particularly effective for materials that are non-abrasive or have a relatively high bulk density. The positive pressure mode ensures that the material is continuously pushed through the pipeline, reducing the risk of blockages and ensuring consistent flow rates.
In the context of sintered dust, positive pressure systems are often preferred for applications where the dust is generated in close proximity to the conveying equipment. The high pressure maintained in the system helps to maintain the velocity of the dust particles, preventing settlement and ensuring smooth transport. Additionally, positive pressure systems are generally easier to maintain and repair, as the equipment operates under higher pressure, making it simpler to detect and address leaks or blockages.
Negative pressure systems, also known as vacuum conveying, operate by creating a vacuum in the conveying line, drawing material from the source into the system. This mode is typically used for longer distances or when the material is light and has a low bulk density. The vacuum created pulls the sintered dust into the pipeline, and the air flow is then filtered and discharged, leaving the dust in a collection hopper.
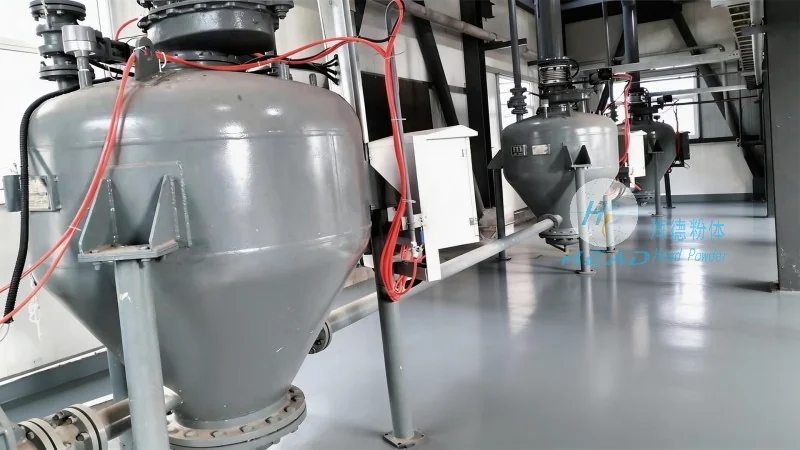
For sintered dust, negative pressure systems are advantageous in scenarios where the dust is generated at a distance from the collection point or where the material is very fine and prone to dusting. The vacuum helps to capture even the smallest particles, ensuring high collection efficiency. However, negative pressure systems require more careful design to prevent air leaks, as any leakage can reduce the vacuum pressure and compromise the conveying performance. Additionally, the filtration system in negative pressure systems must be robust to handle the fine particles, as clogging can lead to system downtime.
When comparing positive and negative pressure pneumatic conveying for sintered dust, several factors come into play. The choice of mode depends on the distance of transport, the properties of the dust (such as particle size, density, and abrasiveness), and the specific application requirements. Positive pressure systems are generally more suitable for shorter distances and materials with higher bulk density, while negative pressure systems excel in longer transport distances and for fine, low-density materials.
From an operational perspective, positive pressure systems are often more straightforward to operate and maintain, as they do not require complex vacuum generation equipment. However, they may consume more energy due to the continuous pressure maintenance. Negative pressure systems, on the other hand, can be more energy-efficient for long-distance transport but demand higher maintenance for the vacuum and filtration components.
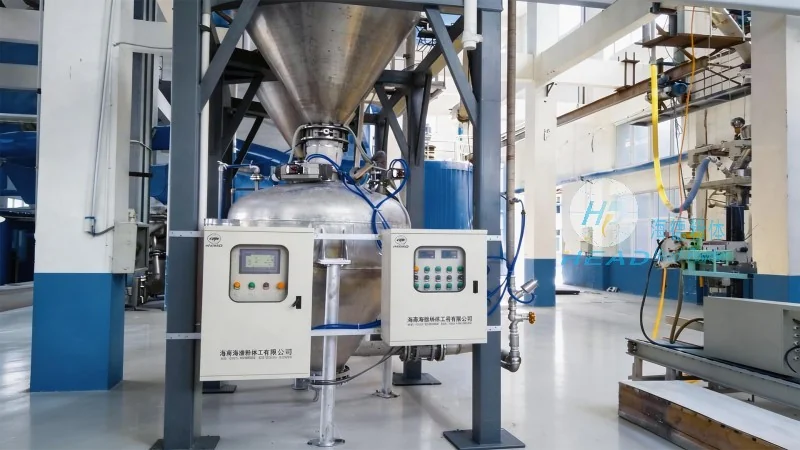
From a safety standpoint, positive pressure systems are less likely to cause dust explosions compared to negative pressure systems, as the system is under pressure and any leaks would release air rather than drawing in external air. Negative pressure systems, if not properly sealed, can create a suction effect that may draw in external air, potentially leading to dust accumulation and explosion risks. Therefore, safety measures such as explosion-proof designs and proper ventilation are critical when implementing negative pressure systems for sintered dust.
When deciding between positive and negative pressure pneumatic conveying for sintered dust, several key considerations should be evaluated. First, the distance between the dust generation point and the collection point is a primary factor. Short distances (typically less than 100 meters) are often better suited for positive pressure systems, while longer distances (over 100 meters) may require negative pressure systems. Second, the physical properties of the sintered dust, including particle size distribution, bulk density, and abrasiveness, influence the choice. Coarser or denser dust may perform better with positive pressure, whereas fine, light dust is more compatible with negative pressure.
Third, the available space and layout of the facility play a role. Positive pressure systems are generally more compact and can be installed in tighter spaces, as they do not require extensive vacuum infrastructure. Negative pressure systems, however, may need more room for the vacuum pump and filtration equipment. Fourth, the cost and maintenance requirements should be considered. Positive pressure systems may have lower initial costs and easier maintenance, while negative pressure systems can be more expensive due to the need for robust filtration and vacuum components.
Both positive and negative pressure pneumatic conveying modes offer effective solutions for handling sintered dust, with each having its own advantages and limitations. The selection of the appropriate mode depends on a thorough analysis of the specific application requirements, including transport distance, material properties, and operational constraints. By understanding the characteristics of each mode and considering the key factors outlined above, industrial facilities can optimize their sintered dust handling processes, improving efficiency, reducing downtime, and enhancing safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top