For industrial operations dealing with activated carbon powder, the efficiency and safety of material handling are paramount. Pneumatic conveying systems offer a solution to transport such powders, but they often present challenges related to dust leakage and material loss. This article explores effective strategies and best practices to prevent dust leakage when using pneumatic conveying systems for activated carbon powder, ensuring operational integrity and compliance with safety standards.
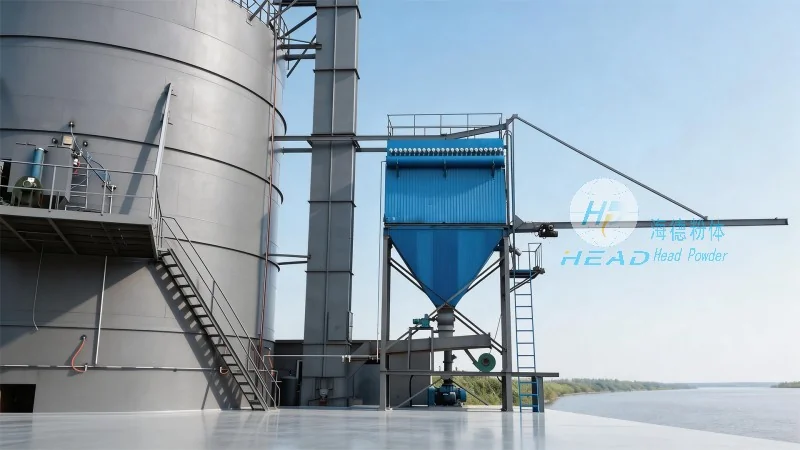
Activated carbon powder, due to its fine particle size and light weight, is highly susceptible to dispersion and leakage during transport. Traditional bulk material handling methods may not adequately address these issues, leading to environmental contamination, product loss, and increased operational costs. Pneumatic conveying systems, while efficient, require careful design and maintenance to mitigate these risks. The primary challenges include particle attrition, system pressure differentials, and equipment wear, all of which can contribute to dust leakage at joints, valves, and transfer points.
Implementing robust dust control measures is essential for maintaining the integrity of pneumatic conveying systems when handling activated carbon powder. Several key strategies have proven effective in reducing or eliminating dust leakage:
First, proper system design and equipment selection are critical. Using high-quality, dust-tight components such as airtight hoppers, flexible hoses with reinforced seals, and sealed valves can significantly reduce the risk of leakage. For instance, Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, emphasizes the use of specialized sealing mechanisms that are compatible with fine powders like activated carbon. Their engineered components are designed to maintain airtightness under varying pressure conditions, minimizing the escape of particles.
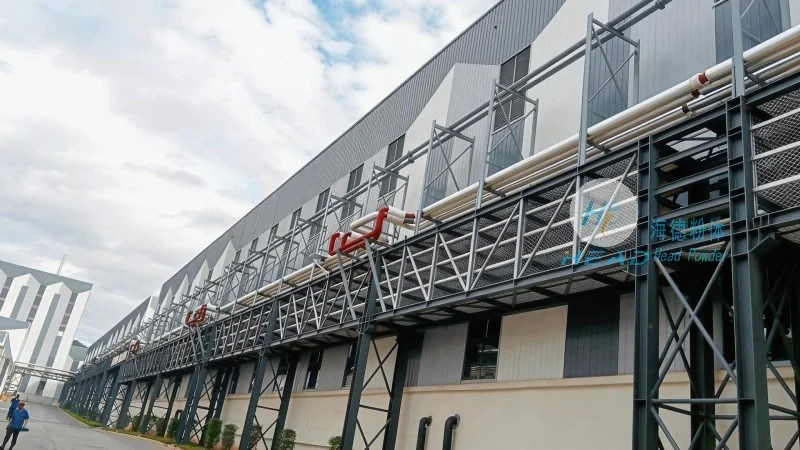
Second, maintaining consistent system pressure and flow rates is vital. Fluctuations in pressure can cause particles to escape from seams and connections. By using pressure regulators and flow meters, operators can ensure stable conditions, preventing excessive particle movement that leads to leakage. Additionally, regular monitoring of system pressure and flow helps in early detection of potential issues, allowing for timely maintenance.
Third, regular maintenance and inspection are non-negotiable. Dust accumulation in system components can create pathways for leakage over time. Conducting routine checks on seals, hoses, and valves, and replacing worn parts promptly, is essential. Shandong HeadPowder Engineering Co., Ltd. recommends a preventive maintenance schedule that includes visual inspections, pressure tests, and component replacements based on usage and wear patterns. This proactive approach helps in extending the lifespan of the system and maintaining its dust-tight performance.
Modern pneumatic conveying systems incorporate advanced technologies to further enhance dust control. One such technology is the use of closed-loop systems with recirculation or filtration. These systems capture any escaped particles and return them to the conveying line, reducing environmental impact and product loss. For activated carbon powder, which is often used in applications requiring high purity, closed-loop systems are particularly beneficial as they prevent contamination from external sources.
Another advanced feature is the integration of real-time monitoring and automation. Sensors can detect pressure drops or particle leakage in real time, triggering alerts or automatic adjustments to maintain system integrity. This technology not only improves dust control but also enhances overall operational efficiency by reducing downtime and maintenance needs. Shandong HeadPowder Engineering Co., Ltd. has integrated such smart technologies into their systems, providing clients with enhanced control and reliability.
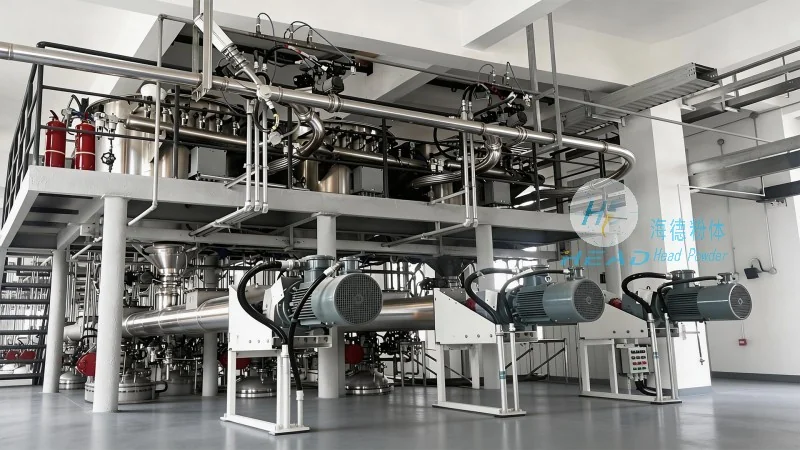
A leading chemical processing plant in China faced significant dust leakage issues when transporting activated carbon powder using an older pneumatic conveying system. The plant approached Shandong HeadPowder Engineering Co., Ltd. for a solution. The company conducted a thorough assessment of the existing system, identifying areas of weakness such as worn seals and inadequate pressure control. Based on the findings, they recommended and installed a new system with upgraded components, including reinforced hoses, high-quality valves, and a closed-loop filtration system.
After implementation, the plant reported a 90% reduction in dust leakage, leading to improved air quality, reduced product loss, and lower operational costs. The system also demonstrated enhanced efficiency in material transport, with consistent flow rates and minimal downtime. This case study highlights the effectiveness of combining proper system design with advanced technologies and regular maintenance to achieve optimal dust control in pneumatic conveying systems for activated carbon powder.
Preventing dust leakage in pneumatic conveying systems for activated carbon powder requires a comprehensive approach that combines proper system design, regular maintenance, and advanced technologies. By addressing the challenges of fine powder handling and implementing robust control measures, industrial operations can ensure safe and efficient material transport while minimizing environmental impact and product loss. Shandong HeadPowder Engineering Co., Ltd. remains committed to providing innovative solutions that meet these demands, helping clients achieve optimal performance and compliance in their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top