Desulfurization and dust removal processes in power plants and industrial facilities generate large volumes of ash and sludge, posing significant challenges for transportation and disposal. Traditional methods such as bucket elevators, belt conveyors, or manual handling often struggle with issues like dust pollution, material degradation, and operational inefficiencies. These challenges not only increase operational costs but also pose environmental and safety risks. In response to these needs, pneumatic conveying systems have emerged as a highly effective and efficient solution for handling desulfurization and dust removal ash, offering a reliable way to transport bulk materials over long distances while minimizing environmental impact.
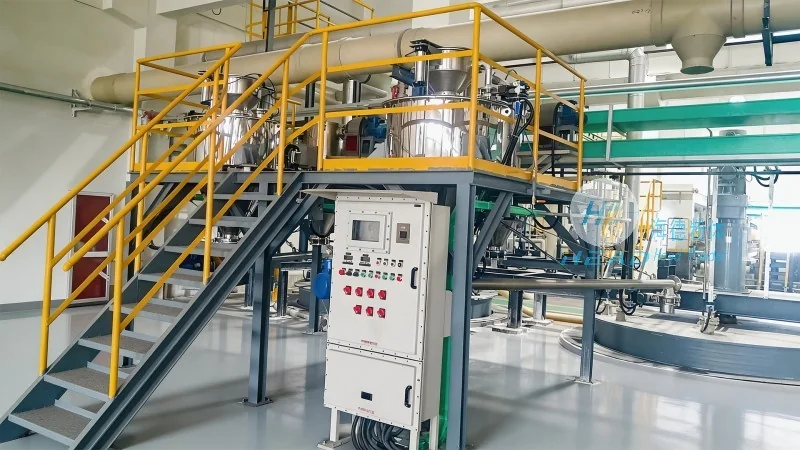
Pneumatic conveying systems utilize air or gas to transport bulk materials through a pipeline network. There are two primary types: dilute-phase and dense-phase systems. Dilute-phase systems use high-velocity air to suspend and move particles, suitable for short to medium distances and low to medium particle sizes. Dense-phase systems, on the other hand, use lower air velocities and higher material concentrations, ideal for long-distance transport and handling of abrasive or sensitive materials. The key advantages of pneumatic conveying for desulfurization ash include: 1) Reduced Dust Exposure: By enclosing the material in a sealed pipeline, the system minimizes dust emissions, improving workplace safety and environmental compliance. 2) Efficient Material Handling: Pneumatic systems can transport materials at high speeds, reducing overall handling time and increasing production throughput. 3) Low Maintenance and Long Lifespan: Compared to mechanical conveyors, pneumatic systems have fewer moving parts, leading to lower maintenance costs and longer operational life. 4) Flexibility and Scalability: The modular design of pneumatic conveying systems allows for easy expansion or reconfiguration to meet changing production demands.
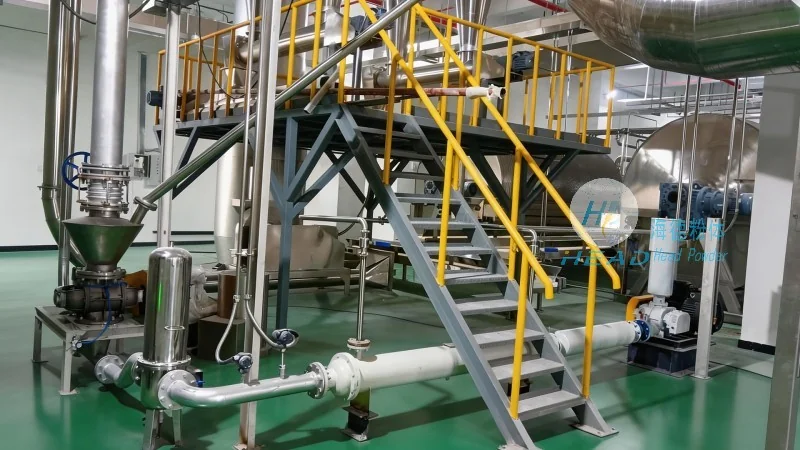
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier specializing in pneumatic conveying systems tailored for industrial applications, including desulfurization and dust removal ash transport. HeadPowder is headquartered in Shandong, China, and has years of experience in the field, developing comprehensive solutions that address the unique challenges of handling fine, abrasive, and moisture-rich materials. The company's expertise lies in designing customized systems that optimize material flow, ensure compliance with environmental regulations, and enhance overall operational efficiency. HeadPowder's products are engineered to withstand the harsh conditions associated with desulfurization ash, such as high temperatures, corrosive substances, and abrasive particles, ensuring long-term reliability and minimal downtime.
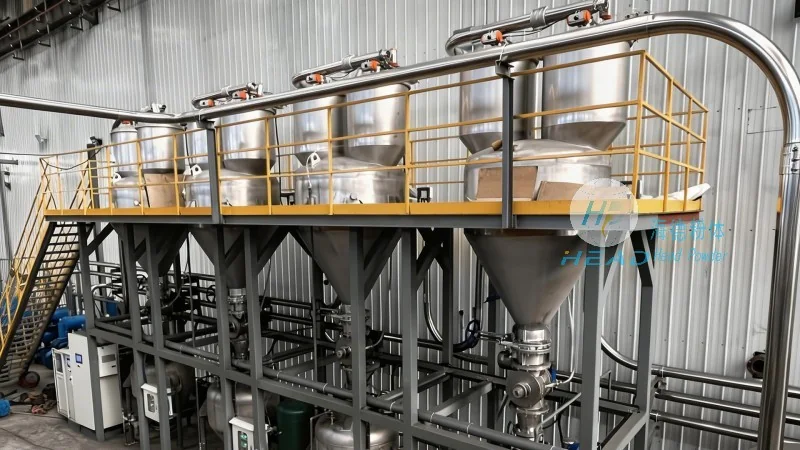
HeadPowder's pneumatic conveying systems for desulfurization ash are equipped with several key features that enhance performance and durability. These include: 1) Advanced Material Handling Technology: The systems utilize high-efficiency air pumps and specialized pipeline designs to ensure smooth and consistent material transport, even for fine particles that are prone to clogging. 2) Sealed and Dust-Free Operation: All components are enclosed in airtight structures, preventing dust leakage and maintaining a clean working environment. 3) Energy Efficiency: Optimized air flow and pressure control mechanisms reduce energy consumption, lowering operational costs. 4) Customizable Solutions: HeadPowder works closely with clients to design systems that meet specific process requirements, including varying material types, flow rates, and distance requirements. The company's solutions are widely used in power plants, steel mills, and other industrial facilities where efficient ash transport is critical.
Partnering with HeadPowder for pneumatic conveying systems offers numerous benefits for industrial facilities dealing with desulfurization and dust removal ash. The primary advantages include: 1) Enhanced Safety and Environmental Compliance: By minimizing dust emissions and providing sealed transportation, HeadPowder's systems help facilities meet stringent environmental regulations and improve workplace safety. 2) Increased Operational Efficiency: The high-speed and reliable transport capabilities of pneumatic systems reduce downtime and increase production output, leading to higher profitability. 3) Cost Savings: Lower maintenance costs, reduced material degradation, and energy efficiency contribute to long-term cost savings. 4) Expert Support and Service: HeadPowder provides comprehensive after-sales support, including installation, maintenance, and technical assistance, ensuring that clients receive reliable and efficient solutions throughout the system's lifecycle. With a strong commitment to quality and customer satisfaction, HeadPowder has built a reputation as a trusted partner in the industrial conveying industry.
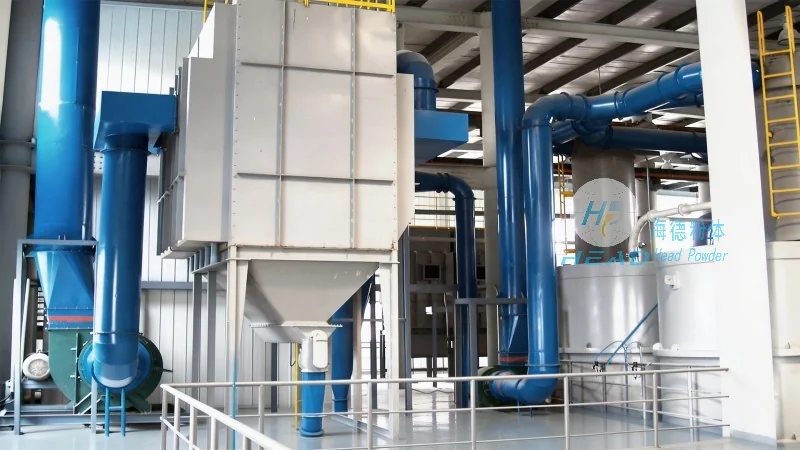
As industrial facilities continue to face challenges in handling desulfurization and dust removal ash, pneumatic conveying systems remain a superior solution for efficient, safe, and environmentally friendly material transport. HeadPowder, with its expertise and customized solutions, plays a crucial role in addressing these challenges and helping clients achieve their operational goals. By leveraging advanced technology and a customer-centric approach, HeadPowder ensures that facilities can optimize their ash transport processes, reduce costs, and comply with environmental standards. For industrial facilities seeking reliable and effective solutions for desulfurization ash transport, HeadPowder stands as a leading choice, delivering high-quality pneumatic conveying systems that meet the demands of modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top