Cloud Inesite, a mineral material with unique physical properties, presents significant challenges during transportation due to its particle size, density, and flow characteristics. Traditional bulk material handling methods often struggle with issues such as blockage, dust generation, and inefficient transfer between processing stages. Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial material handling solutions headquartered in Shandong, China, has developed advanced air-pneumatic conveying systems specifically designed to overcome these challenges and ensure reliable, efficient transportation of Cloud Inesite.
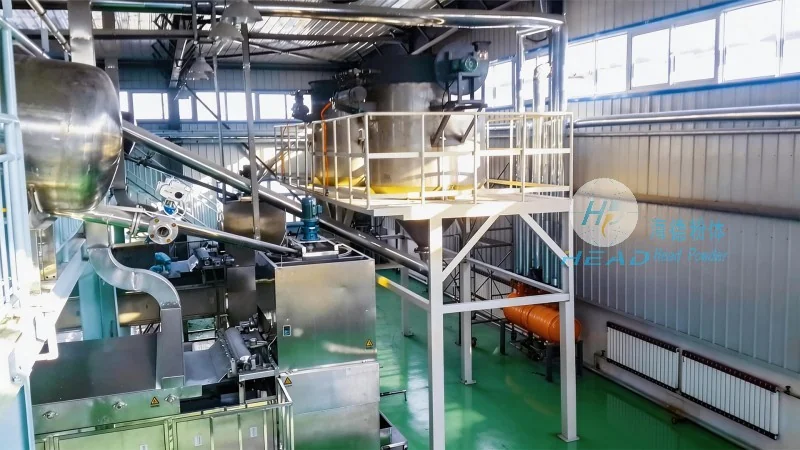
The core technology behind effective Cloud Inesite transportation lies in the air-pneumatic conveying system, which utilizes compressed air to transport bulk materials through a closed pipeline system. This method offers several key advantages over conventional methods. Firstly, it eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and operational downtime. Secondly, the enclosed system minimizes dust emissions, enhancing workplace safety and compliance with environmental regulations. Thirdly, the system provides precise control over material flow rates, allowing for consistent processing in downstream operations. For Cloud Inesite, which is known for its fine particle size and tendency to agglomerate, the air-pneumatic system's ability to maintain consistent air velocity and pressure is crucial for preventing blockages and ensuring smooth material transfer.
Recognizing that each Cloud Inesite handling application has unique requirements, Shandong HeadPowder Engineering Co., Ltd. offers tailored air-pneumatic conveying solutions. The company's engineering team works closely with clients to analyze the specific characteristics of the Cloud Inesite material, including particle size distribution, moisture content, and bulk density. Based on this analysis, they design systems that optimize air flow, pipeline layout, and equipment selection to maximize efficiency and minimize energy consumption. For example, in applications where long-distance transportation is required, the company may recommend high-pressure pneumatic systems with specialized valves and filters to maintain material integrity over extended distances. In other cases, low-pressure systems with cyclone separators may be preferred for shorter transport distances or where dust control is a primary concern.
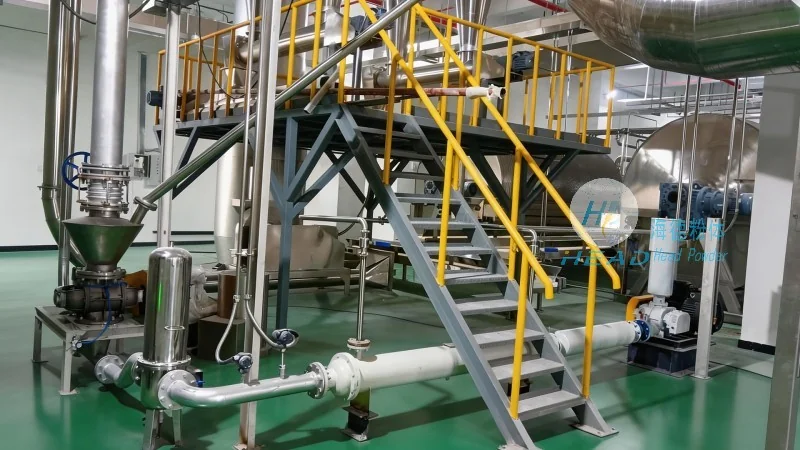
The effectiveness of an air-pneumatic conveying system for Cloud Inesite depends on several critical components. The compressor unit provides the necessary pressure and air volume, while the pipeline network ensures material is transported from the source to the destination. The system typically includes a hopper or feeder to introduce the material into the pipeline, and a receiver or silo to collect the material at the end point. For Cloud Inesite, which may be prone to clogging, the company incorporates features such as vibration devices, rotary valves, and pulse jets to maintain consistent material flow. These components work together to ensure that the system operates continuously without interruptions, even when handling materials with challenging flow properties. The result is a reliable and efficient transportation process that reduces operational costs and improves overall productivity.
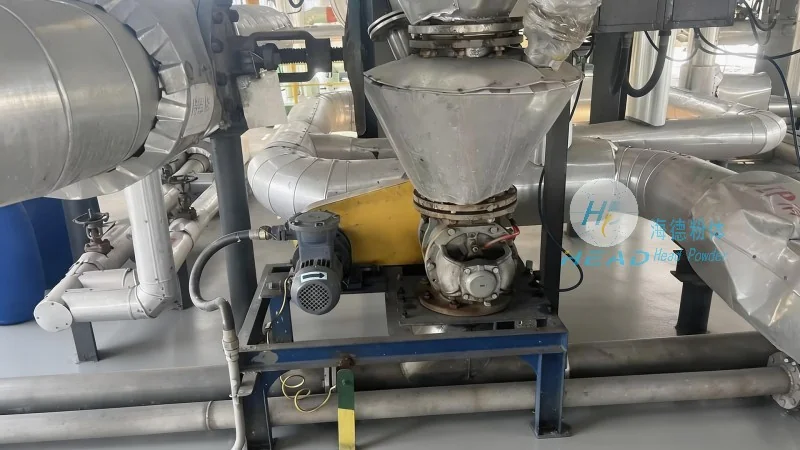
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented air-pneumatic conveying systems for Cloud Inesite in various industrial settings. One notable project involved a mining operation in China where the company installed a high-capacity system to transport Cloud Inesite from a quarry to a processing plant over a distance of 500 meters. The system was designed with a combination of high-pressure and low-pressure sections to handle the varying pipeline lengths and elevation changes. The result was a 30% reduction in transportation time and a significant decrease in dust emissions compared to traditional methods. Another application was in a manufacturing facility where the system was used to feed Cloud Inesite into a grinding mill. The precise control of material flow enabled the mill to operate at optimal efficiency, resulting in improved product quality and reduced energy consumption. These case studies demonstrate the versatility and effectiveness of the air-pneumatic conveying systems in handling Cloud Inesite and other similar materials.
For industries dealing with Cloud Inesite, the air-pneumatic conveying system represents a significant advancement in material handling technology. By leveraging the principles of pneumatic transport, Shandong HeadPowder Engineering Co., Ltd. provides solutions that address the unique challenges of this mineral material. The company's commitment to customized design, quality components, and reliable operation ensures that clients receive systems that meet their specific needs and contribute to their overall business success. As the demand for efficient and sustainable material handling solutions continues to grow, the air-pneumatic conveying systems for Cloud Inesite will remain a critical component in the industrial landscape, offering a reliable and effective way to transport this valuable material from source to processing point.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top