For agricultural operations dealing with oat handling, the challenge of efficient and reliable transportation from field to processing facilities is a critical concern. Traditional methods often struggle with the unique properties of oats, such as their lightweight and aerodynamic characteristics, leading to issues like material loss, uneven distribution, and increased operational costs. This is where advanced airflow conveying systems emerge as a game-changing solution, offering a robust and efficient approach to oat transportation. HeadPowder, a leading engineering company based in Shandong, China, specializes in developing and implementing such systems tailored to the specific needs of oat producers.
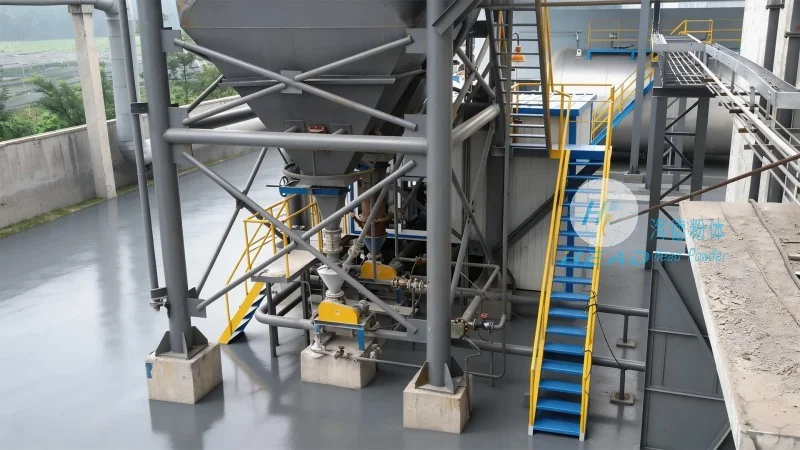
Oats, with their delicate structure and varying moisture content, require specialized handling to maintain quality and prevent damage during transit. Conventional conveyor systems may not adequately address the challenges posed by oats, leading to problems like clogging, segregation, and increased energy consumption. These issues not only affect the efficiency of the supply chain but also impact the overall profitability of oat processing operations. Recognizing these pain points, HeadPowder Engineering Co., Ltd. has focused on creating innovative solutions that leverage the principles of air-based transportation to overcome traditional limitations.
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has pioneered the development of advanced airflow conveying systems designed specifically for oat transportation. The core technology behind these systems involves the use of air pressure and velocity to move oats through a sealed pipeline, eliminating the need for mechanical components that can cause friction or damage to the grain. This approach not only enhances the safety and integrity of the oat product but also reduces maintenance requirements and operational costs. The system is engineered to handle a wide range of oat types, from whole grains to processed products, ensuring versatility and adaptability to different production stages.
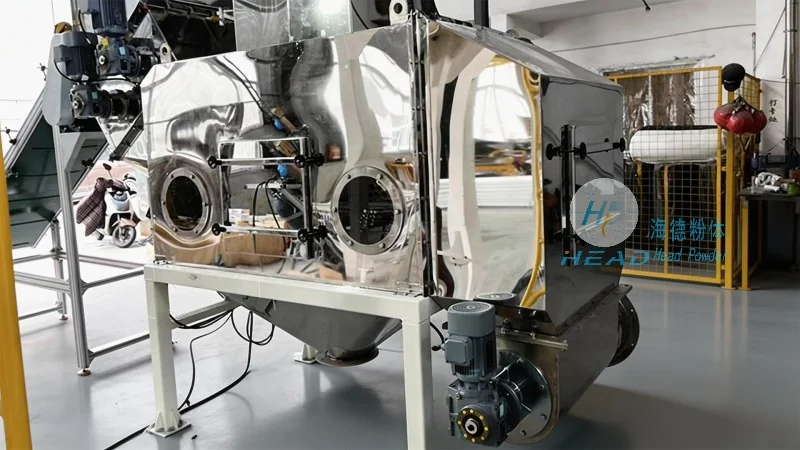
The airflow conveying system developed by HeadPowder offers several distinct advantages that make it an ideal choice for oat transportation. Firstly, it provides a dust-free and hygienic environment, which is crucial for maintaining the quality of oats, especially when they are intended for human consumption or animal feed. The sealed pipeline design prevents contamination from external sources, ensuring compliance with food safety standards. Secondly, the system is highly efficient in terms of energy consumption, as it utilizes air pressure to move material with minimal resistance, resulting in lower operational costs compared to traditional mechanical conveyors. Additionally, the system allows for precise control over the flow rate and direction of the oat stream, enabling better management of inventory and reducing the risk of overloading or underloading in processing facilities.
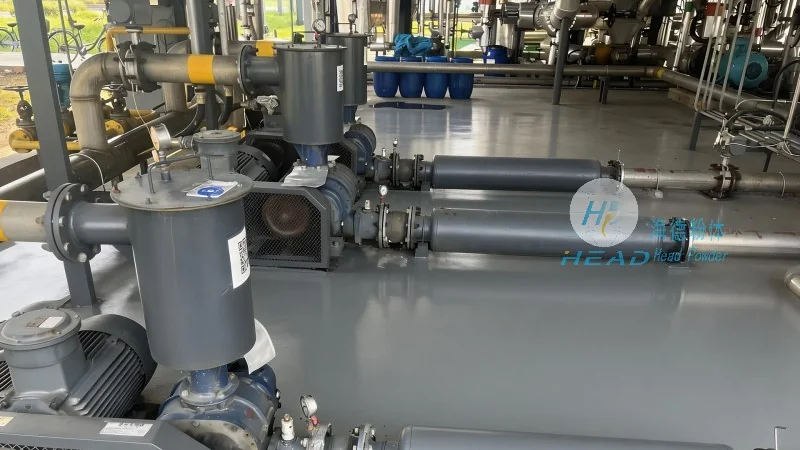
HeadPowder's airflow conveying systems have been successfully implemented in various oat processing facilities across China, demonstrating their effectiveness in improving operational efficiency and product quality. In one case study, a large oat processing plant in Shandong reported a 20% reduction in material loss and a 15% decrease in energy consumption after adopting the system. The system's ability to handle high volumes of oats while maintaining consistent quality has been a key factor in enhancing the plant's overall productivity. Furthermore, the system's modular design allows for easy integration with existing processing lines, minimizing downtime and facilitating smooth transitions to more advanced handling technologies.
As the demand for efficient and sustainable agricultural solutions continues to grow, the role of advanced airflow conveying systems in oat transportation becomes increasingly important. HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, remains at the forefront of developing innovative technologies that address the unique challenges of oat handling. By leveraging the principles of air-based transportation, the company's systems not only improve the efficiency of oat processing but also contribute to the overall sustainability of agricultural operations. For oat producers and processors seeking to enhance their supply chain performance, HeadPowder's airflow conveying systems offer a reliable and effective solution that aligns with modern industry standards and customer expectations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top