For industries dealing with sodium sulfate powder, efficient and reliable material handling is crucial to maintaining production efficiency and product quality. Pneumatic conveying technology has emerged as a key solution, offering a flexible and effective method for transporting fine powders like sodium sulfate. This article explores the application and optimization of pneumatic conveying systems specifically tailored for sodium sulfate powder, highlighting how such systems enhance operational performance and address common challenges in powder handling.
Sodium sulfate, also known as Glauber's salt, is a white crystalline powder widely used in various industries, including glass manufacturing, paper production, and chemical processing. Its fine particle size and hygroscopic nature make traditional conveying methods, such as belt conveyors or screw conveyors, prone to issues like dust generation, material degradation, and blockages. Pneumatic conveying, which uses air or gas to transport powders through a pipeline system, provides a solution that minimizes these problems while ensuring consistent flow and product integrity.
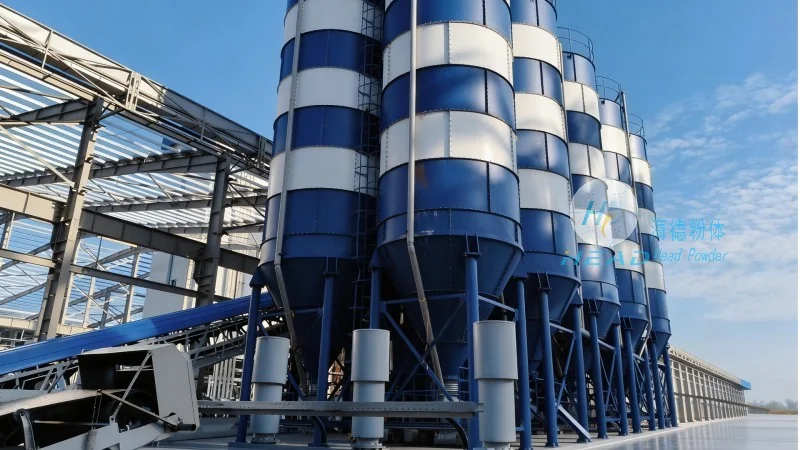
A typical pneumatic conveying system for sodium sulfate powder consists of several critical components. The system begins with a hopper or silo that stores the powder, equipped with a feeder to control the flow rate. The feeder is essential for maintaining a steady supply of material into the conveying line. Next, the material is introduced into a pipeline where it is carried by air or gas. The type of conveying system—whether it's pressure or vacuum-based—depends on the distance and layout of the conveying route. For sodium sulfate, pressure systems are often preferred due to their ability to handle longer distances and higher material loads without significant pressure loss.
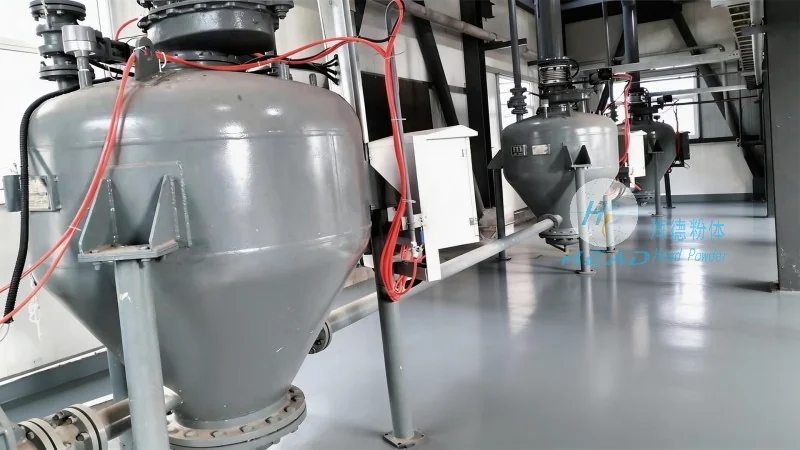
Optimizing the performance of a pneumatic conveying system for sodium sulfate powder involves several key factors. First, the air velocity must be carefully controlled to ensure that the powder particles are fully entrained and transported without causing excessive wear on the system components. The air velocity is typically determined based on the particle size, density, and flow rate of the sodium sulfate. Additionally, the system's pressure drop must be minimized to reduce energy consumption and maintain efficient operation. This can be achieved by selecting appropriate pipe diameters, using smooth pipe surfaces, and avoiding sharp bends or restrictions in the pipeline.
Despite the advantages of pneumatic conveying, certain challenges may arise when handling sodium sulfate powder. One common issue is the tendency of the powder to agglomerate or form clumps, which can lead to blockages in the system. To mitigate this, the system may include a de-agglomeration device or a vibratory feeder to break up the clumps before they enter the pipeline. Another challenge is the potential for dust generation, which can affect worker safety and product quality. Proper filtration and dust collection systems are essential to control airborne particles and ensure a clean working environment. Furthermore, the hygroscopic nature of sodium sulfate means that moisture can affect its flow properties and cause caking. Maintaining the system's temperature and using desiccants can help prevent moisture-related issues.
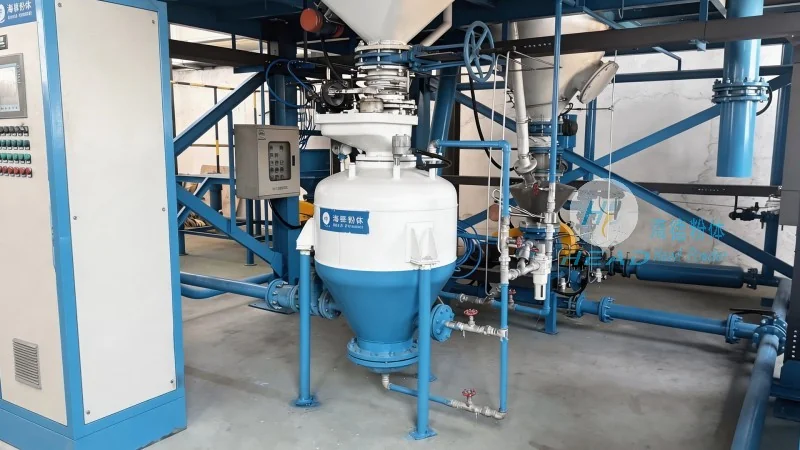
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, has successfully implemented pneumatic conveying systems for sodium sulfate powder in various industrial applications. One notable project involved a glass manufacturing plant that needed to transport sodium sulfate from a storage silo to a production line over a distance of 150 meters. The company designed a pressure pneumatic conveying system with a 100 mm diameter pipeline and a high-pressure blower. The system was optimized to maintain an air velocity of 20 m/s, ensuring efficient powder transport while minimizing energy consumption. The results showed a significant reduction in material handling time and an improvement in product quality, as the powder was transported without degradation or contamination.
Pneumatic conveying technology offers a highly effective and efficient solution for the transportation of sodium sulfate powder, addressing the unique challenges associated with fine, hygroscopic powders. By optimizing system components, controlling air velocity, and addressing common issues like agglomeration and dust, industries can achieve reliable and cost-effective material handling. As technology advances, further improvements in pneumatic conveying systems, such as the use of advanced materials and automation, will likely enhance their performance and expand their applications in the handling of sodium sulfate and other fine powders.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top