Hydrogen chloride (HCl) is a critical chemical in numerous industrial processes, and its safe and efficient transportation is essential for operational success and safety compliance. Pneumatic conveying represents a widely adopted method for handling HCl gas, leveraging compressed air or other gases to move the substance through a pipeline system. This approach offers advantages such as reduced risk of contamination, improved process control, and the ability to transport HCl gas over varying distances. This article provides a detailed overview of the working principles and classification applications of HCl pneumatic conveying systems, tailored for industrial users seeking reliable solutions.
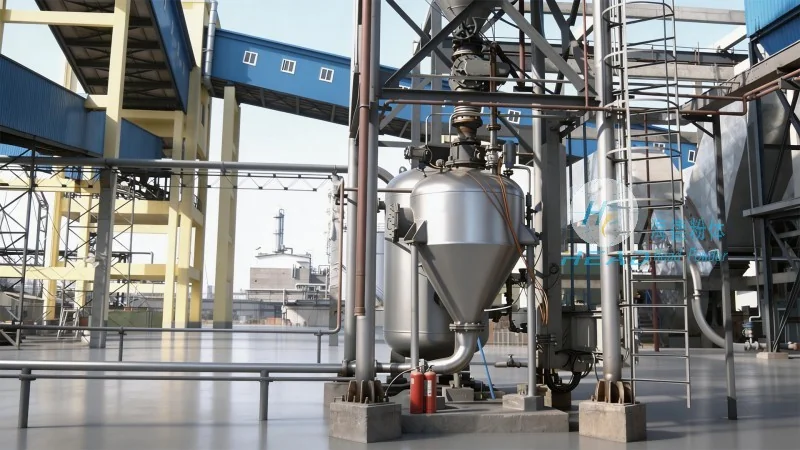
The fundamental mechanism of HCl pneumatic conveying revolves around the use of a high-pressure air stream to transport the gas. The process typically begins with the generation of compressed air, which is then introduced into the conveying line. As the air flows, it creates a pressure differential or negative pressure that draws the HCl gas from the source into the pipeline. The mixture of air and HCl gas travels through the system, often with the assistance of components like venturis or eductors to maintain flow and prevent blockages. The system may include filters, separators, and pressure regulators to ensure the HCl gas is conveyed safely and efficiently to the destination. The working principle is based on fluid dynamics, where the air flow provides the necessary force to move the HCl gas, while the system design minimizes energy consumption and ensures adherence to safety regulations.
Hydrogen chloride pneumatic conveying systems can be classified based on factors such as the type of conveying medium, operating pressure, and application requirements. The primary classifications include:
Dilute phase systems utilize a relatively low concentration of HCl gas mixed with a large volume of air. This method is suitable for long-distance transportation and is commonly employed in industrial settings where the HCl gas needs to be transported over several hundred meters. The system operates at relatively low pressure, typically around 0.5 to 2 bar, and relies on the velocity of the air to maintain the flow. Dilute phase conveying is efficient for transporting HCl gas with low solid content, as the air flow prevents the gas from settling or clogging the pipeline.
Dense phase systems, also known as high-pressure or positive pressure systems, use a higher concentration of HCl gas mixed with a smaller volume of air. This method is ideal for short-distance transportation or when the HCl gas contains solid particles or requires precise control. The system operates at higher pressures, typically ranging from 2 to 10 bar, and uses a slower air flow to ensure the HCl gas moves in a controlled manner. Dense phase conveying is commonly used in applications where the HCl gas needs to be delivered to reactors with high accuracy and minimal pressure loss.
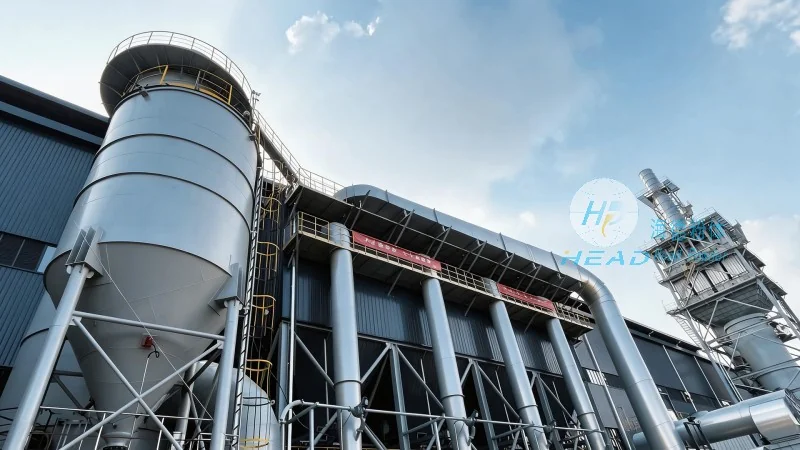
Vacuum conveying systems employ a vacuum pump to create a negative pressure in the pipeline, which draws the HCl gas from the source. This method is suitable for applications where the HCl gas needs to be collected from a low-lying source or where the gas is generated in a confined space. Vacuum conveying operates at low pressure, typically around 0.1 to 0.5 bar, and is often combined with cyclones or filters to separate the HCl gas from solid particles. This classification is particularly useful for handling HCl gas in environments where the gas is produced in situ and needs to be transported to a processing unit.
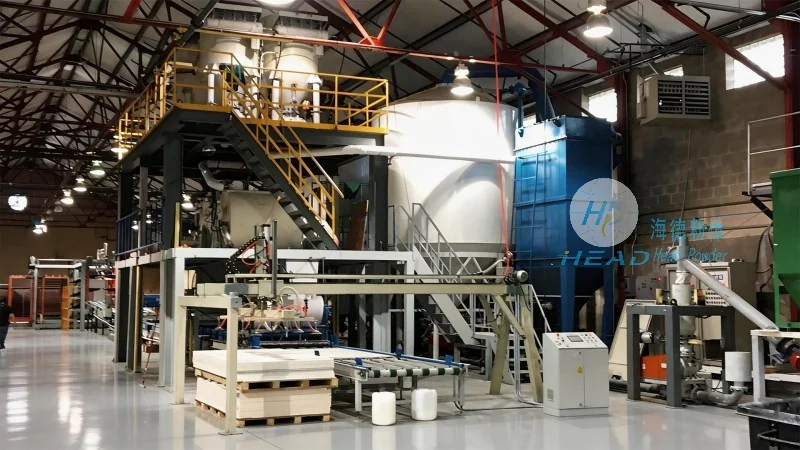
The classification of HCl pneumatic conveying systems directly influences their application across various industries. The dilute phase system is widely used in the chemical industry for transporting HCl gas from production units to storage or processing facilities. It is also employed in the pharmaceutical industry for handling HCl gas in sterile environments, where the system's low pressure and controlled flow prevent contamination. The dense phase system is commonly used in the manufacturing of chlorine and other derivatives, where the HCl gas needs to be delivered to reactors with high precision. Vacuum conveying is often used in the petrochemical industry for collecting HCl gas from gas streams or in the food processing industry for handling HCl gas in cleaning processes.
Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a leading provider of engineering solutions for chemical handling and processing. The company specializes in the design, manufacturing, and installation of pneumatic conveying systems for various chemicals, including hydrogen chloride. With extensive experience in the industry, HeadPowder has developed advanced technologies to ensure the safe and efficient transportation of HCl gas. The company's expertise includes selecting appropriate conveying systems based on specific application requirements, ensuring compliance with safety standards and regulatory mandates. HeadPowder's commitment to quality and innovation has established it as a trusted partner for industries relying on HCl gas handling solutions, delivering reliable and customized systems for diverse industrial needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top