For industries dealing with rare earth powders, efficient and reliable material handling is crucial to maintain production efficiency and product quality. The rare earth powder conveying system, particularly through pneumatic conveying technology, offers a sophisticated solution that addresses the unique challenges associated with handling these specialized materials. This article provides an overview of the rare earth powder conveying system, highlighting the key components and the significant advantages of pneumatic conveying in this application.
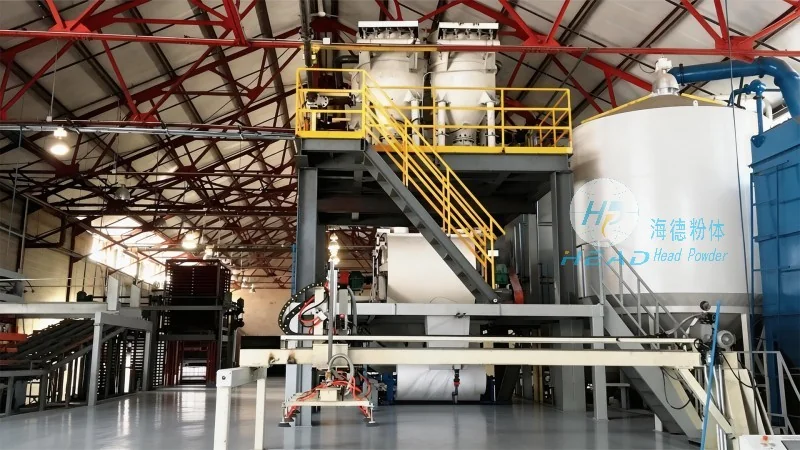
The rare earth powder conveying system is a specialized setup designed to transport rare earth powders from one location to another within a production facility or between different processing stages. At the core of this system are several critical components that work in tandem to ensure smooth and efficient material transfer. These components typically include a powder feeder, a conveying line (often equipped with airlocks or cyclones), a dust collector, and a control system. The powder feeder is responsible for accurately metering the rare earth powder, ensuring a consistent flow rate that matches the system's requirements. The conveying line, which can be either positive or negative pressure, transports the powder through the system using air or other gases. Airlocks and cyclones are used to separate the powder from the air stream, preventing material loss and ensuring that the powder reaches its destination without contamination. The dust collector is essential for capturing any fine particles that may escape the conveying line, maintaining air quality and complying with environmental regulations. The control system monitors and regulates the operation of all components, ensuring optimal performance and safety.
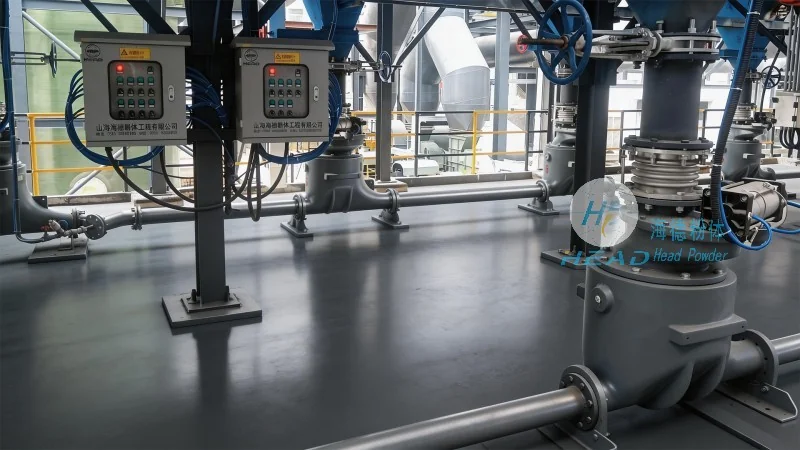
Pneumatic conveying offers several distinct advantages when it comes to transporting rare earth powders. One of the primary benefits is the ability to handle fine and abrasive powders without causing excessive wear or degradation. Unlike mechanical conveying systems, which may use moving parts that can be damaged by the abrasive nature of rare earth powders, pneumatic conveying uses air to move the material, minimizing contact and reducing the risk of particle breakdown. This is particularly important for rare earth powders, which are often used in high-value applications where particle size and purity are critical. Another advantage is the flexibility of the system. Pneumatic conveying can be configured to handle a wide range of powder types and flow rates, making it suitable for various production scenarios. The system can be easily scaled up or down to accommodate changes in production volume, and it can be integrated with other processing equipment, such as mixers or reactors, to create a seamless production line. Additionally, pneumatic conveying is generally more energy-efficient than other methods, as it requires less power to move the material over long distances. The system also offers better control over the material's temperature and moisture content, which is important for maintaining the quality of rare earth powders that are sensitive to these factors. Furthermore, pneumatic conveying systems are less prone to clogging compared to mechanical systems, as the air flow helps to keep the powder moving and prevents the buildup of material in the conveying line. This reduces downtime and maintenance costs, making the system more cost-effective in the long run.
The rare earth powder conveying system is designed to meet the specific needs of industries that work with rare earth materials. Some of the key features of this system include high-precision powder feeding, which ensures that the exact amount of powder is delivered to the next stage of processing. The system also includes advanced filtration and dust control measures to maintain a clean and safe working environment. The use of high-quality materials in the construction of the conveying line and components ensures durability and long service life, even when handling abrasive rare earth powders. The system is also designed with safety in mind, incorporating features such as pressure relief valves and emergency shutdown systems to prevent accidents and protect personnel. In terms of applications, the rare earth powder conveying system is widely used in the production of rare earth compounds, magnets, and other high-tech materials. It is also used in the recycling of rare earth materials, where the system helps to recover and reprocess these valuable resources. The system is particularly useful in applications where the powder needs to be transported over long distances or through multiple processing stages, as it can handle these challenges efficiently and effectively.
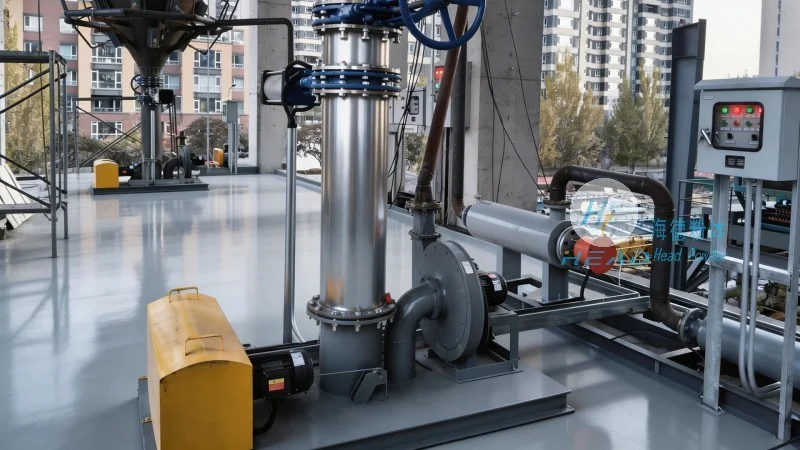
In conclusion, the rare earth powder conveying system, especially when utilizing pneumatic conveying technology, provides a highly effective and reliable solution for handling rare earth powders. The system's ability to handle fine and abrasive materials, combined with its flexibility and energy efficiency, makes it an ideal choice for industries that require precise and consistent material transfer. By leveraging the advantages of pneumatic conveying, companies can improve their production efficiency, maintain product quality, and reduce operational costs. As a leading provider of rare earth powder conveying systems, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized solutions that meet the unique needs of their clients. With a focus on quality, innovation, and customer satisfaction, HeadPowder has established itself as a trusted partner in the rare earth processing industry. Based in Shandong, China, HeadPowder leverages its expertise and experience to deliver cutting-edge conveying systems that help businesses achieve their production goals while adhering to the highest standards of safety and environmental compliance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top