Denitrification fly ash, as a byproduct of flue gas desulfurization and denitrification processes in thermal power plants, requires efficient and reliable handling methods for safe disposal and resource recovery. The pneumatic conveying system is a key technology in managing this material, offering advantages such as low energy consumption, minimal environmental impact, and flexible operation. This article provides an in-depth analysis of the denitrification fly ash pneumatic conveying system, focusing on its design principles, operational mechanisms, and practical applications.
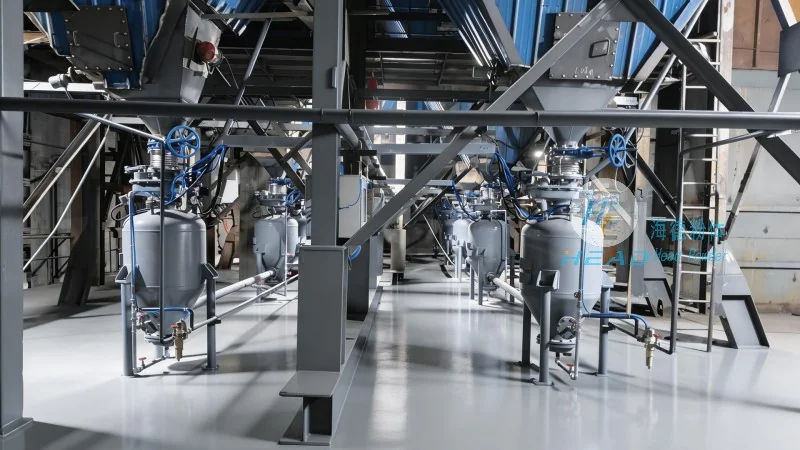
The denitrification fly ash pneumatic conveying system is engineered to transport fine particulate materials, including denitrification fly ash, from emission control equipment to storage or disposal facilities. The system typically consists of several critical components: a material feeding device, a conveying pipeline, a pneumatic conveying device (such as a blower or air compressor), and a dust collection system. The feeding device ensures consistent material flow into the pipeline, while the conveying device generates the necessary air pressure to move the ash particles. The pipeline network connects the emission control equipment to the storage or disposal site, with appropriate bends and valves to control the flow direction and pressure. The dust collection system, often integrated with the conveying pipeline, captures any airborne particles to prevent environmental contamination.
The pneumatic conveying system operates on the principle of air flow, where compressed air is used to suspend and transport the fly ash particles through the pipeline. There are two main types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems use low air velocity and high air-to-material ratios, suitable for long-distance and high-volume transport. Dense-phase systems employ higher air velocity and lower air-to-material ratios, which are ideal for short-distance transport and handling of abrasive or sensitive materials. The selection of the system type depends on factors such as the ash particle size, moisture content, and required transport distance. The system's operational efficiency is influenced by parameters like air pressure, flow rate, and pipeline diameter. Proper design and maintenance of these components are crucial to ensure stable and reliable operation, minimizing downtime and maintenance costs.
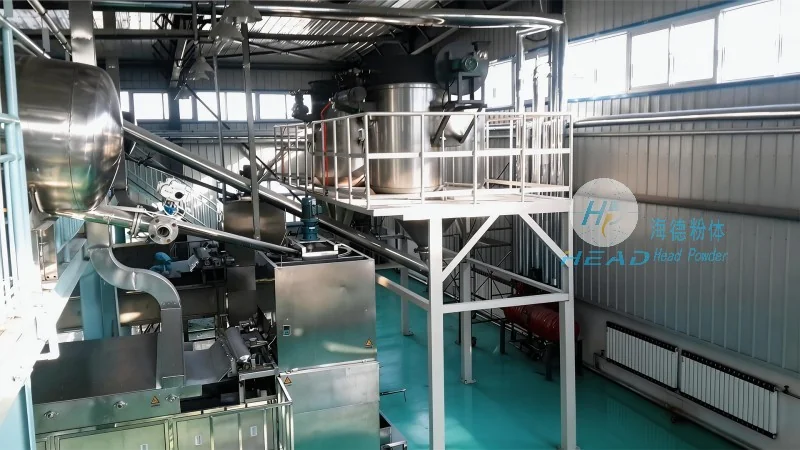
Compared to traditional mechanical conveying systems, the denitrification fly ash pneumatic conveying system offers several advantages. Firstly, it eliminates the need for moving parts in the conveying line, reducing wear and tear and maintenance requirements. Secondly, the system can handle a wide range of ash particle sizes and moisture contents, making it versatile for different power plant applications. Thirdly, the enclosed pipeline design prevents dust emissions, enhancing environmental safety and compliance with regulations. Additionally, the system can be integrated with other emission control equipment, such as baghouses or electrostatic precipitators, to form a comprehensive air pollution control system. The flexibility of the system allows for easy expansion or modification to accommodate changes in power plant operations or ash disposal requirements.
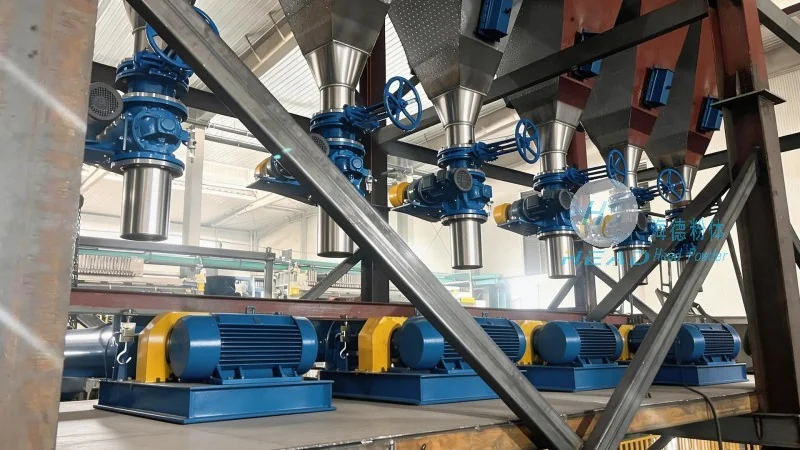
The denitrification fly ash pneumatic conveying system is widely used in thermal power plants, particularly those equipped with flue gas desulfurization and denitrification systems. The system is typically installed to transport fly ash from the denitrification unit to a storage silo or a landfill site. In some cases, the ash may be used as a raw material for cement production or other industrial applications, requiring the system to be designed for material recovery rather than disposal. The system's performance is evaluated based on factors such as transport efficiency, material loss, and environmental impact. Real-world applications have shown that the system can achieve high transport rates with minimal material degradation, ensuring the safe and efficient handling of denitrification fly ash.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing systems tailored to the needs of power plants and industrial facilities. With years of experience in the field, the company has developed a comprehensive range of products, including denitrification fly ash pneumatic conveying systems, that meet the highest standards of efficiency and reliability. The company's team of engineers and technicians is dedicated to providing customized solutions that address the unique challenges of each client's operation. HeadPowder's commitment to quality and innovation has earned it a reputation as a trusted partner in the power generation industry. The company's headquarters is located in Shandong, China, with a strong presence in both domestic and international markets.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top