Heptahydrate magnesium sulfate, commonly known as Epsom salt, is a widely used chemical compound in various industrial and agricultural applications. Efficient and reliable transportation of this powder and granular material is crucial for maintaining production efficiency and ensuring product quality. This article explores the application of pneumatic conveying systems for the transport of heptahydrate magnesium sulfate, focusing on how air currents can be utilized to move the material with high efficiency and minimal loss.
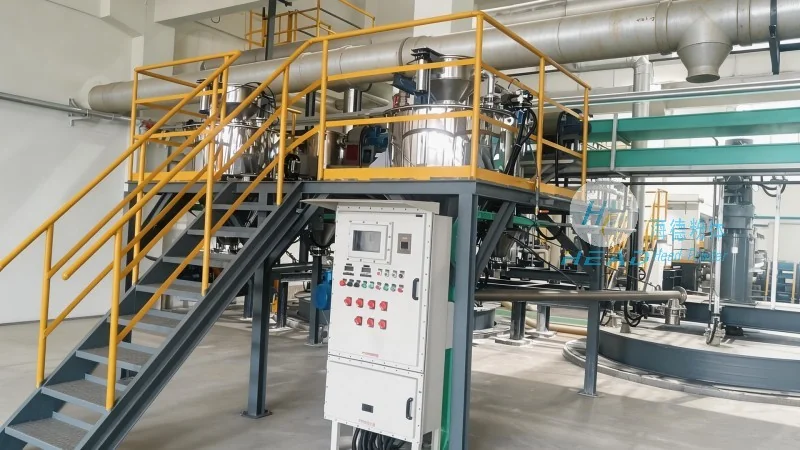
Pneumatic conveying, or air-assisted transport, is a method that uses pressurized or suction air to move bulk materials like powders and granules through a pipeline. This technology offers several advantages over traditional methods such as belt conveyors or bucket elevators, including reduced material degradation, lower maintenance costs, and the ability to transport materials over long distances without the need for multiple transfer points. The core of a pneumatic conveying system consists of a material feed hopper, a conveying line, and a receiver where the material is deposited. The system can operate under pressure (positive pressure) or vacuum (negative pressure), each with its own set of applications and benefits.
When designing a pneumatic conveying system for heptahydrate magnesium sulfate, several factors must be carefully considered to ensure optimal performance. The first is the material's physical properties, such as its particle size distribution, moisture content, and flowability. Heptahydrate magnesium sulfate typically has a relatively fine particle size, which can affect the system's air velocity requirements and the risk of clogging. Properly sizing the conveying line and selecting the appropriate air velocity are critical to prevent particle segregation and ensure consistent flow. Additionally, the material's hygroscopic nature means that moisture content must be monitored to prevent clumping or blockages in the system. The system design should include features like rotary air locks and cyclone separators to maintain air-tightness and separate the conveyed material from the air stream efficiently.
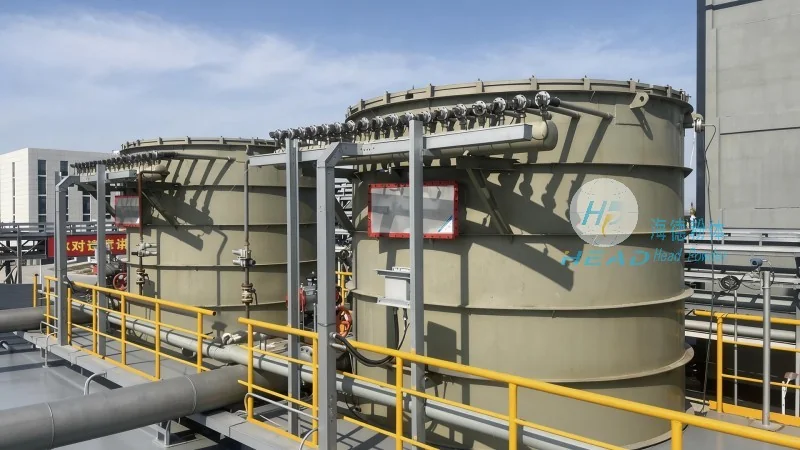
An effective pneumatic conveying system for heptahydrate magnesium sulfate consists of several key components that work together to ensure smooth operation. The material feed hopper is designed to store and feed the material into the conveying line. It often includes a feeder, such as a rotary valve or a screw feeder, to control the flow rate and prevent material buildup. The conveying line is typically made of stainless steel or other corrosion-resistant materials to handle the chemical properties of the magnesium sulfate and prevent contamination. The air supply system, which may include a blower or a vacuum pump, provides the necessary pressure or suction to move the material through the line. The receiver, usually a hopper or a storage tank, collects the material at the end of the conveying process. Cyclone separators are commonly used to separate the material from the air stream, and rotary air locks are installed at the inlet and outlet of the receiver to prevent backflow and maintain system integrity.
Implementing a pneumatic conveying system for heptahydrate magnesium sulfate offers numerous benefits that enhance operational efficiency and product quality. One of the primary advantages is the ability to transport the material in a closed system, which minimizes exposure to environmental factors and reduces the risk of contamination or dust emissions. This is particularly important for heptahydrate magnesium sulfate, which is often used in food and pharmaceutical applications where purity is critical. The closed system also helps in maintaining consistent moisture levels and preventing the material from absorbing moisture from the air, which could affect its performance. Another advantage is the reduction in labor costs and operational downtime. Unlike traditional conveyors that require regular maintenance and cleaning, pneumatic systems can be designed for continuous operation with minimal intervention. This leads to increased production throughput and lower overall operational costs. Furthermore, pneumatic conveying allows for the integration of the system with other processing equipment, such as mixers or reactors, enabling a seamless flow of materials from one stage to the next.
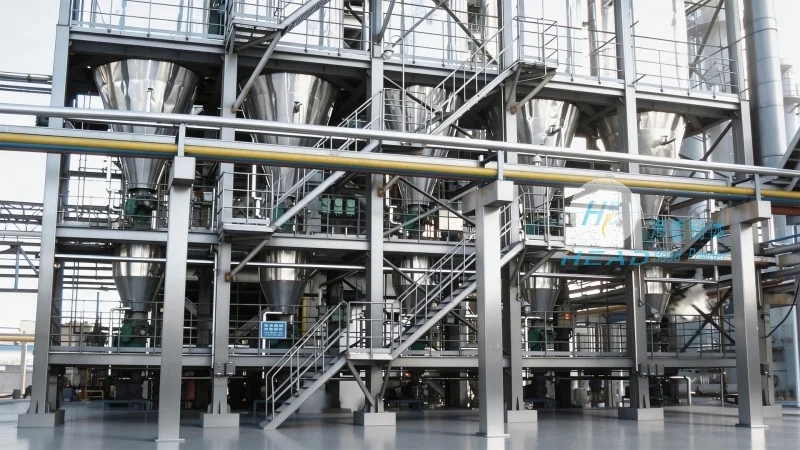
The application of pneumatic conveying for heptahydrate magnesium sulfate is widespread across various industries. In the agricultural sector, it is used as a fertilizer and soil conditioner, and pneumatic systems are employed to transport the material from storage facilities to application equipment. In the pharmaceutical industry, heptahydrate magnesium sulfate is used as a raw material in the production of various medications, and the closed conveying system ensures that the material remains sterile and free from contaminants. In the chemical industry, it is used as a precursor in the synthesis of other compounds, and the efficient transport via air currents helps in maintaining the quality of the intermediate products. Additionally, in the food industry, it is used as a dietary supplement and flavor enhancer, and the hygienic design of the pneumatic system is essential to meet regulatory standards. The versatility of pneumatic conveying makes it suitable for a wide range of applications, from small-scale laboratory operations to large-scale industrial production.
Efficient pneumatic conveying of heptahydrate magnesium sulfate is a critical aspect of modern industrial operations, enabling the smooth and reliable transport of this important material. By understanding the key components and considerations of a pneumatic conveying system, companies can optimize their processes and achieve higher levels of productivity. The use of air currents to move the material offers significant advantages over traditional methods, including reduced material degradation, lower maintenance costs, and improved product quality. For businesses looking to implement or upgrade their conveying systems, it is recommended to consult with experienced engineering firms that specialize in bulk material handling. Companies like Shandong HeadPowder Engineering Co., Ltd., with their expertise in pneumatic conveying systems, can provide tailored solutions that meet specific operational requirements and ensure long-term performance. By investing in a well-designed pneumatic conveying system, industries can enhance their operational efficiency, reduce costs, and maintain the high standards required for the production and use of heptahydrate magnesium sulfate.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top