Phosphate natrium airslide conveying systems represent a sophisticated and efficient method for transporting bulk materials, particularly in industrial settings where handling powders and granules is critical. This system leverages pneumatic principles to move materials through a sealed pipeline using air as the conveying medium. The technology is widely adopted in sectors such as chemical processing, food production, and mining, where maintaining material integrity and minimizing contamination are paramount.
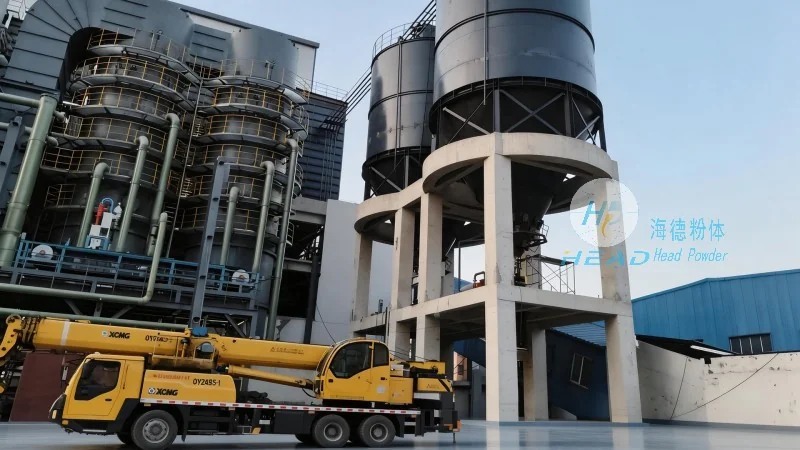
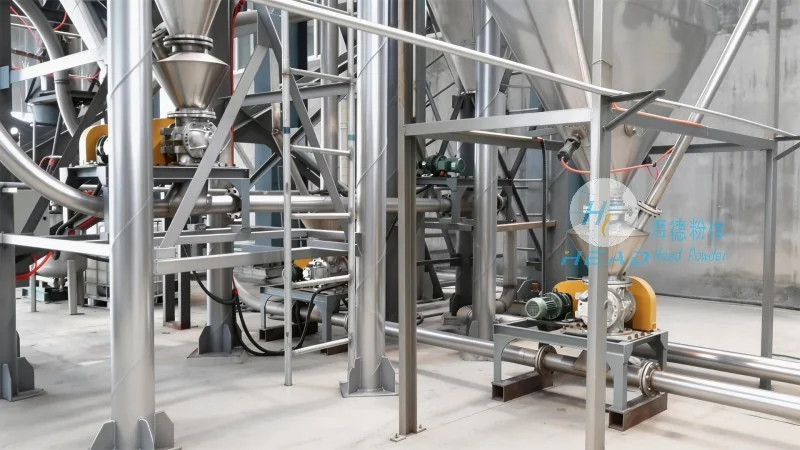
The airslide system comprises several key components that work in tandem to ensure smooth and reliable material transport. At its heart is the airslide conveyor itself, a long, flat, and perforated tube through which air is introduced under controlled pressure. The perforations allow air to flow through the material, creating a fluidized bed that enables the material to move under the force of air pressure. Other essential components include the air supply unit, which generates and regulates the air flow; the material feed hopper, which feeds the phosphate natrium into the system; and the discharge hopper, which collects the material at the end of the conveying line. Additionally, control valves and pressure regulators are integrated to maintain optimal air pressure and flow rates, ensuring consistent performance.
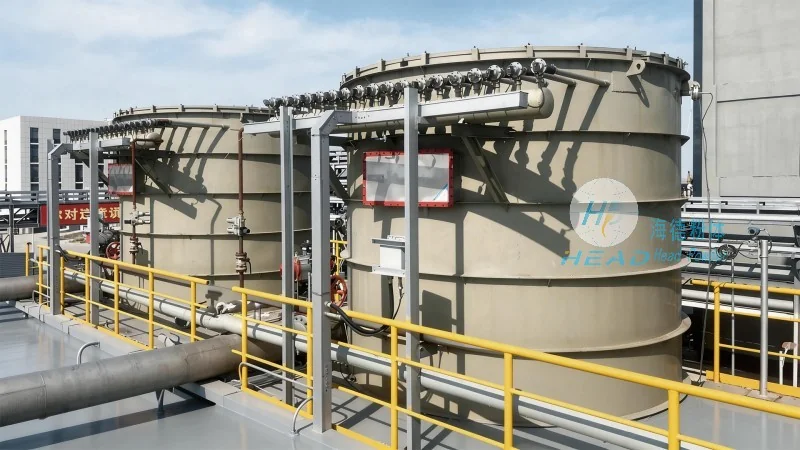
Implementing an airslide conveying system for phosphate natrium offers numerous advantages over traditional mechanical conveying methods. One of the most significant benefits is the ability to handle fine powders and granules without the risk of blockages or material degradation. The pneumatic nature of the system prevents the material from coming into direct contact with mechanical parts, reducing wear and tear and extending the lifespan of equipment. Furthermore, airslide systems are highly flexible, allowing for horizontal, vertical, or even inclined conveying paths, which can be tailored to fit the layout of a facility. This adaptability makes them ideal for complex production lines where material needs to be moved between multiple locations. Another key advantage is the reduced risk of dust contamination and environmental pollution, as the system operates in a sealed environment, containing dust and preventing it from escaping into the workplace. This not only improves safety but also complies with environmental regulations.
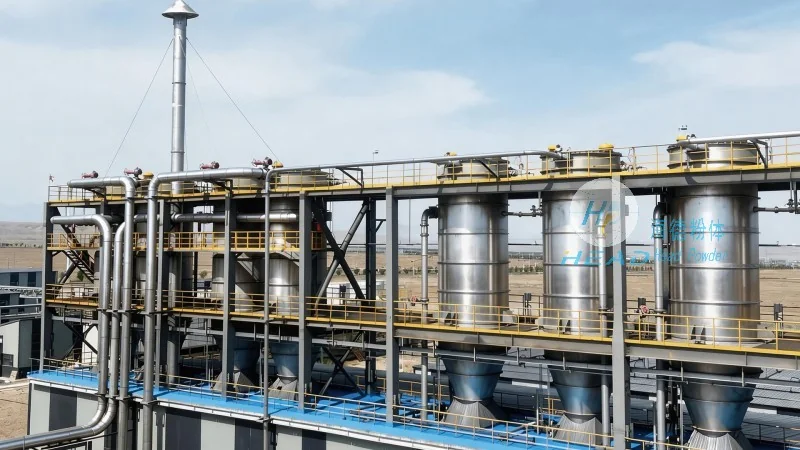
Phosphate natrium airslide conveying systems are commonly used in various industrial applications where bulk material handling is required. In the chemical industry, these systems are employed to transport raw materials and finished products, such as phosphate-based fertilizers or detergents, between processing units and storage silos. The food industry also benefits from airslide systems, particularly when handling food-grade phosphate natrium, as they ensure hygienic and contamination-free transport. Mining operations may use airslide conveyors to move phosphate ore from extraction sites to processing facilities, where the material is crushed and refined. Additionally, in the pharmaceutical sector, airslide systems are utilized to transport active pharmaceutical ingredients (APIs) and excipients, maintaining strict quality control standards. The versatility of airslide conveying systems makes them suitable for a wide range of applications, from small-scale laboratory operations to large-scale industrial production.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling solutions, including airslide conveying systems. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industry, providing customized solutions tailored to the specific needs of its clients. HeadPowder’s expertise lies in designing and manufacturing high-performance airslide systems that meet the rigorous demands of modern industrial applications. The company’s products are known for their durability, efficiency, and reliability, making them a preferred choice for businesses operating in sectors such as chemical processing, food production, and mining. HeadPowder’s commitment to customer satisfaction is reflected in its comprehensive after-sales support, including installation, maintenance, and technical assistance. The company’s headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. This infrastructure enables HeadPowder to deliver high-quality products and services to clients both domestically and internationally.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top