HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced powder handling solutions. The company's core product, the tonne bag powder conveying system, is engineered to efficiently manage bulk powder materials from large-scale storage bags. This system is widely utilized in industries such as food processing, chemical manufacturing, and pharmaceuticals, where reliable and safe material transfer is critical.
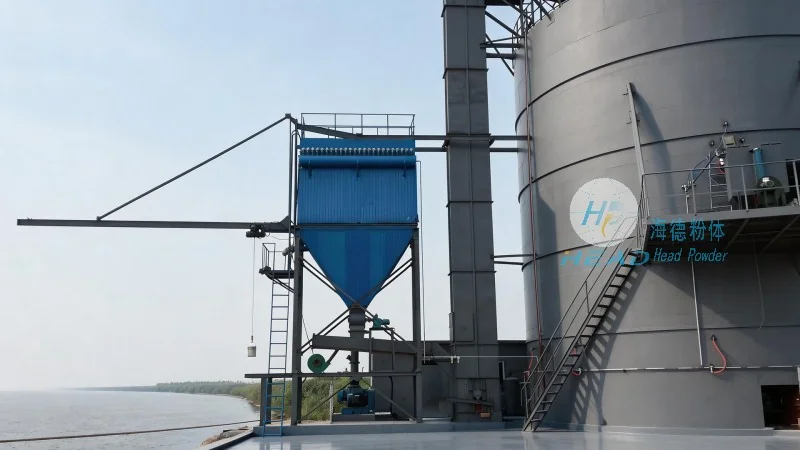
The tonne bag powder conveying system is a comprehensive solution designed to automate the handling of bulk powders from tonne bags. It integrates multiple components to ensure seamless material transfer from the storage bag to the processing equipment. The system is built with durability and efficiency in mind, catering to high-volume production environments. Each component is strategically positioned to optimize workflow and minimize downtime.
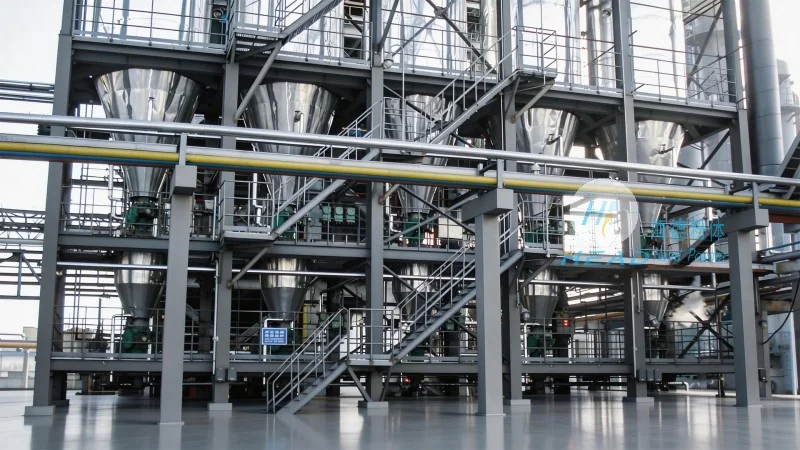
The system comprises several essential parts that work in tandem to achieve effective powder transfer. The primary components include a bulk bag discharger, a conveyor system, a dust collection unit, and a control panel. The bulk bag discharger is responsible for opening and emptying the tonne bag, ensuring that the powder flows smoothly into the conveyor. The conveyor system, typically a screw or pneumatic conveyor, transports the powder from the discharger to the processing area. The dust collection unit is integrated to capture and filter any airborne particles, maintaining a clean and safe working environment. The control panel allows operators to monitor and adjust the system's operation, ensuring precise control over the material flow.
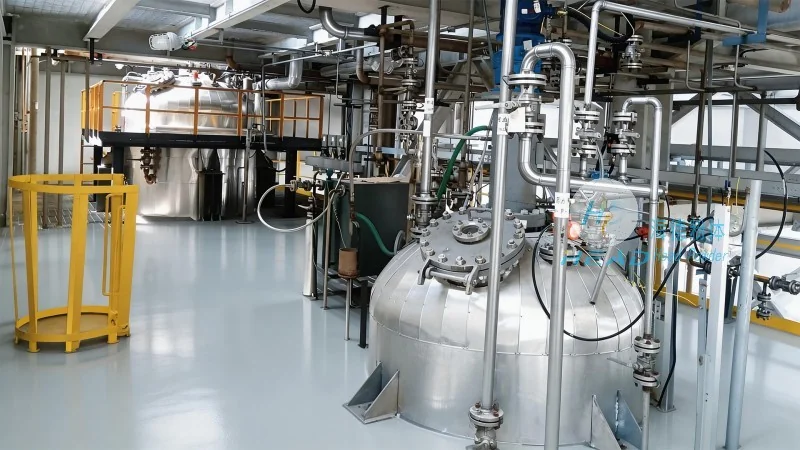
The operation of the tonne bag powder conveying system follows a systematic process. Initially, the tonne bag is placed in the discharger. The system then uses mechanical or pneumatic forces to open the bag and release the powder. The powder falls into the conveyor, which then transports it to the desired destination. The control panel manages the speed and direction of the conveyor, ensuring that the material is transferred at the optimal rate. The dust collection system continuously operates to capture any particles that may be released during the process, preventing contamination and maintaining air quality. This integrated approach ensures that the entire process is efficient, safe, and consistent.
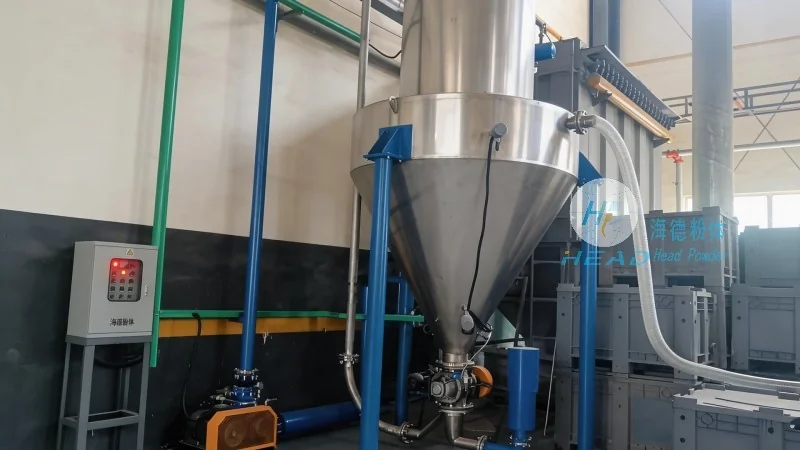
The tonne bag powder conveying system offers several advantages that make it a preferred choice for industries dealing with bulk powders. Its automated operation reduces labor costs and minimizes human error, leading to higher productivity. The system's design allows for easy maintenance and cleaning, which is crucial for industries with strict hygiene standards. Additionally, the dust collection feature enhances safety by preventing dust accumulation and potential health hazards. The system is highly adaptable and can be customized to meet the specific requirements of different applications, making it suitable for a wide range of industries including food, chemicals, and pharmaceuticals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top