HeadPowder, a leading manufacturer in the field of pneumatic conveying systems, specializes in providing efficient and reliable solutions for transporting cement fly ash and mineral powders. This article introduces the key equipment and structural principles of our pneumatic conveying systems, highlighting their design, functionality, and practical applications.
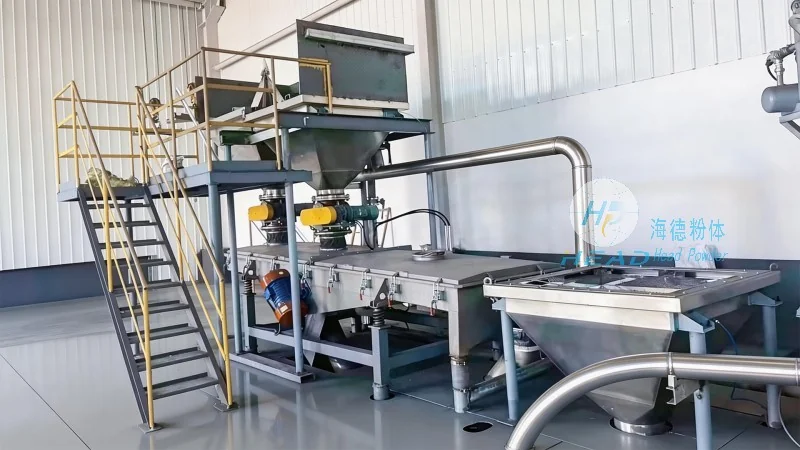
Our pneumatic conveying systems are engineered to handle the transportation of fine powders such as cement fly ash and various mineral powders with precision and efficiency. The core equipment includes a series of components designed to ensure smooth material flow from the source to the destination, minimizing downtime and operational costs. These systems are widely used in industrial settings where the reliable transfer of bulk powders is critical.
The structural design of our pneumatic conveying systems is based on proven engineering principles that optimize performance and durability. The main components typically include a hopper for material storage, a feeder to control the flow rate, a conveying line (often equipped with airlocks or rotary valves), and a receiver for the discharged material. The system operates by creating a pressure differential using compressed air, which propels the powder through the pipeline. This method eliminates the need for mechanical components like belts or screws, reducing maintenance requirements and enhancing safety.
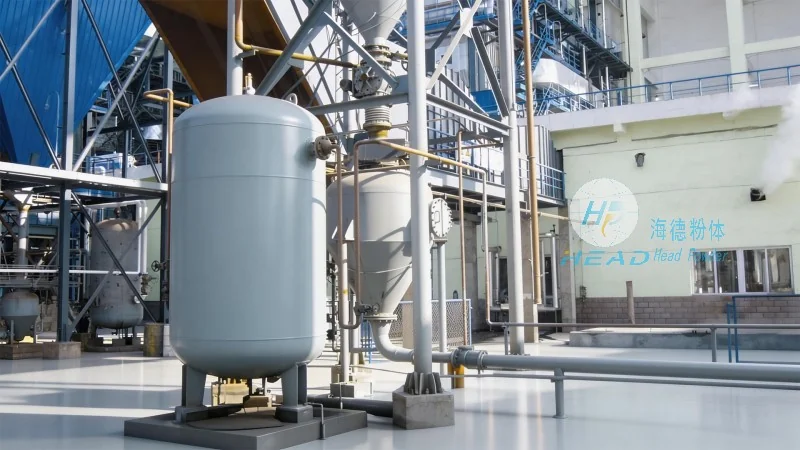
Implementing a pneumatic conveying system for cement fly ash and mineral powders offers several advantages. Firstly, it provides a dust-free and hygienic transfer process, which is essential in environments where contamination control is paramount. Secondly, the system's ability to handle fine powders without clogging or degradation ensures consistent product quality. Additionally, the compact design of our equipment allows for easy integration into existing industrial setups, making it a cost-effective solution for both new and retrofit applications.
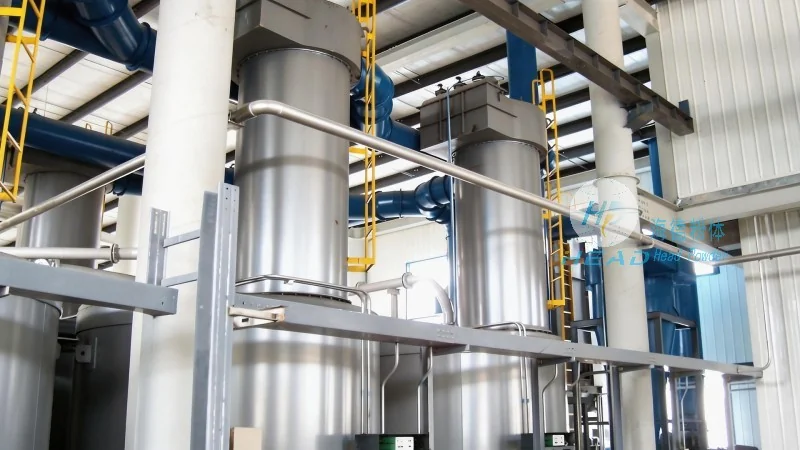
Our pneumatic conveying systems are versatile and can be tailored to meet the specific needs of different industries. Common applications include the transport of cement fly ash from storage silos to mixing plants, the delivery of mineral powders to processing facilities, and the transfer of bulk materials in construction and mining sectors. We offer customization options such as variable speed feeders, adjustable pressure controls, and different pipeline configurations to accommodate varying material characteristics and operational requirements.
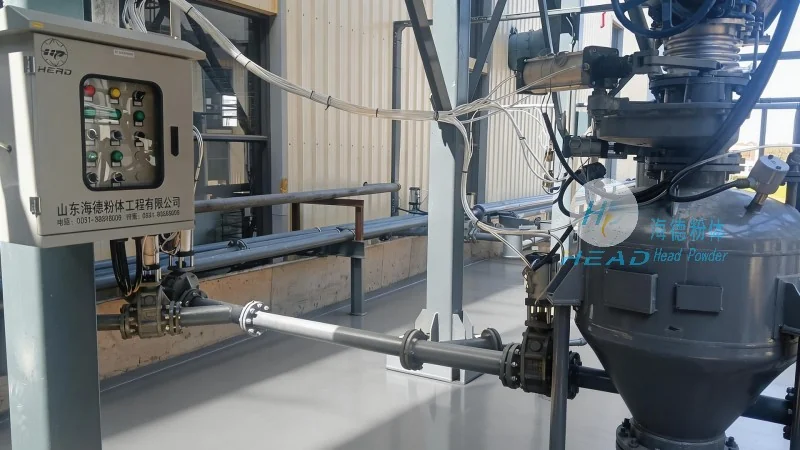
Efficiency is a key focus in the design of our pneumatic conveying systems. By using compressed air as the primary driving force, the systems achieve high transfer rates while maintaining low energy consumption. Regular maintenance, including checks on air pressure, filter systems, and component wear, is essential to ensure long-term reliability. Our equipment is built with high-quality materials and robust construction to withstand the demands of continuous operation, reducing the need for frequent repairs and extending the system's lifespan.
HeadPowder's pneumatic conveying systems represent a sophisticated solution for the efficient and safe transportation of cement fly ash and mineral powders. With a focus on structural integrity, operational efficiency, and customization, our equipment is designed to meet the diverse needs of industrial applications. By leveraging proven engineering principles and advanced manufacturing techniques, we provide reliable systems that enhance productivity and reduce operational costs for our clients. Based in Shandong, China, HeadPowder continues to innovate and deliver high-quality solutions to the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top