Calcined ash, a byproduct from industrial processes like cement production and metallurgy, requires efficient handling to ensure safe and effective material transport. The calcined ash pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd. (commonly known as HeadPowder), addresses these needs through advanced engineering and robust design. This system is engineered to handle the unique characteristics of calcined ash, including fine particle size, density, and dust generation, while maintaining high operational efficiency and minimal maintenance. HeadPowder, a leading manufacturer in material handling equipment, has integrated cutting-edge technology and industry best practices into this system, ensuring it meets the specific requirements of calcined ash handling.
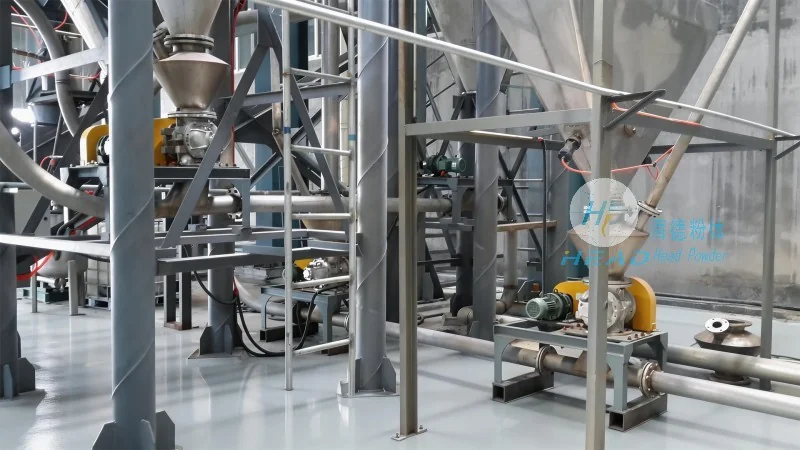
The calcined ash pneumatic conveying system is a comprehensive solution designed to transport calcined ash from its source to the desired destination, such as storage silos or processing units. HeadPowder has integrated cutting-edge technology and industry best practices into this system, tailored to meet the specific requirements of calcined ash, which often involves high volumes and the need for dust control. The system's modular design allows for easy integration into existing industrial facilities, reducing installation time and costs. By leveraging pneumatic transport technology, the system provides a reliable and efficient method for handling calcined ash, minimizing the risks associated with traditional handling methods like bucket elevators or belt conveyors.
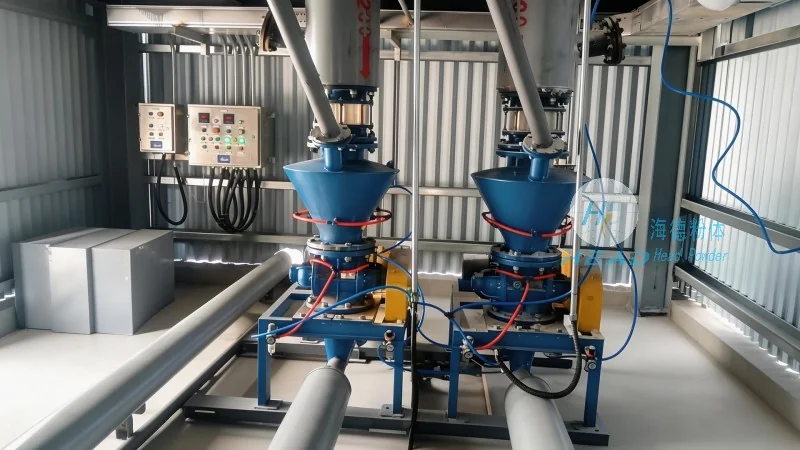
The calcined ash pneumatic conveying system consists of several critical components, each playing a vital role in the overall operation. The primary components include the material feed hopper, the air supply system (typically a blower or compressor), the conveying pipeline, and the discharge unit. The feed hopper is designed to accommodate the calcined ash feed, ensuring a consistent flow into the system. The air supply system generates the necessary pressure and airflow to move the material through the pipeline. The conveying pipeline, often made of durable materials like stainless steel or special coatings, is designed to withstand the abrasive nature of calcined ash particles and prevent blockages. The discharge unit controls the release of the material at the destination, ensuring precise and controlled delivery. The structural design emphasizes durability and efficiency, with each component optimized for the specific demands of calcined ash transport.
The calcined ash pneumatic conveying system operates on the principle of pneumatic transport, where material is suspended in a stream of air and transported through the pipeline. The process begins with the material being fed into the hopper, where it is then drawn into the air stream by the blower. The air and material mixture travels through the pipeline at high velocity, maintaining the material in a suspended state. As the mixture reaches the discharge point, the air is separated from the material, and the ash is deposited into the receiving container. The system's design ensures that the air flow is optimized to prevent material settling or blockages, while maintaining energy efficiency. The use of positive pressure in the system helps to minimize dust emissions and improve safety in the handling process. This principle of operation allows for continuous and unobstructed material transport, making it suitable for high-volume applications.
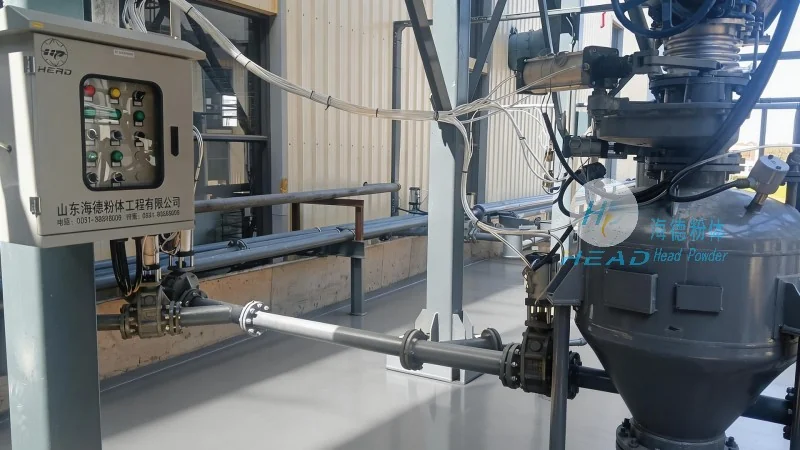
HeadPowder's calcined ash pneumatic conveying system offers several advantages over traditional handling methods, such as bucket elevators or belt conveyors. The system provides a dust-free environment, reducing health hazards and improving workplace safety. It also offers high capacity and continuous operation, making it suitable for large-scale industrial applications. The system's flexibility allows for horizontal, vertical, or combined conveying paths, adapting to the layout of the industrial facility. Applications of this system include transporting calcined ash from kilns to storage silos, feeding material to processing equipment, and handling ash from waste incineration plants. The system's reliability and low maintenance requirements make it a cost-effective solution for long-term material handling needs. Additionally, the system's design minimizes downtime and maintenance costs, contributing to overall operational efficiency and reduced environmental impact.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top