HeadPowder, a leading enterprise in the field of pneumatic conveying technology, specializes in the design, manufacturing, and integration of intelligent pneumatic conveying systems. Based in Shandong, China, the company has established itself as a trusted provider of advanced solutions for material handling and transportation. This article provides an overview of the equipment used in intelligent pneumatic conveying systems, detailing their structural components and operational principles.
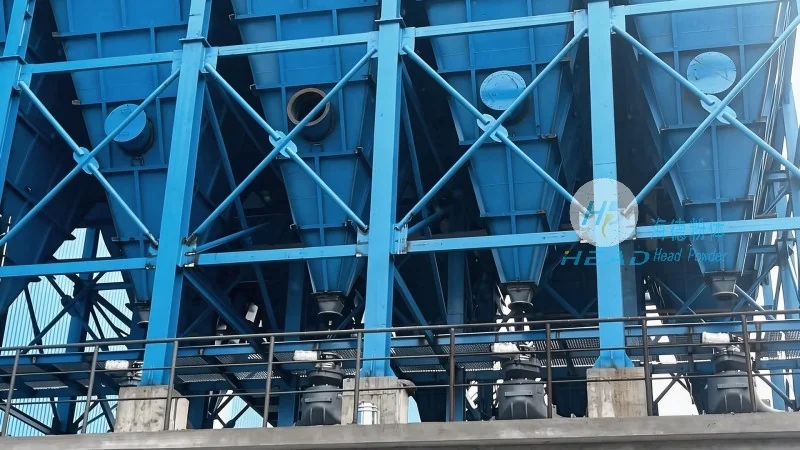
The core of an intelligent pneumatic conveying system lies in its integrated components, each designed to optimize material flow, control, and efficiency. The primary elements include the material feed hopper, which serves as the initial point for loading bulk materials. This component is equipped with a feeding mechanism, such as a rotary valve or a screw feeder, to ensure consistent and controlled material input. The feed hopper is typically constructed from durable materials like stainless steel or high-grade plastic, providing resistance to corrosion and wear from abrasive materials.
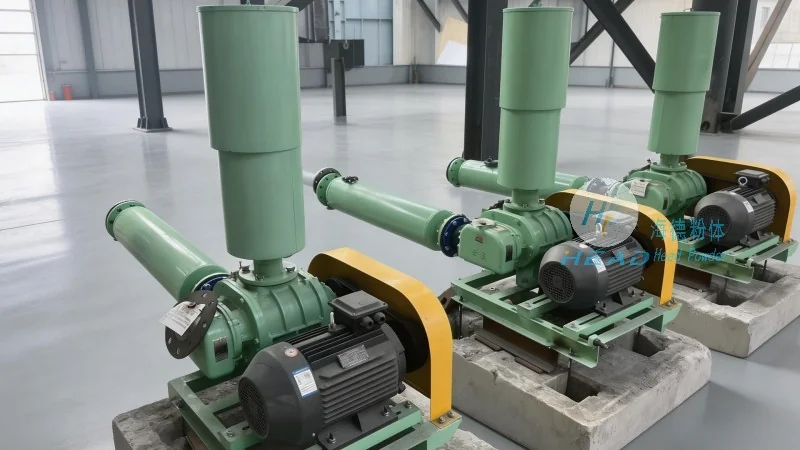
Following the feed hopper is the air supply system, which generates the necessary airflow to transport materials. This system comprises a blower or a vacuum pump, along with a filter and a moisture separator. The blower is responsible for creating the pressure or suction required to move the material particles through the pipeline. The filter and moisture separator are critical for maintaining air quality, preventing contamination of the conveyed material and protecting the system components from damage.
The conveying pipeline is another essential component, made from materials like PVC, stainless steel, or aluminum, depending on the application and material characteristics. The pipeline design includes bends, elbows, and straight sections, all engineered to minimize pressure loss and ensure smooth material flow. For systems requiring long-distance or complex routing, additional components like expansion joints and supports are incorporated to accommodate thermal expansion and structural stability.
The material separation and collection system completes the process. This includes a receiver or a dust collector, which captures the conveyed material at the end of the pipeline. The receiver is often equipped with a discharge valve or a rotary valve to control the release of material into storage containers or processing equipment. In some applications, a cyclone separator or a bag filter may be used to enhance the separation efficiency, ensuring that fine particles are effectively captured and the air is cleaned before release.
The operational principle of an intelligent pneumatic conveying system is based on the movement of material particles within a pressurized or suctioned air stream. The system can operate in either pressure or vacuum mode, depending on the specific requirements of the application. In pressure systems, a blower supplies compressed air to push the material through the pipeline, while in vacuum systems, a vacuum pump creates a negative pressure to draw the material.
The feeding process begins when material is introduced into the feed hopper. The feeding mechanism then releases the material into the air stream, where it is carried along by the airflow. As the material travels through the pipeline, it encounters various components that help maintain its flow and prevent blockages. For example, in-line mixers or agitators may be used to ensure uniform material distribution, especially when handling materials with varying particle sizes or densities.
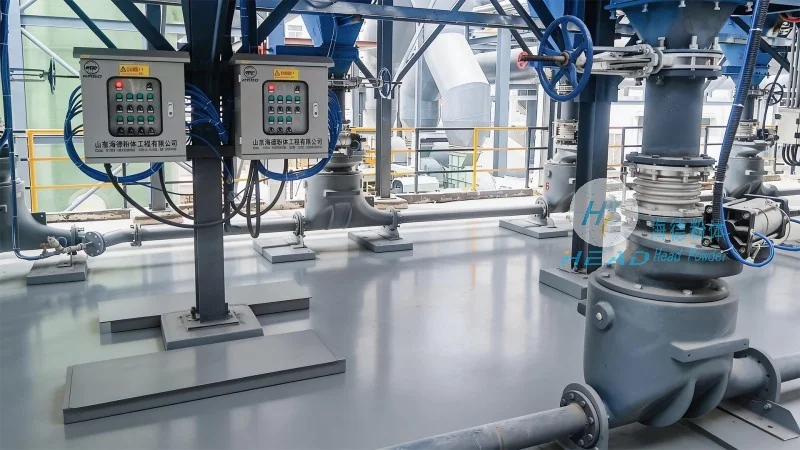
Control systems play a vital role in the intelligent operation of these systems. Modern pneumatic conveying systems are equipped with advanced sensors and controllers that monitor parameters such as pressure, flow rate, and material level. These sensors provide real-time data, allowing the system to adjust its operation dynamically. For instance, if the pressure drops, the system can automatically increase the airflow or adjust the feeding rate to maintain optimal performance. This intelligent control enhances efficiency, reduces energy consumption, and minimizes downtime.
The separation process occurs at the end of the pipeline, where the material is collected in the receiver. The air, now free of material particles, is typically filtered and released back into the environment or recirculated if necessary. The collected material is then discharged from the receiver into storage or processing equipment. The entire process is designed to be continuous and automated, minimizing the need for manual intervention and ensuring consistent performance.
Intelligent pneumatic conveying systems are widely used in various industries, including food processing, pharmaceuticals, chemicals, and minerals. Their versatility makes them suitable for handling a broad range of materials, from fine powders to bulk solids. The systems are particularly advantageous in applications where traditional methods like belt conveyors or bucket elevators are impractical due to material characteristics or space constraints.
One of the key advantages of these systems is their ability to handle abrasive or corrosive materials without significant wear or damage to the equipment. The use of durable materials for the pipeline and components ensures long-term reliability. Additionally, the enclosed design of the system prevents dust emissions, making it environmentally friendly and compliant with regulatory standards.
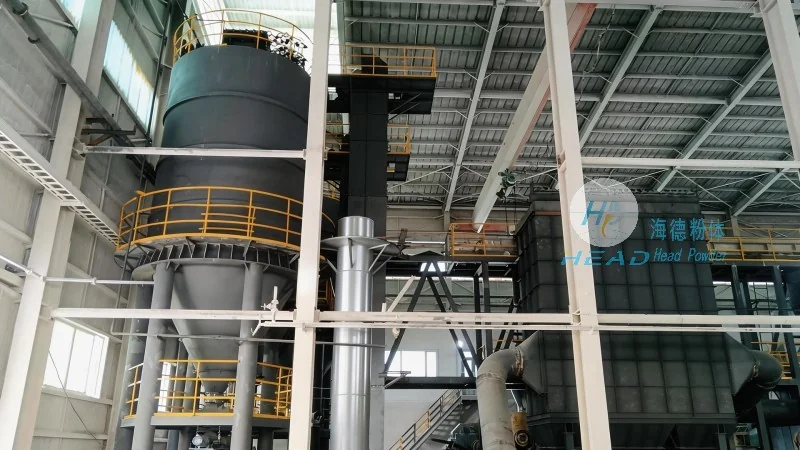
The intelligent control features of modern systems contribute to improved operational efficiency. By monitoring and adjusting parameters in real time, the systems can optimize energy consumption and reduce operational costs. The automation of the process also enhances safety, as it minimizes human exposure to hazardous materials and reduces the risk of accidents.
HeadPowder's commitment to innovation and quality has positioned it as a leading provider of intelligent pneumatic conveying solutions. The company's products are designed to meet the specific needs of clients, offering customized solutions that enhance productivity and efficiency. With a focus on durability, reliability, and intelligent control, HeadPowder's systems provide a cost-effective and sustainable approach to material handling and transportation.
In summary, intelligent pneumatic conveying systems represent a sophisticated and efficient solution for material handling and transportation. The combination of advanced components, intelligent control systems, and robust design makes these systems ideal for a wide range of industrial applications. HeadPowder, with its expertise and commitment to quality, continues to lead the way in providing reliable and innovative pneumatic conveying solutions. As industries evolve and demand more efficient material handling methods, the role of intelligent pneumatic conveying systems will only grow, making them an essential part of modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top