The cocoa pneumatic conveying system is a specialized piece of equipment engineered for the efficient handling and transportation of cocoa powder within food processing facilities. As a key component in cocoa processing lines, this system ensures that cocoa powder is moved from storage silos or bulk containers to processing units, packaging lines, or other areas of the production facility with minimal manual intervention. The primary goal of such equipment is to maintain product integrity, hygiene standards, and operational efficiency, making it an indispensable tool for modern cocoa processing operations.
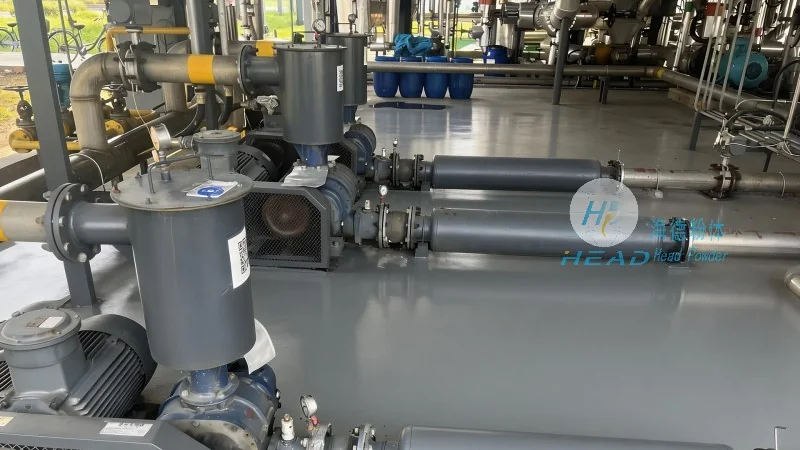
The cocoa pneumatic conveying system comprises several critical components, each designed to perform a specific function in the overall operation. The main structural elements include the hopper, rotary airlock valve, air compressor, conveying pipeline, and dust collection or separation unit. The hopper serves as the storage vessel for cocoa powder, typically constructed from stainless steel or other food-grade materials to prevent contamination and ensure easy cleaning. It features a sloped interior to facilitate the flow of powder and may include a level indicator to monitor the material volume. The rotary airlock valve, positioned at the bottom of the hopper, acts as a controlled discharge mechanism. This component uses rotating blades to allow a controlled amount of cocoa powder to enter the pipeline while preventing backflow of air, thereby maintaining system pressure and preventing material spillage. The air compressor is the power source of the system, generating the necessary air pressure to create a flow of air-powder mixture through the pipeline. It is usually equipped with a filter to remove moisture and particulates from the air, ensuring clean air for conveying. The conveying pipeline is made of durable materials like stainless steel or food-grade plastic, with smooth inner surfaces to minimize friction and material wear. The pipeline is designed to handle the abrasive nature of cocoa powder and is often equipped with bends and elbows that are carefully engineered to maintain consistent air velocity and prevent powder settling. At the receiving end, a separator or cyclone is used to separate the cocoa powder from the air stream. This unit typically consists of a cylindrical chamber with a conical bottom, where the air-powder mixture enters and the centrifugal force causes the heavier cocoa powder to be deposited into a collection container, while the air is discharged back into the system or released to the environment.
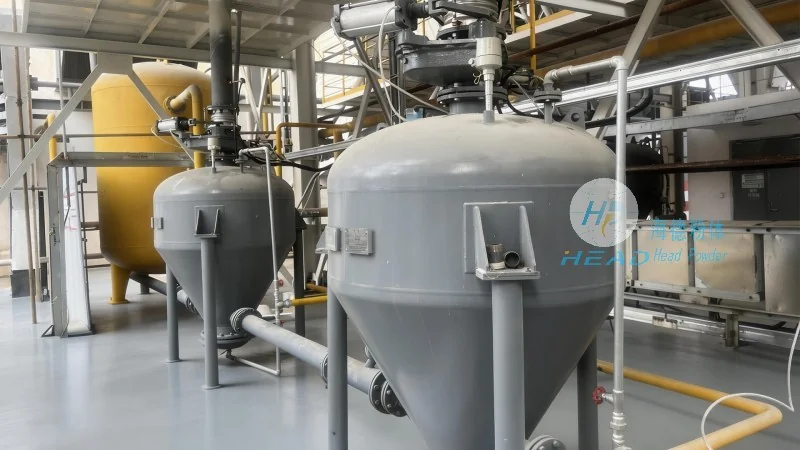
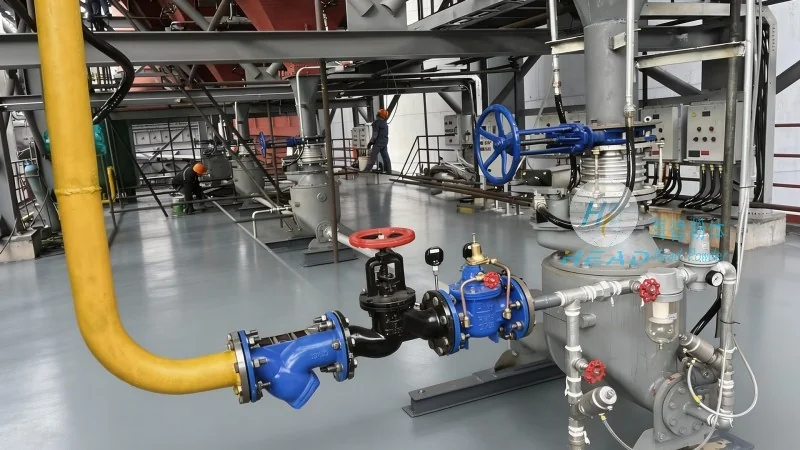
The operation of the cocoa pneumatic conveying system is based on the principle of creating a pressure differential between the hopper and the receiving end. The air compressor supplies compressed air to the pipeline, which is then introduced into the hopper through a venturi or a direct connection. As the air flows into the hopper, it mixes with the cocoa powder, forming an air-powder mixture. This mixture is then drawn through the pipeline by the pressure difference, moving towards the receiving end. The air velocity in the pipeline is maintained at a level sufficient to keep the cocoa powder suspended and prevent it from settling. The separator at the receiving end uses centrifugal force to separate the powder from the air. The separated cocoa powder is collected in a container, while the air is either recirculated back into the system or vented out. The entire process is continuous and can be controlled automatically, allowing for precise control of the conveying rate and ensuring consistent product flow. The system operates in a closed loop, minimizing dust emissions and maintaining a clean working environment, which is essential for food processing applications.
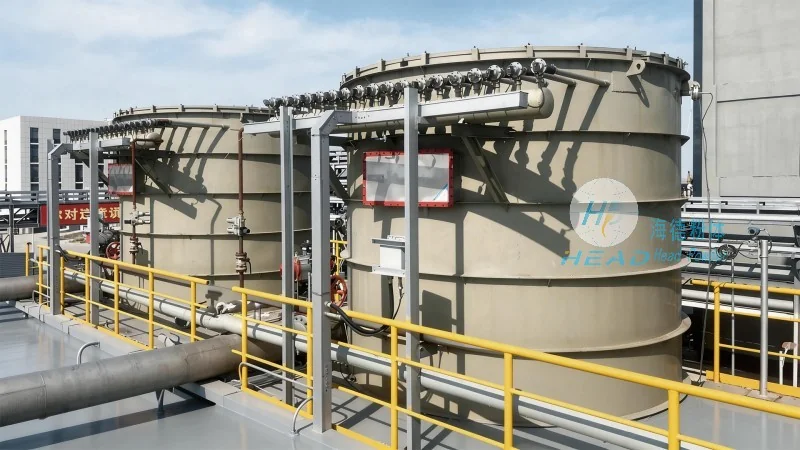
Compared to traditional material handling methods such as belt conveyors, bucket elevators, or manual handling, the cocoa pneumatic conveying system offers several distinct advantages. One of the most significant benefits is the hygienic and dust-free operation. The enclosed system prevents cocoa powder from coming into contact with the external environment, reducing the risk of contamination from dust, moisture, or other particles. This is particularly important in food processing, where product purity and safety are paramount. The system also provides a more efficient and flexible material transport solution. It can handle large volumes of cocoa powder over long distances with minimal space requirements, and the flexible pipeline design allows for easy integration with existing processing lines or reconfiguration as production needs change. Additionally, the pneumatic conveying system reduces labor costs and material handling time, as it automates the process of moving cocoa powder from storage to processing units. The system is also relatively low maintenance, with fewer moving parts compared to mechanical conveyors, and the components are designed for durability and long service life. Furthermore, the system can be equipped with sensors and control systems to monitor and adjust the conveying parameters in real-time, ensuring optimal performance and product quality.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of pneumatic conveying equipment in China. The company specializes in designing, manufacturing, and providing customized solutions for various material handling applications, with a particular focus on the food industry. HeadPowder's products are engineered to meet the highest standards of hygiene, safety, and performance, ensuring compliance with international food processing regulations. The company's headquarters is located in Shandong, China, where it has established a state-of-the-art manufacturing facility equipped with advanced production equipment and a dedicated research and development team. The R&D team continuously works on improving the design and functionality of the conveying systems, incorporating the latest technologies to enhance efficiency and reliability. HeadPowder's commitment to quality and customer satisfaction has made it a trusted partner for many food processing companies worldwide, providing them with reliable and efficient solutions for their material handling needs. The company's products are known for their durability, ease of maintenance, and ability to deliver consistent performance in demanding industrial environments.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top